



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
waste water treatment system supplier
High-Efficiency Waste Water Treatment System for Global Use
If you're a procurement manager or lead engineer in South America, Southeast Asia, Europe, the Middle East, or Africa and you're upgrading infrastructure, picking a reliable waste water treatment system from a waste water treatment system supplier is a key decision for long-term operational stability. A waste water treatment system is the technical framework that removes physical, chemical, and biological contaminants from effluent. It ensures discharged water meets environmental rules or can be reclaimed for industrial reuse. In water treatment today, these systems need to balance high-performance filtration with energy efficiency to stay sustainable over a multi-decade lifecycle.
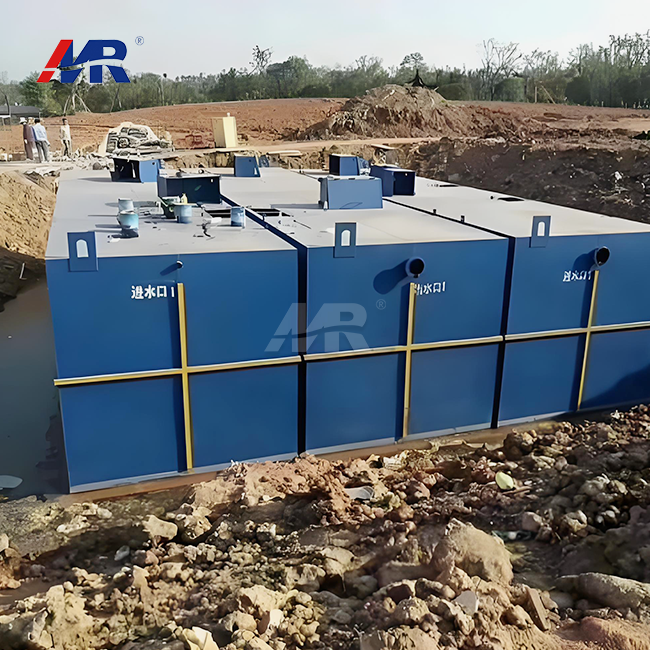
In these regions, operators constantly deal with serious headaches, whether it's tighter local rules or the steep running costs of traditional treatment methods. Across Southeast Asia and South America, high humidity and shifting influent loads tend to weaken biological stability, which makes effluent quality fluctuate. On top of that, many facilities wrestle with the large footprint of conventional clarifiers and the difficulty of finding certified parts that meet international safety standards. And when fast technical support isn't available from a waste water treatment system supplier, or when sophisticated membrane components are tough to maintain, downtime climbs and maintenance costs can blindside operators.
Guangdong Morui Environmental Technology Co., Ltd. was founded in 2005 and supplies specialized waste water treatment system solutions built to solve these regional pain points. Our approach focuses on modularity and resilience under high loads, especially through the MR-MBR-5TH model. Designed for domestic wastewater treatment, this system uses an AAO+MBR flow process: Anaerobic-Anoxic-Oxic plus Membrane Bioreactor. That setup delivers strong nutrient removal and clear effluent while keeping a compact footprint. The equipment is certified to ISO, CE, and ROHS, so it meets the strict quality control requirements of European and Middle Eastern markets and can fit into existing municipal or industrial grids.
- Advanced AAO+MBR Process Integration: Pairing biological nutrient removal with ultrafiltration membranes removes the need for secondary clarifiers. This cuts the system footprint by a lot and still delivers Class A effluent quality.
- International Standard Compliance: The hardware and electrical components hold ISO, CE, and ROHS certifications. The wastewater treatment system meets global safety and environmental rules, so it can be deployed right away.
- Optimized Physical Dimensions: With a footprint of 9x2x2.4 meters, the MR-MBR-5TH model is engineered for rapid site installation and ease of transport to remote locations in Africa and South America.
- Consistent Throughput Performance: The system provides a stable capacity of 100m³/day, featuring automated toxicity monitoring to protect the biological reactor from sudden influent shocks.
Technical specifications, including respirometry test results and membrane integrity data, can be provided to assist in the validation of system performance against specific project requirements. Engaging with our technical team allows for the customization of the AAO process parameters to better suit local ambient temperatures and pollution loads.
The modular design of the MBR unit allows for scalable capacity upgrades to meet the growing demands of urban and industrial water treatment facilities.
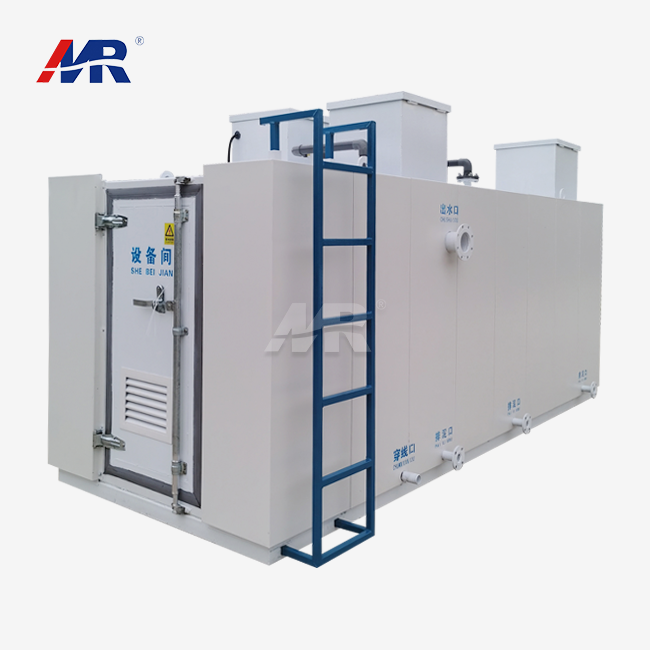




Guangdong Morui Environmental Technology: Proven Expertise in Waste Water Treatment
Established in 2005, Guangdong Morui Environmental Technology Co., Ltd. is a specializing in high-performance waste water treatment system supplier. We have been in this business for almost twenty years and have a strong foothold in South America, Southeast Asia, Europe, the Middle East, and Africa. We build stable infrastructure that meets strict environmental standards.
We are very good at providing complete water treatment solutions, like our MR-MBR-5TH series for treating wastewater from homes. Our systems get Class A wastewater quality by using a sophisticated AAO+MBR flow method in a small 9x2x2.4-meter space. Our engineering team specializes in high-dimensional designs that keep biomass from being shocked and keep its performance stable even when the input conditions change for both home and business use.
ISO, CE, and ROHS certificates show that we are dedicated to quality. We put mechanical reliability first by using AISI 316L stainless steel parts that don't rust and IP65-rated control panels. Every wastewater treatment system goes through strict tests to make sure the membranes are intact and the pumps are working properly. This makes sure that the system always delivers clean water and lasts a long time.
Morui has a wide range of services available to help our customers all over the world. These include online fixing, on-site technology training, and expert advice on how to do routine maintenance. We offer the technical know-how needed for long-term water management, whether it's getting chemicals back into the water or making sure that rules are followed. Work with Guangdong Morui to get answers that can be scaled up to protect people's health and water environments around the world.

Integrated MBR Technology for Sustainable Global Water Resilience
Where These Systems Fit in Modern Infrastructure
Pressure to meet environmental standards keeps building, and it isn't going away. A wastewater treatment system you can depend on is a must, and picking the right waste water treatment system supplier can make all the difference. It protects the ecological balance and keeps operations running. One common use is decentralized domestic sewage treatment for apartment complexes and hotels. Process water treatment in industrial parks is another, along with high-grade water reuse for commercial farm irrigation. These systems have to handle organic loads that shift over time. They also need to meet discharge permits in very different climates, from the humid tropics of Southeast Asia to the dry Middle East.
Compliance and Operating Challenges
Clients in South America, Europe, and Africa are now dealing with tighter environmental rules. Meeting Class A effluent quality is one example. The hard part is balancing high energy costs against the push for automated, low-maintenance operation. Traditional systems often fall short. They take up too much space, respond poorly to toxic influent, and produce too much sludge. In remote areas, there's no on-site technical expertise to rely on right away. That's why reliability and remote monitoring from a waste water treatment system supplier matter so much. They help companies avoid costly downtime and environmental penalties.
Morui's Integrated Wastewater Treatment Solution
Guangdong Morui Environmental Technology Co.,Ltd started operations in 2005. Its advanced modular system is built around the MR-MBR-5TH model. It combines biological treatment with physical membrane separation. Customers receive a complete engineering package that meets ISO, CE, and ROHS standards. Rather than piecing together separate pieces of equipment, they get one factory-tested unit. Startup is fast, and the unit performs reliably in demanding overseas markets.
System Architecture and Technical Configuration
The system runs through several stages. This design aims to remove the most contaminants possible and keep the process stable:
- Biological Unit (AAO Process): The Anaerobic-Anoxic-Oxic flow process delivers deep nitrogen and phosphorus removal. It also stabilizes the biomass before filtration.
- MBR Ultrafiltration Module: This unit is the core of the system. It relies on high-performance membranes rather than traditional secondary clarifiers. Effluent turbidity stays well below regulatory limits, even at 100m3/day.
- Automated Control System: A single integrated PLC interface runs the entire flow. It guards against biomass shock and lowers energy use by matching demand in real time.
- Compact Structural Design: The full system sits in a corrosion-resistant frame that measures 9X2X2.4 meters. That build holds up to harsh outdoor conditions.
Measurable Benefits and Strategic Gains
- Footprint Efficiency: The modular layout cuts land needs by 40–60% against conventional activated sludge plants.
- High-Quality Effluent: Every run meets Class A standards. That makes the treated water fit for non-potable reuse and resource recovery.
- Certified Reliability: The equipment is CE and ISO compliant. It holds up mechanically and stays electrically safe, even when industrial loads are heavy.
- Operational savings: Automated chemical dosing and clean-in-place (CIP) modules can lower manual labor needs by as much as 70%.
Global Deployment and Service Excellence
Guangdong Morui Environmental Technology Co.,Ltd guides its customers worldwide through a structured project lifecycle. It starts with influent analysis and runs through to remote diagnostic support. For projects in Southeast Asia and the Middle East, the company supplies full technical documentation along with modular spare parts kits, which keeps maintenance local. This approach cuts the risks that come with international logistics and protects system integrity over the long term.
Typical Application Case: MR-MBR-5TH
A domestic wastewater project proves what an AAO+MBR system can do. The site had little space and strict discharge rules, so the client brought in the MR-MBR-5TH system to treat 100m3/day of sewage. The compact 9-meter unit took over from a traditional plant that had stopped performing. Energy use fell 30% in the first month. The plant stayed within local nutrient concentration limits 100% of the time.
Advanced membrane bioreactor technology lets you reclaim water to high standards. It works at any scale and anywhere you are.
FAQs
1. How do I choose the most reliable waste water treatment system for my facility's specific needs?
Selecting the right waste water treatment system requires a balance between effluent quality, footprint, and operational stability. For domestic or industrial applications, you should first evaluate your daily capacity requirements and the target discharge standards. A system like the MR-MBR-5TH, which utilizes the AAO+MBR (Anaerobic-Anoxic-Oxic + Membrane Bioreactor) process, is often preferred for its ability to produce high-quality effluent in a compact 9x2x2.4 meter footprint. Guangdong Morui Environmental Technology Co.,Ltd recommends checking if the equipment holds certifications like ISO or CE, which verify manufacturing quality. We suggest providing your raw water parameters and site dimensions so our engineers can customize a solution that ensures long-term compliance and minimizes energy consumption.2. What are the primary performance advantages of an integrated MBR waste water treatment system?
An integrated MBR (Membrane Bioreactor) waste water treatment system offers significant benefits over traditional sedimentation-based systems. By replacing the secondary clarifier with ultrafiltration membranes, systems like the MR-MBR-5TH achieve superior solids-liquid separation, resulting in Class A water quality suitable for reuse. This specific model handles a capacity of 100m³/day, making it ideal for localized domestic wastewater treatment. Key advantages include a significantly smaller physical footprint, reduced sludge production, and the ability to maintain a higher biomass concentration, which improves the removal efficiency of organic pollutants. For projects in South America or Southeast Asia where land costs or space constraints are high, this high-efficiency design provides a cost-effective and space-saving solution.3. Does a waste water treatment system from Morui comply with local environmental regulations in Southeast Asia, the Middle East, or Africa?
Compliance is a critical factor for international projects. A waste water treatment system manufactured by Guangdong Morui Environmental Technology Co.,Ltd is designed to meet international standards, supported by ISO, CE, and ROHS certifications. Generally, these systems are engineered to meet common discharge limits for BOD, COD, and Nitrogen; however, specific discharge requirements often vary by country and local municipality. For instance, projects in the Middle East may have stricter water reuse standards compared to industrial discharge limits in parts of Africa. We advise clients to provide their local regulatory "Table of Standards" so we can calibrate the AAO+MBR process to ensure the treated water consistently meets or exceeds local environmental mandates.4. How does the waste water treatment system maintain stability under varying influent conditions in tropical or arid climates?
Operating a waste water treatment system in diverse climates like the humid regions of Southeast Asia or the arid environments of the Middle East requires robust biological control. Our systems utilize an advanced AAO (Anaerobic-Anoxic-Oxic) process, which provides multiple stages of treatment to handle fluctuations in organic loading and toxicity. To ensure stability, we recommend three key steps: implementing an equalization tank to buffer influent flow, conducting regular membrane integrity tests, and monitoring dissolved oxygen levels within the biological reactors. The MR-MBR-5TH is built with high-quality components designed to withstand harsh environments, and Guangdong Morui Environmental Technology Co.,Ltd provides technical guidance to help local operators adjust aeration and sludge return rates based on seasonal temperature changes.5. How can international buyers verify the authenticity and technical strength of Guangdong Morui Environmental Technology Co.,Ltd?
Verifying a supplier’s credibility is essential for successful international procurement. Guangdong Morui Environmental Technology Co.,Ltd has been a professional manufacturer in the water treatment industry since 2005, giving us nearly two decades of expertise in engineering complex waste water treatment system solutions. Prospective clients can verify our strength through our ISO, CE, and ROHS certifications and by reviewing our project portfolio across South America, Europe, and Asia. We encourage buyers to request detailed technical drawings of the MR-MBR-5TH and documentation of our AAO+MBR process performance. For large-scale projects, we offer comprehensive technical support, including remote installation guidance or on-site commissioning, to ensure the system is integrated seamlessly into your local infrastructure.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.