



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
1T/H EDI system supplier
High-Performance 1T/H EDI Systems for Industrial Ultrapure Water
Procurement managers in South America, Southeast Asia, Europe, the Middle East, and Africa need ultrapure water they can depend on. When they evaluate a 1T/H EDI system from a 1T/H EDI system supplier, long-term efficiency is usually the first thing they consider. Electrodeionization (EDI) is an advanced water treatment technology. It combines electricity, ion-exchange membranes, and resin to continuously deionize water, with no hazardous chemical regeneration. The process plays a key role in modern water treatment. It supplies the steady stream of high-purity water that precision manufacturing and laboratory environments require.
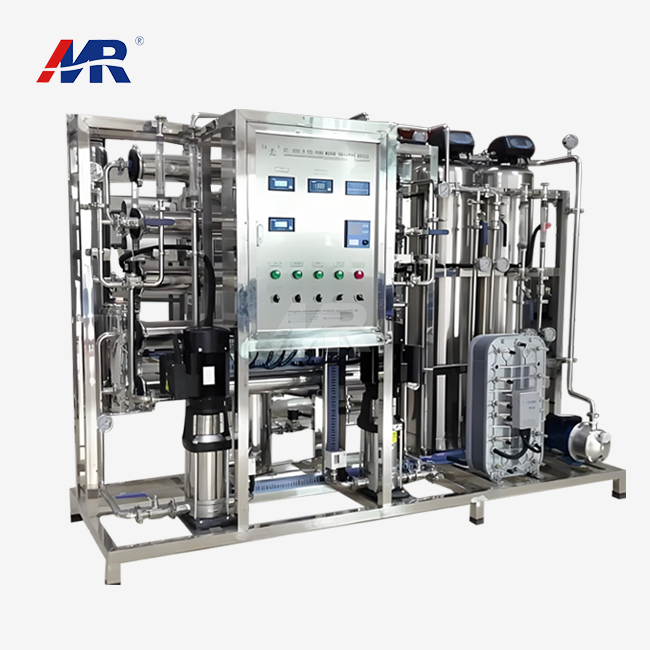
Industrial facilities across Southeast Asia and the Middle East run into real trouble when they try to meet ultra-high purity standards. Local environmental rules for discharging acidic or caustic wastewater from traditional ion exchange systems are strict, and energy costs add up quickly. Many plants also struggle to keep the system stable when feed water conditions shift, which leads to membrane scaling or unplanned downtime. At remote project sites in Africa and South America, just getting regeneration chemicals on site is a logistics problem in itself. Technical support is not close at hand either, so for a plant relying on a 1T/H EDI system supplier, sourcing dependable water treatment solutions becomes that much harder.
Guangdong Morui Environmental Technology Co., Ltd has been in business since 2005. The company provides specialized 1T/H EDI system solutions built to ease these operational constraints around the world. With ISO, CE, and ROHS certifications behind it, this experienced 1T/H EDI system manufacturer focuses on robust, pre-engineered units that make installation and validation simpler for international clients. The Model MR-EDI-1TH is engineered for ultrapure water production, and its advanced stack technology holds results steady across very different climates. Durability and easy integration come first, so procurement managers can sidestep the risk that comes with unverified suppliers and substandard components.
The following technical and service advantages define the Morui 1T/H EDI system approach:
- Chemical-Free Operation: The system regenerates itself continuously through electricity. There are no hazardous chemicals to handle, and the system stays in line with ROHS environmental standards.
- High-Efficiency Rejection: Salt rejection on the MR-EDI-1TH runs at 99.99%. The water it produces has the high resistivity that sensitive industrial applications need.
- Low Energy Draw: The 1T/H EDI system runs on 4 kW/hour. For plants working to lower total cost of ownership and shrink their energy footprint, that power profile keeps operating costs in check.
- Meets Global Rules: Every unit comes out of ISO-certified manufacturing and carries the CE mark. That satisfies the strict safety and quality documentation buyers in Europe and South America ask for.
- Steady Output Numbers: A 55% recovery rate keeps permeate output and concentrate management in balance. Membranes hold up longer this way, even across varied water treatment conditions.
Technical specs, performance data sheets, and custom engineering drawings are ready to support your selection and integration work. Talk to our technical team, and we can line up the system configuration with your actual feed water quality and the conditions at your site. A total cost analysis shows continuous electrodeionization as a sustainable route to high-resistivity water, without the logistical burden of chemical handling.
Related Products




About Guangdong Morui Environmental Technology Co., Ltd.
Founded in 2005, Guangdong Morui Environmental Technology Co., Ltd. is a professional manufacturer focused on advanced water treatment solutions. Nearly two decades of engineering experience have made us a dependable 1T/H EDI system supplier for high-purity water systems. Our industrial customers span South America, Southeast Asia, Europe, the Middle East, and Africa.
We focus mainly on designing and manufacturing the 1T/H EDI system (Model: MR-EDI-1TH). These systems are made for ultrapure water production. They reach a 99.99% salt rejection rate and a 55% recovery rate, and power use stays low at 4kw/hour. As an ISO, CE, and ROHS-certified 1T/H EDI system supplier, we make sure every 1T/H EDI system meets strict quality control standards, including monitoring electrical current stability and pressure drop testing. The result is a chemical-free, continuous deionization process that replaces traditional ion exchange.
To support our international clientele, Morui offers comprehensive technical services ranging from remote debugging and onsite training to long-term maintenance support. We are committed to helping global facilities reduce their total cost of ownership through sustainable water treatment technology. Partner with Morui for stable, high-resistivity water supply and proven project execution excellence.

Sustainable High-Purity Water via Advanced 1T/H EDI Technology
Industrial Water Treatment Use Cases
High-resistivity water is a workhorse in modern industry, keeping product quality steady and helping equipment last longer. The 1T/H EDI (Electrodeionization) system, often sourced from a 1T/H EDI system supplier, covers three main jobs: rinsing wafers in electronics, making injection-grade water for pharmaceuticals, and feeding high-pressure boilers in power plants. In each case, the water has to be nearly free of dissolved ions, silica, and carbon dioxide. That keeps it from disrupting sensitive chemical processes or heat exchange surfaces.
Regional Hurdles and Operating Pain Points
In places like Southeast Asia and the Middle East, operators often have to deal with hard, salty feed water. That can cause scaling in traditional systems fast, which is why a 1T/H EDI system supplier is often the first call. In Europe, strict rules on chemical waste discharge are making traditional ion exchange less and less workable, because it needs acid and caustic regeneration.
Some common challenges come up again and again:
- Regulatory compliance: following CE and ROHS standards for environmental safety and wastewater discharge.
- Operational downtime: Traditional resin beds have to shut down every so often for chemical regeneration. That can create production bottlenecks.
- High energy costs: Where electricity is expensive, inefficient purification systems drive up the total cost of ownership by a lot.
- Maintenance Expertise: Remote parts of Africa and South America rarely have trained technicians on hand. That alone can turn a complex manual system into a real liability.
Guangdong Morui Environmental Technology Co.,Ltd Solution
Leveraging nearly two decades of expertise since 2005, Morui provides a modular 1T/H EDI solution designed to replace hazardous chemical deionization. Our approach integrates the MR-EDI-1TH model into a seamless, automated process that delivers ultra-pure water continuously. By combining membrane filtration with electrochemical regeneration, the solution eliminates the need for chemical storage and neutralization, offering a "green" footprint suitable for global export markets.
System Architecture and Key Components
The system is engineered for stability and high-flux performance, consisting of several critical modules:
- Pre-treatment & RO Module: Removes the bulk of dissolved solids, ensuring the feed water quality meets the EDI stack’s stringent requirements to prevent scaling.
- MR-EDI-1TH Stack: The core unit uses high-grade ion-exchange membranes and resins. It draws just 4kw/hour of power and still rejects 99.99% of salt.
- Intelligent Control System: A PLC interface tracks DC voltage, amperage, and water resistivity in real time. That allows unmanned operation and keeps water quality steady.
- Internal cleaning. A dedicated CIP (Cleaning-In-Place) loop flushes the stack, so microbes and minerals never get a chance to build up. That keeps the components running longer.
Benefits You Can Measure, Plus a Strategic Edge
- Purity that holds up. The system turns away 99.99% of salt, and the water it produces stays consistently above 15-18 MΩ·cm resistivity.
- Efficient with resources. A 55% recovery rate lets the system balance high-purity output against water savings.
- Lower energy use. Drawing just 4kw/hour, the system trims operational energy costs by roughly 20-30% next to older EDI models.
- No Chemicals Needed: There are no regeneration chemicals to buy, handle, or throw away. Those costs are gone.
- Certified Worldwide: Our products meet ISO, CE, and ROHS standards in full. That helps your shipment clear customs without trouble and get approved by local regulators.
Implementation and International Service Capability
Guangdong Morui Environmental Technology Co.,Ltd follows a project through its whole life, starting with water analysis and engineering designed for your site, then moving on to manufacturing and global shipping. International customers get extra support as well. We can run remote diagnostics, and our partners in South America, Southeast Asia, and other regions rely on a spare parts chain that responds fast. We also train local operators, which keeps systems healthy over the long run and downtime to a minimum.
Typical Implementation Case
A semiconductor manufacturer in Southeast Asia needed a steady 1T/H of ultrapure water, but chemical costs were high and the resin kept wearing out. With the MR-EDI-1TH in place, the plant switched to a continuous, automated process. Chemical handling fell by 100%, production uptime improved by 15%, and the water has consistently met international electronics-grade standards.
Technical specs and full performance data are the starting point when you're choosing the most efficient ultrapure water purification architecture.
FAQs
1. What are the primary advantages of implementing a 1T/H EDI system for industrial ultrapure water production?
An Electrodeionization (EDI) system, such as our MR-EDI-1TH model, offers a continuous, chemical-free process to produce high-purity water, eliminating the need for hazardous acid and caustic regeneration required by traditional ion exchange. By integrating a 1T/H EDI system into your workflow, you benefit from a compact footprint and lower operational costs. Our system is engineered for efficiency, featuring a 4kw/hour power consumption and a 99.99% salt rejection rate. This ensures a stable, high-resistivity water supply for demanding applications like electronics or pharmaceuticals. To maximize efficiency, we recommend maintaining a recovery rate of approximately 55%. For a detailed energy-saving analysis for your specific facility, please contact Guangdong Morui Environmental Technology Co.,Ltd.2. How does the MR-EDI-1TH model ensure high salt rejection and long-term performance stability?
The MR-EDI-1TH ensures a 99.99% salt rejection rate by utilizing high-quality ion-exchange membranes and resin that are continuously regenerated by an electric field. To maintain this performance, it is critical to monitor the feed water quality coming from the Reverse Osmosis (RO) stage. We suggest ensuring feed water hardness is less than 1 ppm (as CaCO3) and silica levels are below 0.5 ppm to prevent scaling within the EDI stack. Additionally, consistent monitoring of DC voltage and amperage is vital for efficient ion migration. Established in 2005, Guangdong Morui Environmental Technology Co.,Ltd designs these systems to minimize downtime and bypass the batch regeneration cycles common in older technologies.3. For projects in Europe, Southeast Asia, or the Middle East, what certifications and standards does the 1T/H EDI system meet?
When exporting to diverse markets such as Europe, Southeast Asia, the Middle East, Africa, and South America, compliance with international quality and safety standards is mandatory. Our 1T/H EDI system is manufactured under ISO standards and carries CE and ROHS certifications, ensuring it meets rigorous safety and environmental requirements. These certifications typically cover electrical safety and the restriction of hazardous substances, which are essential for industrial equipment entering the European and Middle Eastern markets. However, specific local import regulations or water discharge standards may vary by country. We recommend sharing your local site requirements with us so Guangdong Morui Environmental Technology Co.,Ltd can ensure full compliance with your regional laws.4. What are the critical feed water requirements to prevent fouling in an EDI water system?
To protect your 1T/H EDI system from premature fouling or mineral scaling, the influent water must be pre-treated, usually via a double-pass RO system. Key parameters to monitor include Total Organic Carbon (TOC), chlorine levels, and water hardness. If the feed water exceeds 1 ppm hardness, calcium and magnesium scales can form on the membrane surface, significantly reducing the 55% recovery rate and increasing power consumption beyond the standard 4kw/hour. We suggest implementing a routine sanitization cycle and using online instrumentation to monitor resistivity in real-time. If you are dealing with challenging source water in regions like Africa or Southeast Asia, contact Guangdong Morui Environmental Technology Co.,Ltd for a customized pre-treatment configuration.5. Does Guangdong Morui Environmental Technology Co.,Ltd provide installation and technical support for international clients?
Yes, Guangdong Morui Environmental Technology Co.,Ltd has been serving the global water treatment industry since 2005, providing comprehensive support for our 1T/H EDI systems across South America, Southeast Asia, Europe, the Middle East, and Africa. We offer detailed technical documentation, remote commissioning guidance, and, depending on the project scale, on-site installation support to ensure your MR-EDI-1TH is integrated correctly. Our team can assist in calibrating online meters and TOC analyzers against international standards to ensure accurate performance data. For companies operating in remote regions, we provide specialized maintenance kits and training to ensure your technical staff can handle routine microbial control and stack inspections effectively.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.