



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
2000LPH EDI system supplier
Engineering a High-Purity 2000LPH EDI System for Industrial Water Treatment
For procurement managers and lead engineers across South America, Southeast Asia, Europe, the Middle East, and Africa, picking a dependable 2000LPH EDI system is a critical step toward securing high-purity water for sensitive industrial processes. EDI, or electrodeionization, uses ion-exchange membranes and an electric current to continuously deionize water, which means it sidesteps hazardous chemical regeneration. This technology, often sourced through a 2000LPH EDI system supplier, is a cornerstone of modern ultrapure water production. It delivers a steady supply of high-resistivity water while significantly reducing a facility's physical footprint and environmental impact.
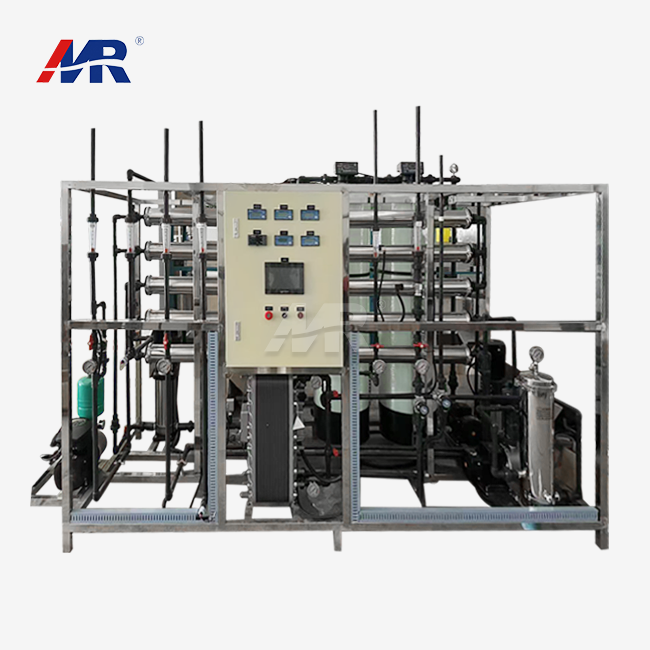
In places with strict environmental rules, like Europe, or where operating costs run high, like Southeast Asia and Africa, industrial plants face real pain points when they choose a 2000LPH EDI system. They must keep up with international safety standards, pay rising energy bills, and, with a dependable 2000LPH EDI system supplier, avoid major downtime caused by an unstable system or a lack of local technical support. Traditional deionization methods also struggle when source water has high salt concentrations. That means frequent maintenance and the logistical burden of handling acidic and caustic chemicals for resin regeneration.
Guangdong Morui Environmental Technology Co.,Ltd was established in 2005. We provide specialized 2000LPH EDI systems designed to meet these industrial challenges worldwide. Our flagship Model MR-EDI-2TH is engineered for high-performance ultrapure water production. It gives facilities a smooth transition from traditional ion exchange beds. We use advanced stack designs that put electrical current stability and membrane integrity first. This makes our systems a reliable alternative to chemical-dependent processes. They are built for the demanding climates and regulatory environments of our target markets in the Middle East and South America.
- Compliance and Quality for International Markets: The system is built with ISO-certified processes and holds CE and ROHS certification. That means it meets the strict safety and quality standards required in Europe and other global markets.
- High-Efficiency Ion Removal: The MR-EDI-2TH is made for critical water treatment work. It reaches a salt rejection rate of 99.99%, so water quality stays consistent even in demanding industrial use.
- Optimized Energy Usage: This 2000LPH EDI system features a power consumption of only 8.5kw/hour, providing a cost-effective solution for regions where energy prices are a primary operational concern.
- Continuous Chemical-Free Operation: With a recovery rate of 55%, the system provides a steady flow of ultrapure water while eliminating the downtime and hazardous waste disposal associated with chemical regeneration.
- Verified Manufacturing Expertise: With nearly two decades of experience since 2005, our engineering team provides comprehensive technical documentation and performance data to support procurement verification and site integration.
Selecting an appropriate 2000LPH EDI system requires a thorough evaluation of technical parameters and supplier manufacturing credentials. Technical teams can review detailed specifications and performance benchmarks to ensure the system aligns with local feedwater conditions and resistivity requirements. Engaging with experienced engineering partners allows for the precise calibration of the EDI stacks to balance energy efficiency with the necessary output volumes for long-term production stability.
Continuous electrodeionization keeps a steady supply of high-resistivity water flowing. It also removes the environmental risks that come with traditional chemical regeneration cycles.
Related Products




About Guangdong Morui Environmental Technology Co., Ltd.
Guangdong Morui Environmental Technology Co., Ltd. got its start in 2005, and we're a premier manufacturer in the professional water treatment industry. High-precision purification is what we do best, and with nearly two decades under our belt, we've become a leading 2000LPH EDI system supplier for industrial applications. Our customers come from South America, Southeast Asia, Europe, the Middle East, and Africa.
Our specialized technical team focuses on the MR-EDI-2TH model, a sophisticated 2000LPH EDI system designed for ultrapure water production, and as a trusted 2000LPH EDI system supplier we build it to replace traditional chemical-intensive ion exchange. The system achieves a 99.99% salt rejection rate and a 55% recovery rate, with efficient power consumption of 8.5kw/hour. This chemical-free, continuous process lets international manufacturing plants meet stringent resistivity requirements while significantly reducing their environmental footprint.
Quality comes first in our operations. Morui Environmental is ISO, CE, and ROHS certified. We maintain strict quality control through electrical current stability monitoring and membrane integrity testing. For our global partners, we provide strong technical support that includes remote debugging, on-site training, and routine maintenance packages. This keeps your ultrapure water supply reliable over the long term.
Guangdong Morui is committed to high-performance solutions that help operations run at their best. For your next high-purity water project, we're ready to deliver sustainable value.

Sustainable 2000LPH EDI Solutions for Global Ultrapure Water Production
Overview of Industrial Application Scenarios
In modern industrial processing, the 2000LPH EDI system is a key piece of equipment for facilities that need a constant flow of high-purity water. This technology is mainly used in the pharmaceutical industry for injectable water production and laboratory reagents, where microbial control and ionic purity can't be compromised, so working with a 2000LPH EDI system supplier who knows the ins and outs is a smart move. In electronics and semiconductor manufacturing, the system provides the ultra-low conductivity water needed for wafer cleaning and circuit board production. Power plants also rely on these systems for high-pressure boiler feed water to prevent scale buildup and corrosion in turbine systems.
Addressing Regional Operational Challenges
Operating ultrapure water systems across South America, Southeast Asia, Europe, the Middle East, and Africa throws a lot of different challenges at you. In regions like the Middle East and Africa, feed water tends to be very hard, and for a 2000LPH EDI system supplier, that means membrane scaling happens fast. If it isn't managed, that scaling can shorten the life of the system.
In Europe, tough rules on wastewater discharge make traditional chemical-based deionization (DI) resin regeneration hard and expensive. Hazardous waste disposal fees drive up the cost. At the same time, facilities in Southeast Asia and South America often put energy efficiency and less downtime first. They do this to offset fluctuating local power costs and a limited pool of specialized labor. If these factors aren't addressed, the result is frequent membrane replacements, high chemical handling risks, and inconsistent water resistivity. Any one of these can stop multi-million dollar production lines.
The Guangdong Morui MR-EDI-2TH Solution
Guangdong Morui Environmental Technology Co.,Ltd was founded in 2005. The company offers a modular turnkey solution built around the MR-EDI-2TH model. The system combines advanced Electrodeionization technology with pre-treatment protocols. These protocols are designed to remove the need for hazardous acid and caustic regeneration. It uses a continuous process powered by electricity. That setup delivers steady ultrapure water output and takes up much less space than traditional ion exchange beds.
System Design and Main Components
For reliability, the 2000LPH EDI system is built with high-grade components:
- Pre-treatment and RO Integration: Feed water usually goes through a Double Pass RO first. That brings conductivity down to the levels the system needs and keeps the EDI stack from fouling too early.
- MR-EDI-2TH Main Module: The core stack uses high-performance ion-exchange membranes. It hits a 99.99% salt rejection rate and a 55% recovery rate, which keeps water efficiency as high as possible.
- Advanced Control System: Built-in PLC and HMI panels let you monitor DC voltage, amperage, and water resistivity in real time. That keeps the system running at its optimized 8.5kw/hour power consumption level.
- CIP (Clean-in-Place) Module: A dedicated maintenance unit lets you clean the stack on a regular schedule without taking it apart. It's built to handle high-fouling loads in tropical climates.
Performance Benefits You Can Quantify
- Zero Chemical Hazards: No toxic chemicals to store or handle. The system meets ISO and ROHS safety standards.
- Energy Optimization: The system runs at 8.5kw/h. That cuts energy use by up to 20% compared to older generation EDI stacks.
- Superior Purity: Consistent achievement of 15-18 MΩ·cm resistivity through 99.99% salt rejection.
- Space Efficiency: The modular design reduces the installation area by approximately 40% compared to conventional DI systems.
- Continuous Production: Unlike batch resin systems, this solution provides 24/7 water supply without regeneration downtime.
Implementation and Global Service Capability
Guangdong Morui supports customers worldwide. Each project follows a set implementation process. It starts with raw water analysis and ends with on-site commissioning. For work in South America and the Middle East, the company provides remote diagnostics so teams can troubleshoot performance issues in real time. The systems hold CE and ISO certifications and are built to international standards. A reliable supply chain supports them, ensuring critical spare parts reach Southeast Asian and African markets in shorter lead times.
Typical Case Study: Pharmaceutical-Grade Water
A pharmaceutical manufacturer in Southeast Asia needed a steady supply of ultrapure water at 2m³/h, and it also had to meet strict local rules on chemical discharge. The plant adopted the MR-EDI-2TH solution and replaced its aging ion exchange beds. The project eliminated chemical waste entirely, cut annual utility costs by 15%, and maintained consistent compliance with pharmacopeia water standards.
Technical Consultation and Specification Support
Detailed selection reports and engineering drawings are available for technical teams to evaluate system compatibility with existing infrastructure. Accessing site-specific performance simulations allows for accurate forecasting of long-term operational expenditures and water quality stability. The MR-EDI-2TH platform ensures stable high-resistivity water production for demanding industrial environments.
FAQs
1. [What is a 2000LPH EDI system and why should my facility consider it over traditional ion exchange?]
An EDI (Electrodeionization) system, such as our MR-EDI-2TH, is a chemical-free water treatment solution that uses electricity, ion-exchange membranes, and resin to produce ultrapure water. Unlike traditional ion exchange beds that require hazardous chemical regeneration using acid and caustic, the 2000LPH EDI system operates as a continuous, electrically driven process. This eliminates the downtime associated with batch regeneration and addresses the high costs of chemical handling and wastewater neutralization. With a salt rejection rate of 99.99%, it is an ideal post-Reverse Osmosis (RO) solution for industries in Europe and Southeast Asia seeking sustainable, "green" water treatment. By choosing this technology, you significantly reduce your facility's physical footprint and total cost of ownership while maintaining a stable, high-resistivity water supply.2. [How can I verify the capacity and efficiency of a 2000LPH EDI system before purchasing?]
When evaluating a 2000LPH EDI system to verify a supplier's strength, you should focus on specific performance metrics and certifications. Guangdong Morui Environmental Technology Co.,Ltd, established in 2005, provides transparent technical data for the MR-EDI-2TH model, including a power consumption of 8.5kw/hour and a recovery rate of 55%. To ensure you are dealing with a reputable manufacturer, verify their ISO, CE, and ROHS certifications. We also recommend requesting a simulation report based on your specific feed water analysis. Key parameters to check are the system’s ability to handle your specific influent hardness and silica levels without scaling. If a supplier cannot provide detailed electrical stability data or recovery calculations, it may indicate a lack of technical depth. We invite you to contact Guangdong Morui for a detailed technical proposal to validate these parameters for your specific project.3. [What specific feed water quality is required to prevent scaling in a 2000LPH EDI system in regions like the Middle East or Africa?]
In regions like the Middle East or Africa, where source water often contains high mineral content, maintaining strict feed water quality is essential for the longevity of a 2000LPH EDI system. To prevent scaling—the accumulation of mineral deposits—the feed water entering the EDI stack must typically be pre-treated by a Double Pass RO system. The MR-EDI-2TH requires feed water with a total hardness of less than 1 ppm (as CaCO3) and reactive silica levels below 0.5 ppm. High hardness can lead to scaling on the membranes, which increases electrical resistance and reduces water purity. We suggest installing online resistivity and TOC (Total Organic Carbon) monitors to ensure the influent consistently meets these specifications. For projects in these regions, Guangdong Morui can provide customized pre-treatment configurations to protect the EDI membranes from local water challenges.4. [Does the 2000LPH EDI system meet international quality certifications for projects in Europe and South America?]
Yes, our 2000LPH EDI systems are designed to comply with rigorous international standards, which is a critical requirement for water treatment projects in Europe and South America. Guangdong Morui holds ISO, CE, and ROHS certifications, ensuring that the MR-EDI-2TH model meets essential safety, health, and environmental protection requirements. While these certifications cover the machine's construction and electrical safety, we always advise clients that local regulations regarding wastewater discharge or specific industrial water grades may vary. Generally, these systems meet the most stringent ultrapure water requirements for electronics and pharmaceuticals. Since 2005, we have provided comprehensive documentation and quality control reports to help our international clients navigate local compliance and customs procedures. Please consult with our technical team to confirm that the system meets the specific regulatory framework of your project location.5. [Can Guangdong Morui provide technical support and installation guidance for a 2000LPH EDI system in Southeast Asia or Africa?]
Guangdong Morui Environmental Technology Co.,Ltd offers extensive technical support for our 2000LPH EDI systems in all target markets, including Southeast Asia and Africa. We recognize that remote project sites require robust support; therefore, we provide detailed installation manuals, remote video commissioning, and comprehensive operator training. Our support covers critical operational tasks, such as monitoring DC voltage for electrical current stability and performing microbial control to prevent biofilm formation. Since our establishment in 2005, we have developed a reliable logistics and service network to ensure that the MR-EDI-2TH is installed correctly and operates at peak efficiency. For large-scale industrial projects, we can also discuss on-site technical supervision options. We encourage you to share your project coordinates and local site conditions so we can tailor a support package that ensures the long-term success of your ultrapure water production.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.