



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
brackish water reverse osmosis supplier
Certified Brackish Water Reverse Osmosis Systems for Drinking Water Factories Worldwide
If you buy water treatment equipment in South America, Southeast Asia, or the Middle East, reliability is key. So does a brackish water reverse osmosis supplier's technical know-how. That's why vetting often begins with a close look at engineering competence. Brackish water reverse osmosis (BWRO) is a membrane-based process. It treats groundwater or surface water with more salt than freshwater, but much less than seawater. In the professional water treatment industry, these systems act as the primary filtration barrier. They turn high-TDS (Total Dissolved Solids) sources into high-purity water for industrial use and drinking.
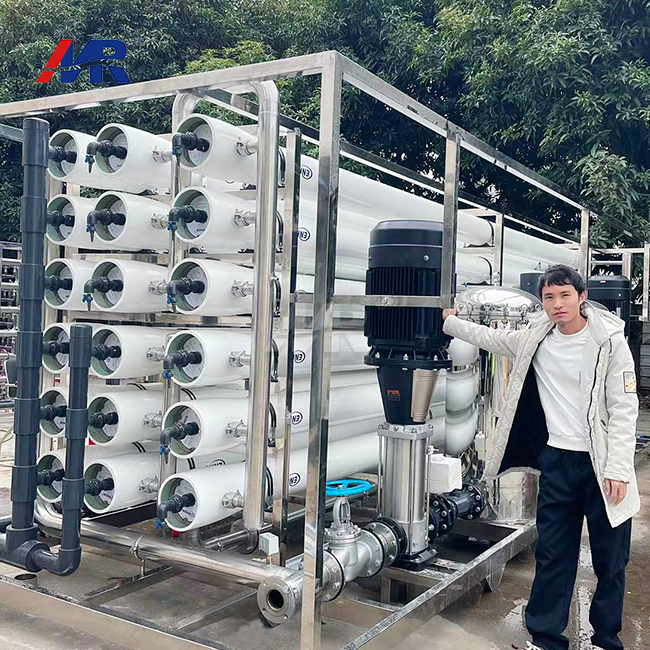
Water treatment plants in markets as varied as Africa and Southeast Asia run into their own set of problems. Local water safety rules tend to be strict, and procurement teams have to keep pace. On top of that, they face steady pressure to cut energy use, especially where utility prices swing. System stability is another headache, and picking the wrong brackish water reverse osmosis supplier only makes it worse. Weak membrane setups foul early and cause frequent downtime, particularly when groundwater quality keeps shifting. Shipping across borders adds more logistical work. Slow or unresponsive technical documentation can push project timelines back too. Both issues hit the bottom line of drinking water production facilities.
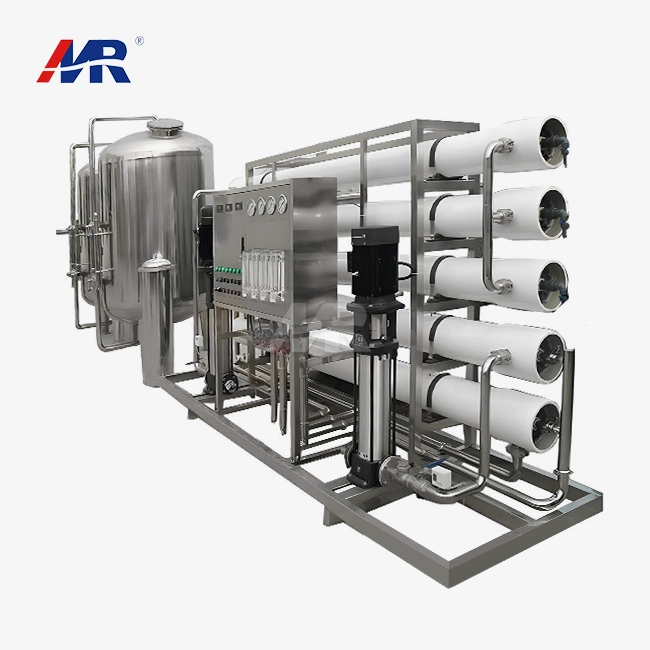
Guangdong Morui Environmental Technology Co., Ltd. has been in business since 2005. We build engineered brackish water reverse osmosis systems meant to solve these operational problems worldwide. Nearly two decades of manufacturing experience goes into every unit, and our systems bridge the gap between top technical performance and regional compliance. They carry ISO, CE, and ROHS certifications. For drinking water factories, our Model MR-BWRO-12TH pairs advanced automation with high-efficiency membrane modules. That keeps output consistently in line with international safety standards. We keep engineering transparent, offering detailed performance simulations and material specifications to help procurement managers through validation.
- Built for High-Volume Drinking Water: The MR-BWRO-12TH suits large drinking water factories. It runs at a steady 20kw/hour, striking a balance between operating costs and output volume.
- Strong Salt Management: We focus on building brackish water reverse osmosis systems. Our units deliver a 99% salt rejection rate. They remove dissolved solids, heavy metals, and organic contaminants, even from tough feed water sources.
- Global Compliance and Quality: Every system is built to strict international benchmarks. ISO and CE certifications back that up. That helps customs clearance and local regulatory approval go more smoothly in Europe and South America.
- Better Use of Resources: Our brackish water reverse osmosis systems reach a 70% recovery rate. That saves as much water as possible. It also cuts wastewater discharge sharply and makes the plant more sustainable overall.
- Regional Adaptability and Durability: The systems use premium pressure vessels and specialized pretreatment stages. This design helps them withstand the demanding environmental conditions found in Middle Eastern and African water treatment projects.
For a precise technical fit at a specific site, a recommended part of procurement is to review comprehensive system schematics and component lists. Talk to engineering teams about a detailed feed water analysis. Then you can fine-tune system parameters to match local power grids and specific water chemistry profiles. Technical data sheets and performance reports from existing installations in Southeast Asia and Europe give the necessary evidence for long-term reliability. The MR-BWRO-12TH configuration delivers consistent mineral removal and energy efficiency for large-scale industrial water purification requirements.




About Guangdong Morui Environmental Technology Co.,Ltd
Guangdong Morui Environmental Technology Co.,Ltd was founded in 2005. We're a leading manufacturer of industrial water treatment solutions, and with nearly 20 years in the field, we've grown into a dependable global supplier of high-performance brackish water reverse osmosis systems, and as a brackish water reverse osmosis supplier we help customers from critical sectors across South America, Southeast Asia, Europe, the Middle East, and Africa.
Our technical strength really shows in specialized equipment like the MR-BWRO-12TH, which we built for drinking water factories. These systems handle high TDS, and as a brackish water reverse osmosis supplier, we make sure they hit a 99% salt rejection rate and a 70% recovery rate. They also keep power consumption at 20kw/hour. That's what helps international bottling plants and industrial facilities maximize output while meeting strict global safety standards.
Quality is the foundation of our work. Our facility follows a strict ISO-certified management system, and every product meets CE and ROHS requirements. We use advanced testing equipment to check each brackish water reverse osmosis unit before it ships. That's how we make sure it delivers steady performance and durability. We also maintain a high on-time delivery rate for complex international projects.
Morui provides full technical support for our global markets to help with long-term operation. This covers remote debugging, on-site technical training, and maintenance guidance. It's all meant to keep your water treatment infrastructure running at peak efficiency. Partner with Guangdong Morui for scalable, high-rejection water solutions backed by proven manufacturing excellence.

Sustainable Brackish Water Desalination for Global Drinking Water Factories
Application Scenarios Overview
Brackish water reverse osmosis (BWRO) is a workhorse technology worldwide. It turns high-salinity groundwater or surface water into drinking water. Drinking water factories count on a dependable brackish water reverse osmosis supplier most when they need a steady supply of high-purity mineral water. These systems also matter for food and beverage processing and for pharmaceutical-grade utility water, not just city water supplies. In those roles, feed quality has to stay consistent even when raw water quality shifts.
What Customers Struggle With
Water scarcity brings its own technical headaches in places like the Middle East, Southeast Asia, and Africa. Well water with high Total Dissolved Solids (TDS) can, as any brackish water reverse osmosis supplier will tell you, foul standard membranes fast. That leads to more downtime and higher chemical cleaning costs. Operators in South America and Europe have strict rules to meet as well, including CE and ROHS standards. Their systems need to deliver high output while keeping environmental impact low.
Energy waste is another major barrier. If pressure management is not optimized, the operational cost (OpEx) of desalination can hurt a drinking water factory's profits. In remote areas, local technical expertise is often hard to find. That makes reliability and easy maintenance the main concerns for long-term investment.
Guangdong Morui Environmental Technology Co.,Ltd BWRO Solution
Guangdong Morui Environmental Technology Co.,Ltd was founded in 2005. The company offers a complete modular brackish water reverse osmosis solution that can be deployed quickly and built to withstand heavy industrial use. The MR-BWRO-12TH platform sits at the center of the solution. It is a turnkey system made specifically for drinking water bottling lines. Advanced filtration works with smart automation to turn difficult brackish sources into high-quality water that meets global safety standards.
System Architecture and Key Components
The system is built around a multi-stage design. This design helps it achieve the longest membrane life and the best output quality.
- Pre-treatment Unit: Multi-media and carbon filtration pull out suspended solids and chlorine. That protects the sensitive RO membranes, so they last longer instead of breaking down early.
- MR-BWRO-12TH Mainframe: The high-rejection membrane elements inside hit a 99% salt rejection rate. That takes out dissolved minerals, heavy metals, and pathogens.
- Energy Management System: It draws only 20kw/hour. Even so, it handles high-pressure demand and keeps electrical use in check.
- Control and Automation: PLCs are integrated into the system and track the 70% recovery rate in real time. They adjust flow parameters to stop scaling and raise yield.
What the Solution Offers, in Measurable Terms
- High Efficiency: Water recovery reaches 70%, so wastewater discharge falls sharply compared with standard systems.
- Operational Economy: A 20kw/h power profile keeps the carbon footprint low. It also trims monthly utility bills for large factories.
- Certified Quality: The product carries full ISO, CE, and ROHS certification. That opens the door to global markets and meets safety compliance.
- Proven Reliability: Nearly two decades of engineering expertise go into every unit, which keeps unscheduled maintenance to a minimum.
- Superior Purification: Salt rejection runs at 99%, so the finished product meets premium drinking water standards every time.
Implementation and Service Capability
Guangdong Morui Environmental Technology Co.,Ltd supports the full project lifecycle. That covers initial water analysis, custom scheme design, manufacturing, and global logistics. On the technical side, we handle remote diagnostics and complete spare parts kits. This helps keep lead times short in Southeast Asia, the Middle East, and other regions. We also run professional training modules for local operators, so the system stays at peak performance throughout its service life.
Typical Application Scenario
A drinking water factory located in an arid region of the Middle East required a solution for high-salinity well water. By implementing the MR-BWRO-12TH system, the facility replaced an aging, inefficient plant. The transition resulted in a stabilized production of 12 tons per hour, a 25% reduction in energy overhead, and a consistent output quality that passed all local health department audits for bottled water distribution.
The modular architecture facilitates rapid deployment across diverse geological conditions while maintaining high-purity output through advanced membrane separation technology.
FAQs
1. What is brackish water reverse osmosis, and how does it benefit a drinking water factory?
Brackish water reverse osmosis (BWRO) is a specialized membrane filtration process designed to treat water with a higher salinity level than fresh water but lower than seawater—typically found in wells, rivers, or estuaries. For a drinking water factory, implementing a system like the Guangdong Morui MR-BWRO-12TH ensures the removal of up to 99% of dissolved salts, heavy metals, and contaminants. This technology is vital for producing high-quality bottled or tap water that meets stringent health standards. By utilizing high-pressure pumps to force water through semi-permeable membranes, the system achieves a high recovery rate of approximately 70%, minimizing wastewater. When selecting a system, ensure the salt rejection rate and energy efficiency align with your production goals. For factories requiring specific output volumes, we recommend consulting our technical team to match the system capacity with your source water TDS (Total Dissolved Solids) profile.2. How do I choose the right brackish water desalination system for high TDS groundwater?
Choosing the correct brackish water reverse osmosis equipment requires a detailed analysis of your raw water quality and intended application. First, obtain a comprehensive water chemistry report focusing on TDS, hardness, and silica levels, as these dictate the necessary pre-treatment stages to prevent membrane scaling. Second, consider the energy footprint; for instance, a standard industrial model may consume around 20kw/hour to maintain optimal pressure. Finally, verify the manufacturer’s track record. Guangdong Morui Environmental Technology Co.,Ltd has been engineering water treatment solutions since 2005, ensuring that our systems are built for long-term durability. We suggest looking for systems with modular designs that allow for future scaling. If you are uncertain about your local water parameters, our engineers can provide a customized projection to ensure the system delivers the 99% salt rejection required for your specific site conditions.3. What are the typical energy consumption and recovery rate expectations for industrial BWRO units in Southeast Asia and Africa?
In regions like Southeast Asia and Africa, where operational costs and water scarcity are primary concerns, energy efficiency and recovery rates are critical metrics. A high-performance brackish water reverse osmosis system, such as the MR-BWRO-12TH, is engineered to balance these factors, typically operating at a recovery rate of 70%. This means 70% of the input water is converted into high-quality permeate, significantly reducing raw water waste. Energy consumption for these industrial units is approximately 20kw/hour, depending on the feed water salinity and temperature. To optimize performance in hot or humid climates, we recommend regular maintenance of the high-pressure pumps and monitoring membrane fouling. Because local electricity stability varies, it is also wise to consider surge protection for the control systems. Contact Guangdong Morui for a detailed energy consumption analysis based on your local utility costs and water source characteristics.4. Does the brackish water reverse osmosis equipment meet international standards for the European or South American markets?
Yes, high-quality brackish water reverse osmosis systems must adhere to rigorous international standards to ensure safety and performance. Guangdong Morui holds ISO, CE, and ROHS certifications, which are essential for entering the European and South American markets. These certifications verify that the equipment meets strict health, safety, and environmental protection requirements. While our systems are designed to comply with global benchmarks, including a 99% salt rejection rate for drinking water applications, it is important to note that specific countries may have additional local regulations regarding water discharge or electrical configurations. We generally recommend that clients verify local import standards and water quality mandates with regional authorities. Our team can provide the necessary technical documentation and certification copies to facilitate the compliance process for your specific project in South America, Europe, or the Middle East.5. How does Guangdong Morui ensure technical support and system reliability for projects in the Middle East and Africa?
Reliability in harsh environments, such as the Middle East or Africa, is a hallmark of Guangdong Morui Environmental Technology Co.,Ltd’s engineering approach. Since our establishment in 2005, we have optimized our brackish water reverse osmosis systems to withstand high ambient temperatures and varying source water qualities. We provide comprehensive technical support, which includes detailed installation manuals, video guidance, and remote troubleshooting. For large-scale drinking water factory projects, we can discuss onsite commissioning and staff training to ensure your team can maintain the 70% recovery rate and 99% salt rejection performance. Our systems use high-grade components that are globally sourcable, simplifying long-term maintenance. We suggest keeping a stock of essential consumables, such as pre-filters and membranes, to prevent downtime. If you are planning a project in these regions, please share your raw water parameters so we can design a robust system tailored to your local environment.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.