



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
containerized RO equipment supplier
High-Performance Containerized RO Equipment for Industrial Water Treatment Around the World
Procurement managers and engineers in South America, Southeast Asia, Europe, the Middle East, and Africa know how much rides on securing a reliable source. The right source keeps operations stable for years, so it pays to find a reliable containerized RO equipment supplier who understands your site's specific needs. In industrial water treatment, these systems work like mobile, plug-and-play plants. They convert brackish or contaminated water into high-purity process water, and they scale to fit remote sites, construction camps, and municipal backup.
Even so, sourcing containerized RO equipment for international projects comes with serious challenges. In regions like Southeast Asia or Africa, power grids fluctuate and ambient temperatures stay high. That can foul membranes early and lead to unexpected downtime. Many procurement teams also struggle to meet local environmental regulations and international safety standards like CE or ROHS, even with a containerized RO equipment supplier on board. Add high operating costs from heavy energy use, plus no immediate technical support for complex media filtration systems, and the return on investment for large-scale water treatment infrastructure can suffer.
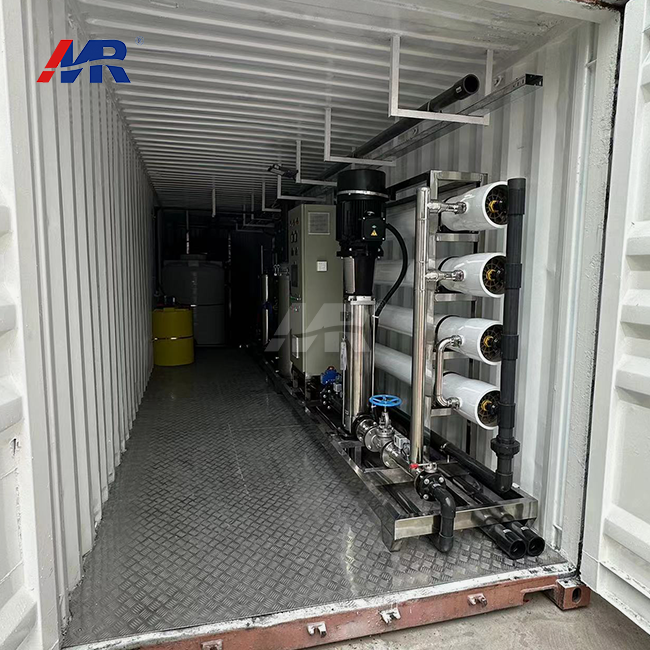
Guangdong Morui Environmental Technology Co., Ltd., established in 2005, addresses these challenges by acting as a technically grounded containerized RO equipment manufacturer. With nearly two decades of expertise, our team specializes in engineering containerized RO equipment solutions that balance durability with energy efficiency. Our systems, such as the Model MR-CTRO-25TH, are designed specifically for the rigorous demands of the Middle East's high-salinity environments and South America's diverse industrial landscapes. By integrating the entire treatment process—from media filtration to Brackish Water Reverse Osmosis (BWRO)—within a standard ISO shipping container, we eliminate the need for extensive civil works and reduce onsite installation time by up to 80%.
Our containerized RO equipment offers several distinct technical advantages tailored for professional procurement verification:
- Industrial-Grade Efficiency: The MR-CTRO-25TH model runs at 32kw/hour, a power consumption level optimized for sites in Africa and Southeast Asia, where energy costs are a primary concern.
- High-Purity Performance: Salt rejection sits at 98%. That means the output water meets strict industrial standards, whether it goes to boiler feed or pharmaceutical processes.
- Verified Compliance: Every unit comes from ISO-certified manufacturing. They also carry CE and ROHS certifications, which satisfy the strict rules of European and South American markets.
- Optimized Recovery Rates: The system achieves a recovery rate of 55-65%, significantly reducing wastewater discharge and improving overall water treatment resource management.
- Durable Pre-treatment Logic: The inclusion of advanced media filters protects the BWRO membranes from suspended solids, extending the lifecycle of the core components in harsh environments.
Picking a partner for complex water treatment work takes real knowledge of membrane chemistry and mechanical engineering. We've been in the industry for 20 years. That lets us provide complete technical documentation, fast spare parts response, and modular designs that scale up as project demands grow.
Integrated BWRO technology and automated controls create a self-contained setup. It keeps water quality steady, even when feed water conditions shift.




About Guangdong Morui Environmental Technology Co.,Ltd
Founded in 2005, Guangdong Morui Environmental Technology Co.,Ltd is a professional manufacturer focused on advanced industrial water treatment solutions. With nearly two decades of engineering experience under our belt, we have grown into a trusted containerized RO equipment supplier, delivering high-performance systems for critical infrastructure and industrial projects throughout South America, Southeast Asia, Europe, the Middle East, and Africa.
We build containerized RO equipment for fast deployment in tough places. Remote mining sites, construction camps, and decentralized municipal facilities are typical examples. Our specialty is plug-and-play modular design, and the MR-CTRO-25TH series shows how it works. These units, from a containerized RO equipment supplier, put multi-media filtration and BWRO technology inside standard ISO containers. They are made to save space and hold up under hard use, and they keep a 98% salt rejection rate even in harsh climates.
Morui follows strict ISO, CE, and ROHS standards and keeps a rigorous quality management system. Our factory keeps assembly precise, so modular units achieve a consistent recovery rate of 55-65%. We back the hardware with full technical support, including remote commissioning, onsite training, and localized maintenance that matches the logistics each international client needs.
Morui is committed to sustainable, scalable water treatment solutions that keep your water supply secure. Explore our technical configurations, and partner with us for operational excellence over the long term.

High-Efficiency Containerized RO Solutions for Sustainable Water Supply
Overview of Application Scenarios
Industry and cities don't treat water in one central spot anymore. Demand pops up wherever it pops up, so purification needs to be easy to move and reliable. That's where a containerized RO equipment supplier comes in. It's a good fit for places where building permanent infrastructure isn't possible or would take too long. Here are the common cases:
- Remote Industrial Operations: Mines in South America and construction camps in Africa sit in isolated areas. Each site needs high-purity process water and drinking water right there, so a containerized RO equipment supplier often becomes the go-to solution.
- Emergency and Disaster Relief: When a natural disaster strikes or infrastructure fails, clean water has to get there fast. This happens often in Southeast Asia and the Middle East.
- Commercial Decentralization: Island resorts and remote coastal sites use self-contained desalination units. The local municipal grid cannot meet their needs.
Key Pain Points and Regional Challenges
When you run water treatment systems in markets as different as Europe, the Middle East, and Southeast Asia, you face tough regulatory and environmental challenges:
- Strict Compliance: In Europe and the Middle East, you have to meet ISO, CE, and ROHS standards. Miss those quality benchmarks and you risk legal penalties, or a shutdown of operations.
- Environmental Extremes: The Middle East brings high salinity. Southeast Asia brings high humidity and organic fouling. Either one can wear down standard equipment. Without a design built for these conditions, membrane life falls fast.
- Operational Overheads: High energy costs and the scarcity of skilled technicians in remote areas make automation and energy efficiency (such as the 32kw/h threshold) critical for maintaining profitability.
Guangdong Morui’s Integrated Solution
Since 2005, Guangdong Morui Environmental Technology Co., Ltd. has specialized in bridging the gap between large-scale plant performance and mobile flexibility. Our containerized RO equipment solutions are designed as "Plug-and-Play" turnkey systems. By integrating filtration, membrane separation, and smart control within a single ISO-standard shipping container, we eliminate the need for extensive civil works and reduce onsite installation time by up to 80%.
System Architecture and Key Components
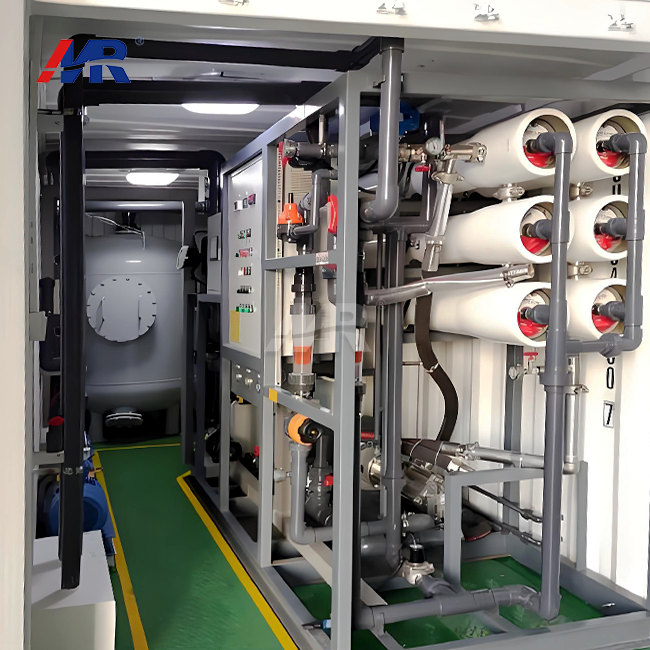
Our flagship Model MR-CTRO-25TH utilizes a sophisticated multi-stage process optimized for diverse water chemistries:
1. Pre-treatment Unit
This stage runs high-efficiency media filters. They pull out suspended solids and turbidity, which keeps the membranes downstream from fouling too soon. That counts most with high-turbidity sources in Southeast Asian river basins.
2. BWRO Membrane Module
Premium Brackish Water Reverse Osmosis (BWRO) membranes sit at the heart of the system. Built for a 98% salt rejection rate, this module makes sure the output meets the highest purity standards for both industrial and drinking use.
3. Control System and Automation
A centralized PLC system provides fully automated operation. It monitors critical parameters like flow rates and pressure, allowing for remote diagnostics which is essential for projects in Africa and South America where local technical support may be limited.
4. Integrated Maintenance (CIP)
A built-in Clean-in-Place (CIP) module is part of the system. It takes care of automated chemical cleaning for the membranes. This maintains the 55-65% recovery rate and extends the equipment lifecycle, with no manual intervention required.
Advantages and Measurable Benefits of the Solution
- Superior Purification: Salt rejection stays steady at 98%, so water quality remains reliable.
- Energy Optimization: The advanced hydraulic design keeps power use at 32kw/h or below. Over time, that lowers your operating costs.
- Space Efficiency: All parts are skid-mounted inside a 20ft or 40ft container. That saves you valuable land.
- Fast Setup: We test and pre-commission every unit at the factory. It's ready to run as soon as it reaches your site.
- Global Compliance: Our units come with full ISO, CE, and ROHS certification. That makes them easy to place in international markets.
Implementation and Service Capability
Guangdong Morui covers the full service cycle. We start with water analysis and a customized design plan, then stay with you through global logistics and remote monitoring. Customers in the Middle East and Southeast Asia get spare parts supply chains built for quick delivery, along with remote technical support, so performance stays at zero downtime.
Typical Application Example
A remote mining facility in South America faced high salinity in local groundwater and a lack of local construction resources. By deploying the MR-CTRO-25TH containerized solution, the client achieved:
- Immediate potable water supply within 48 hours of delivery.
- A stable 60% water recovery rate despite fluctuating feed water quality.
- Significant reduction in energy overheads compared to traditional onsite builds.
To receive a customized technical proposal based on your specific raw water parameters, please provide your site conditions for a detailed selection report.
Standardized ISO shipping containers provide the ultimate protection and mobility for high-performance brackish water desalination systems.
FAQs
1. [What are the primary advantages of investing in containerized RO equipment for industrial water treatment?]
Containerized RO equipment, such as the modular solutions designed by Guangdong Morui Environmental Technology Co.,Ltd since 2005, offers a sophisticated "plug-and-play" alternative to traditional site-built plants. These systems house the entire treatment process—including media filters and BWRO (Brackish Water Reverse Osmosis) membranes—within a single, weather-resistant shipping container. This design is particularly beneficial for projects in Southeast Asia and Africa, as it eliminates the need for extensive civil engineering and reduces installation time by up to 80%. By integrating all components into one unit, businesses can maximize their footprint while ensuring the equipment is protected from harsh external elements. When verifying a supplier's capability, look for systems that offer automated PLC controls and pre-wired configurations, which ensure that the equipment is ready to produce high-quality water immediately upon arrival and connection to a power source.2. [How do I determine if a specific model, like the MR-CTRO-25TH, meets my facility's energy and recovery requirements?]
Choosing the right containerized RO equipment requires a careful analysis of water recovery and energy efficiency. For example, our MR-CTRO-25TH model is engineered for industrial efficiency, featuring a recovery rate of 55-65% and an impressive salt rejection rate of 98%. With a power consumption of approximately 32kw/hour, it balances high-volume output with manageable operational costs. To ensure the model fits your needs, you should first conduct a comprehensive raw water analysis to determine Total Dissolved Solids (TDS) levels. We recommend that clients in energy-sensitive markets, such as Europe or the Middle East, prioritize systems with High-Pressure Pumps equipped with Variable Frequency Drives (VFDs) to optimize energy use. For a detailed calculation of potential OPEX savings based on your local utility costs, you should contact Guangdong Morui for a customized technical proposal tailored to your specific project parameters.3. [For projects in the Middle East or Southeast Asia, how does this equipment handle high-salinity source water and potential membrane fouling?]
In regions like the Middle East or Southeast Asia, where raw water may have high salinity or organic loading, containerized RO equipment must be equipped with robust pre-treatment to prevent "fouling" (the accumulation of unwanted material on membrane surfaces). The MR-CTRO-25TH system addresses this by utilizing a multi-stage media filter process before the water reaches the BWRO membranes. This pre-treatment effectively removes suspended solids that could otherwise cause "scaling" or mineral buildup. To maintain a consistent 98% salt rejection rate, we incorporate chemical dosing systems and Clean-in-Place (CIP) units within the container. We suggest that operators in these regions strictly follow the recommended backwash schedules for the media filters. If your source water has unique chemical characteristics, Guangdong Morui can customize the filtration media and membrane selection to ensure long-term stability and prevent frequent, costly membrane replacements.4. [What international certifications and standards should I look for when importing containerized RO equipment to Europe or South America?]
Importing water treatment technology into Europe or South America involves strict adherence to safety and quality regulations. It is essential to choose containerized RO equipment that carries ISO, CE, and ROHS certifications. These credentials verify that the system’s pressure vessels, electrical wiring, and material safety meet international benchmarks. For instance, the CE mark is a mandatory requirement for the European Economic Area, ensuring the machinery meets health and safety standards. Guangdong Morui, established in 2005, ensures all export models comply with these global quality management systems. However, since environmental regulations regarding brine discharge (the concentrated salt water left over) can vary significantly by country, we recommend consulting with local authorities to confirm specific discharge permits. Our team can provide the necessary technical documentation to assist with your local compliance and permitting process in any target market.5. [Can Guangdong Morui provide technical support and installation guidance for containerized RO systems in remote regions like Africa?]
Yes, supporting containerized RO equipment in remote locations, such as mining sites in Africa or rural developments in South America, is a core competency of Guangdong Morui Environmental Technology Co.,Ltd. Because our systems are factory-tested and pre-plumbed, they arrive as turnkey units that require minimal local technical expertise to commission. We provide comprehensive digital installation manuals, video tutorials, and remote technical support via PLC diagnostics where available. For large-scale industrial installations, we can also arrange for onsite engineering support to train your local staff on routine maintenance and membrane cleaning procedures. We strongly advise clients in remote areas to maintain a "critical spares kit," including cartridge filters and specific seals, to ensure zero downtime. Please reach out to our technical department with your site coordinates and water quality reports so we can design a specialized logistics and support strategy for your project.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.