



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
container reverse osmosis equipment supplier
Scalable Container Reverse Osmosis Equipment for Global Industrial Desalination
For procurement managers and engineers in South America, Southeast Asia, and the Middle East, finding a container reverse osmosis equipment supplier you can rely on is a critical step toward long-term water security. Industrial demand for purified water keeps climbing, and these modular units meet it with a plug-and-play setup built for underground water desalination and process water preparation. What you get is a treatment plant on site, mobile and able to handle rough weather.
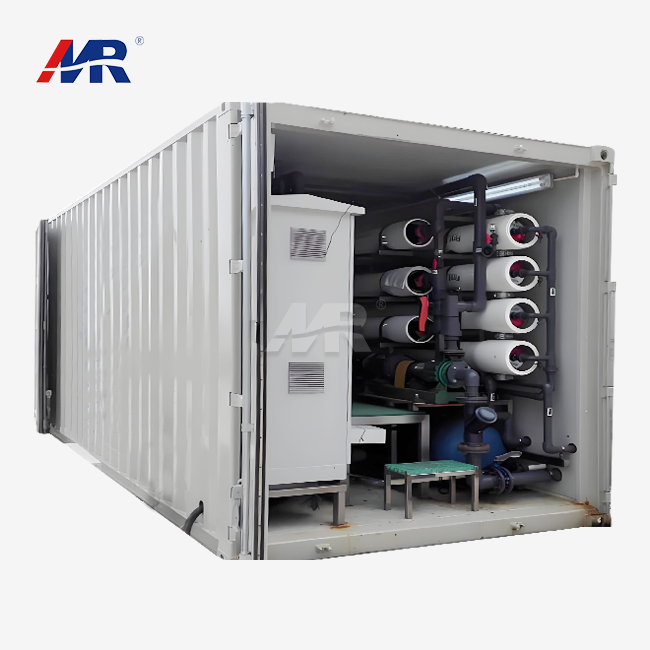
B2B buyers in the global water treatment market, especially in Africa and Europe, often run into real operational problems. Environmental rules are getting tighter, and international standards like ISO and CE mean equipment has to clear strict safety and quality benchmarks. Energy use is another pressure point, too: high consumption drives up operating expenditure (OPEX) and can put a project's feasibility at risk. When a system is built without the specialized engineering a container reverse osmosis equipment supplier brings, membranes tend to foul early and maintenance costs run high, particularly with feedwater whose salinity keeps shifting. At remote industrial sites, long delivery cycles and no immediate technical support for complex desalination units often mean costly downtime.
Guangdong Morui Environmental Technology Co.,Ltd, founded in 2005, closes these gaps with high-performance container reverse osmosis equipment made for tough industrial conditions. Nearly two decades of experience go into systems that hold ISO, CE, and ROHS certifications, so water treatment clients around the world get hardware that meets international safety and durability standards. Our flagship unit, the MR-CTRO-25TH, was built for underground water desalination and strikes a balance between high output and efficient energy use. It is engineered around the source water profiles common in Southeast Asian and Middle Eastern groundwater, and uses industrial-grade components to get the longest possible life out of the reverse osmosis membranes.
To ensure procurement managers can verify the technical strength of these solutions, the following core advantages define our current containerized offerings:
- Precise desalination performance: the MR-CTRO-25TH delivers a salt rejection rate of 98%, which means high-purity permeate for industrial use.
- Low energy use: at 32kw/hour, the system holds down running costs and still delivers high-pressure performance.
- Strong recovery numbers: a 55-65% recovery rate means far less brine is discharged than with traditional standalone units.
- Certified build quality: every unit is made under ISO 9001 and carries CE and ROHS certification, so it meets legal requirements for European and South American markets.
- Modular and built to last: the equipment ships in standard containers, uses corrosion-resistant internal piping, and runs on automated PLC controls for steady operation in remote regions.
Professional buyers should review detailed technical specifications and historical project data. That's how you judge whether these systems suit the water chemistry in a specific region. Look at the full technical documentation and performance charts. They let you compare efficiency metrics and long-term durability in detail. Talk with experienced application engineers, too. They can refine the configuration to meet site requirements for flow rates and permeate quality. The MR-CTRO-25TH model supports continuous 24/7 operation, backed by a robust architectural design optimized for underground water desalination.




About Guangdong Morui Environmental Technology Co.,Ltd
Guangdong Morui Environmental Technology Co.,Ltd was established in 2005. We're a leading manufacturer specializing in industrial water treatment. After nearly two decades of technical development, we've become a trusted global container reverse osmosis equipment supplier for high-performance systems. We deliver dependable solutions to markets around the world, including South America, Southeast Asia, Europe, the Middle East, and Africa.
Our expertise comes from tackling tough water problems, especially underground water desalination for industrial and municipal use, and as a container reverse osmosis equipment supplier we put that experience into our signature container reverse osmosis equipment, Model: MR-CTRO-25TH. It achieves a 98% salt rejection rate with optimized power consumption of 32kw/hour. These systems are built to last and deploy fast. Their modular designs meet the strict requirements of remote industrial sites and local brand factories.
Quality is the foundation of our operations. We hold ISO, CE, and ROHS certifications. Every unit goes through rigorous factory acceptance testing, from the corrosion-resistant piping to the PLC automated controls. Our commitment to excellence shows in our consistent on-time delivery and high-performance metrics that guarantee process stability.
Beyond equipment, we provide local technical support, including remote commissioning and on-site operator training. This helps our systems integrate smoothly in regions from Southeast Asia to the Middle East. Partnering with Morui means you get a reliable, long-term expert for your sustainable water security.

Integrated Containerized Desalination Solutions for Remote Global Markets
Application Scenarios Overview
Container reverse osmosis units are mobile infrastructure for industrial water treatment. They go where no permanent water system exists. Guangdong Morui Environmental Technology Co., Ltd, a container reverse osmosis equipment supplier, builds specialized systems for underground water desalination. That work matters for remote mining operations in South America, coastal construction sites in Southeast Asia, and agricultural irrigation projects in the Middle East and Africa. These systems turn high-salinity brackish water into high-purity process water, so operations can keep running in isolated places.
Pain Points and Challenges Customers Face
Setting up water treatment systems in emerging markets throws challenges at you that standard indoor units just are not built for, and that is where a container reverse osmosis equipment supplier can really help:
- Harsh Environmental Conditions: In places like the Middle East or Sub-Saharan Africa, intense heat and heavy dust can wear parts out fast.
- Energy constraints: As electricity prices rise, heavy power use adds real pressure to Total Cost of Ownership (TCO).
- Regulatory compliance: Companies that want to sell into European and South American markets have to meet CE, ROHS, and ISO standards. That calls for strict quality control.
- Maintenance hurdles: Skilled technicians are often unavailable at remote sites. A system outage there can be catastrophic for industrial productivity.
The Morui Containerized Solution
Morui has nearly two decades of experience going back to 2005. The company provides turnkey reverse osmosis equipment in containers. Our approach is built on a "Plug-and-Play" philosophy. The whole desalination plant sits inside a reinforced shipping container with climate control. This modular setup removes the need for complex civil works onsite. It also shields sensitive parts from extreme weather. The result is a stable water supply, no matter what the local site conditions are.
System Design and Main Components
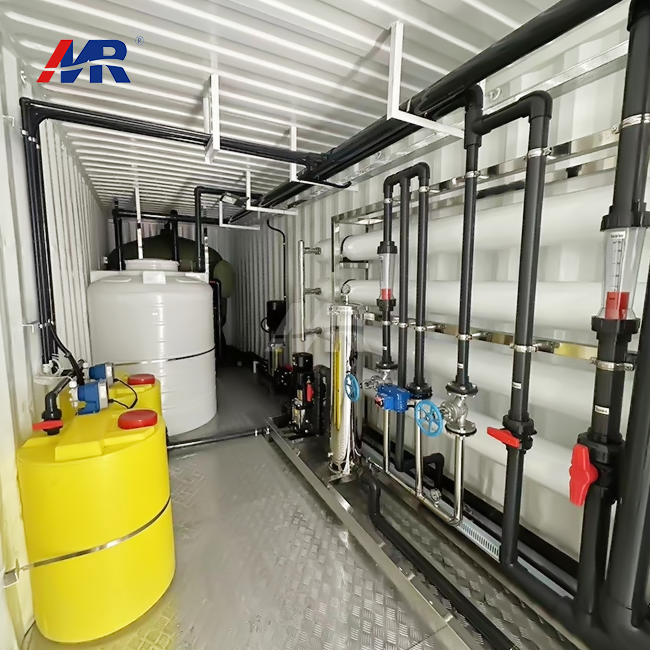
The MR-CTRO-25TH is built to last and run efficiently:
- Pre-treatment Unit: Multi-media filtration and anti-scalant dosing protect the membranes from fouling. Both are calibrated to match the underground water profile.
- RO Membrane Module: High-rejection membranes deliver a 98% salt rejection rate. That's key to meeting strict industrial water quality standards.
- Energy-Efficient Power Train: This unit is tuned to draw only 32kw/hour. Output stays high, and running costs stay low.
- Integrated Control System: PLC-based automation tracks flux and conductivity in real time. No one has to watch the line all day.
- Cleaning-in-Place (CIP) Module: Built-in maintenance loops let you run chemical cleaning fast and without fuss. That keeps your membranes in service longer.
Solution Advantages and Measurable Benefits
- Optimized recovery: It reaches a 55-65% recovery rate. That cuts wastewater discharge by a large margin next to standard portable units.
- Fast deployment: Because it comes in a container, onsite installation takes up to 80% less time than traditional builds.
- Energy savings: The advanced hydraulic design brings energy use down to levels that remote grids can sustain.
- Reliable purity: A steady 98% salt rejection rate protects high-value industrial equipment downstream.
- Global compliance. We hold full ISO, CE, and ROHS certification. Every system we ship meets international safety and quality standards.
Implementation and Service Capability
Guangdong Morui Environmental Technology Co., Ltd handles the whole lifecycle. It starts with the first water analysis and a custom scheme design, and runs through to factory FAT (Factory Acceptance Testing). For customers in South America, Southeast Asia, and the Middle East, we offer remote diagnostic support and quick spare parts dispatch, so downtime stays low. Localized commissioning support is part of the package too, which means each system gets tuned to the chemical makeup of the local feedwater.
Typical Application Case: Underground Water Desalination
A remote industrial site in Southeast Asia had a primary underground water source with high salinity, and that put equipment lifespan at risk. After the facility installed the MR-CTRO-25TH containerized solution, it secured a steady supply of 25m³/h of treated water. Maintenance costs for downstream equipment fell by 30%, and the system held a steady 60% recovery rate even as feed water TDS levels rose and fell.
The modular design means units go in fast and deliver the same water quality, wherever they are installed.
FAQs
1. What are the primary advantages of using container reverse osmosis equipment for remote industrial sites?
Container reverse osmosis equipment offers a "plug-and-play" solution that is particularly beneficial for remote projects in regions like Africa or Southeast Asia. Unlike traditional stationary plants, these systems are housed within reinforced shipping containers, providing immediate protection against harsh environmental conditions such as high humidity or sandstorms. Guangdong Morui Environmental Technology Co.,Ltd, with nearly two decades of expertise since 2005, designs these units to be mobile and easy to deploy. The self-contained nature minimizes on-site civil works and installation time. For industrial users, this means lower labor costs and the ability to relocate the entire water treatment facility if project requirements change. Our systems, such as the MR-CTRO-25TH, integrate all necessary filtration, pumping, and membrane stages into a single secure module, ensuring consistent water quality even in the most challenging geographical locations.2. How can I determine if the MR-CTRO-25TH model is suitable for my underground water desalination needs?
Choosing the right container reverse osmosis equipment depends heavily on your raw water quality and required output. The MR-CTRO-25TH model is specifically engineered for underground water desalination, featuring a robust salt rejection rate of 98%. When evaluating this system, you should consider three main parameters: your feed water TDS (Total Dissolved Solids), your required daily volume, and power availability. This model offers a recovery rate of 55-65%, meaning it efficiently converts raw water into purified product water while managing brine discharge effectively. With a power consumption of approximately 32kw/hour, it balances high-performance output with energy efficiency. We recommend providing a detailed water analysis report to Guangdong Morui so our engineers can verify if these standard parameters align with your specific borehole or well water conditions to ensure long-term membrane stability.3. What international certifications should I look for to ensure the reliability of a containerized RO system in Europe or South America?
When importing container reverse osmosis equipment into regulated markets like Europe or South America, certification is a critical indicator of both safety and supplier authenticity. Buyers should prioritize suppliers who hold ISO 9001 for quality management, alongside CE and ROHS certifications which ensure the electrical and material safety of the components. Guangdong Morui Environmental Technology Co.,Ltd maintains these rigorous standards to guarantee that every system meets international benchmarks. These certifications confirm that the pressure vessels, electrical panels, and membrane housings have undergone standardized testing. While these international marks provide a baseline for quality, we always advise clients to check local environmental and electrical regulations, as specific countries may have additional grid-tie or discharge requirements. Choosing a certified manufacturer who has been operating since 2005 provides an extra layer of security regarding the equipment's lifespan and the availability of replacement parts.4. For projects in Southeast Asia and the Middle East, how does the equipment handle high-salinity underground water and high ambient temperatures?
In regions like the Middle East and Southeast Asia, container reverse osmosis equipment must be adapted to handle both high-salinity feed water and extreme ambient heat. Our systems utilize high-rejection membranes and corrosion-resistant high-pressure pumps to maintain a 98% salt rejection rate, effectively turning brackish underground water into potable or process water. To combat heat, the containers can be equipped with integrated ventilation or thermal insulation to protect the sensitive PLC controllers and high-pressure components. The MR-CTRO-25TH model is designed for durability in these climates, maintaining a stable recovery rate of 55-65% even under continuous operation. Since high temperatures can affect water viscosity and membrane flux, Guangdong Morui provides customized scaling inhibitors and pre-treatment modules to prevent mineral buildup, ensuring the system operates efficiently at its 32kw/hour power rating without frequent emergency maintenance.5. What kind of technical support and maintenance can be expected for container reverse osmosis equipment installed in Africa?
Reliable technical support is a primary concern for operators in Africa. Guangdong Morui Environmental Technology Co.,Ltd addresses this by designing our container reverse osmosis equipment with user-friendly PLC (Programmable Logic Controller) interfaces that allow for easy monitoring of flow rates, pressure, and water conductivity. Because the units are fully assembled and tested at our factory before shipping, the onsite commissioning process is significantly simplified. For long-term maintenance, we provide comprehensive digital manuals and remote technical consultations to help local teams manage filter replacements and membrane cleaning (CIP) cycles. Our 2005 establishment ensures we have a mature supply chain for consumables. If your project involves complex underground water desalination, we can offer tailored guidance on pre-treatment configurations to extend the life of your membranes, and we encourage customers to reach out for a customized maintenance schedule based on their specific site conditions.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.