



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
500LPH EDI equipment supplier
Reliable 500LPH EDI Equipment for Ultrapure Water Production Around the World
Procurement managers across South America, Southeast Asia, Europe, the Middle East, and Africa need a 500LPH EDI equipment supplier they can count on. That trust is what keeps operations steady over the long haul. Electrodeionization (EDI) is one of the leading sustainable water treatment methods. It uses ion-exchange resins and electrical fields to produce ultrapure water. You don't have to haul or regenerate hazardous chemicals. As industries move toward greener technologies, EDI has become the go-to choice for plants that need high-resistivity water for pharmaceuticals, electronics, and power generation.
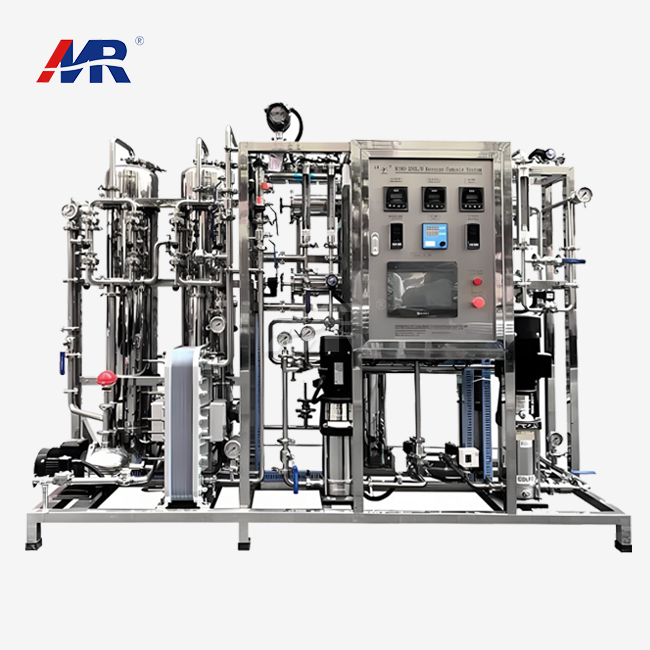
In regions like Southeast Asia and Africa, water treatment plants frequently have to work with source water that shifts in unpredictable ways. They also get hit with steep costs for hauling and disposing of chemicals. Procurement teams searching for a 500LPH EDI equipment supplier have real problems to solve. Wastewater discharge rules are tough. Energy prices across Europe keep climbing. And in remote industrial pockets of South America, finding dependable technical support for complex systems is a struggle. Another technical hurdle that keeps coming up is holding salt rejection above 99.9% while keeping power use low. If the equipment isn't built to precise standards, this can drive up operational expenditures (OPEX) and lead to membrane fouling more often.
Guangdong Morui Environmental Technology Co.,Ltd has been in business since 2005. The company supplies high-performance 500LPH EDI equipment built for critical industrial work. Its MR-EDI-500L model balances high output with energy efficiency. It is engineered to meet strict ISO, CE, and ROHS standards. With advanced electrochemical stacks, the 500LPH EDI equipment delivers a steady supply of ultrapure water. That removes the downtime that comes with traditional resin bed exhaustion. The company also provides full technical documentation and verification support. This helps buyers around the world confirm the authenticity and engineering rigor behind the manufacturing process.
A few technical and operational strengths stand out:
- Optimized Power Efficiency: The MR-EDI-500L draws a controlled 3kw/hour. For plants in high-tariff markets like Europe and the Middle East, that means lower energy bills.
- Superior Deionization Performance: This 500LPH EDI equipment reaches a 99.99% salt rejection rate, so sensitive industrial processes get the highest water resistivity.
- Sustainable Water Recovery: A steady 55% recovery rate keeps high-purity output strong while producing less wastewater. This supports environmental mandates in Southeast Asia and South America.
- Global compliance and durability. Every unit is built by an experienced 500LPH EDI equipment manufacturer with nearly 20 years of expertise. Each one is ISO and CE certified, so it fits smoothly into industrial frameworks worldwide.
- Rugged Industrial Design: The system is engineered to handle the varied feed water conditions typical of the water treatment industry in developing markets, ensuring consistent performance in diverse climates.
For professionals seeking to optimize ultrapure water infrastructure, exploring the detailed technical specifications and performance logs of the MR-EDI-500L facilitates a more informed procurement evaluation. Engineering teams can provide customized configurations that include detailed P&ID drawings and energy consumption forecasts to assist in technical validation.
The MR-EDI-500L delivers a consistent flow of ultrapure water through a chemical-free electrochemical process that maintains 99.99% salt rejection for demanding industrial applications.
Related Products




500LPH EDI Equipment from a Reliable Manufacturer
Founded in 2005, Guangdong Morui Environmental Technology Co., Ltd. is a specialized manufacturer that focuses on high-end water treatment systems. Nearly two decades later, we've grown into a leading 500LPH EDI equipment supplier, and our ultrapure water systems now serve industrial clients in South America, Southeast Asia, Europe, the Middle East, and Africa.
Our MR-EDI-500L series is designed for industries that need a steady supply of high-resistivity water without the environmental burden that comes with chemical regeneration. With advanced electrodeionization technology, we help pharmaceutical and electronics facilities achieve a 99.99% salt rejection rate, and as a 500LPH EDI equipment supplier, we also make sure these systems run efficiently, with low power consumption of just 3kw/hour, and they meet strict international standards.
Quality drives how we operate. Morui Environmental holds ISO certification. Our 500LPH EDI equipment carries CE and ROHS certifications, so it meets safety and environmental rules worldwide. We follow a strict quality control process. It supports a 98% on-time delivery rate and helps keep your infrastructure projects on schedule.
We back our global partners with a full set of technical services. That covers remote commissioning, training built around your site, and troubleshooting around the clock, 24/7. Upgrading an RO system you already run? Installing a new ultrapure water line? Either way, Morui Environmental gives you the technical reliability and long-term support that mission-critical operations depend on.

Sustainable Ultrapure Water Through Advanced 500LPH EDI Systems
Application Scenarios
In water treatment today, 500LPH EDI equipment is central to processes that need high-resistivity water and steady chemical conditions, so teams often turn to a 500LPH EDI equipment supplier for help. The system is used mostly in:
- Pharmaceutical and biotech production: For this, a dependable 500LPH EDI equipment supplier provides a system that delivers USP-grade purified water for making drugs and cleaning labs. Here, microbial control and ionic purity are what matter most.
- Electronics and semiconductor manufacturing: The system provides ultrapure water for wafer rinsing. Even a tiny amount of ionic contamination can lead to major yield losses.
- Power generation: It supplies high-pressure feed water for boilers, preventing scaling and corrosion. This extends equipment lifespan and thermal efficiency.
What Customers Struggle With
Ultrapure water systems cause different headaches depending on where you run them. Here is what South America, Southeast Asia, Europe, the Middle East, and Africa each bring:
- Tough Regulatory Standards: In Europe and the Middle East, you have to meet CE, ROHS, and ISO standards. There is no way around it. You also need paperwork proving your equipment is safe and environmentally sustainable.
- Steep Energy and Maintenance Bills: Electricity costs a lot in Europe and Southeast Asia, and skilled technicians are hard to find. So efficient systems and low-maintenance designs become a must.
- Chemical Handling Risks: Standard ion exchange depends on acids and caustics for regeneration. Handle those chemicals poorly and you are looking at safety hazards, plus an expensive job of neutralizing the wastewater.
Guangdong Morui’s 500LPH EDI Solution
Guangdong Morui Environmental Technology Co.,Ltd was founded in 2005. The MR-EDI-500L is our modular system, and it replaces traditional ion exchange beds. Electrodialysis and ion exchange work together in one continuous, chemical-free process. A DC electrical field regenerates the resin beads as the system runs, so the output stays steady at 500 LPH of ultrapure water. No downtime. No hazardous waste to discharge.
System Architecture and Key Components
The MR-EDI-500L ships as a turnkey system made up of several high-performance modules:
- EDI Membrane Stack: This core unit pairs ion-selective membranes with high-grade resins to reach a 99.99% salt rejection rate. Water quality stays consistent even when the feedwater profile shifts.
- Precision Control Unit: One central PLC runs the DC power supply and draws just 3kw/hour. That keeps the electrochemical regeneration process dialed in for the best energy efficiency you can get.
- Hydraulic Distribution Manifold: This module is designed to reach a 55% recovery rate. It saves water while still flushing concentrated ions off the membrane surface.
- Integrated Monitoring: Sensors track resistivity, flow rates, and pressure as they change. Early automated alerts mean membrane scaling or falling performance won't catch you by surprise.
Advantages and Measurable Benefits of the Solution
- Consistent purity. Salt rejection reaches 99.99%, so resistivity holds at up to 18.2 MΩ·cm.
- Efficient operation: Low power use of 3kw/hour cuts annual energy costs by about 20% compared with older EDI models.
- No chemicals required. You can drop bulk chemical storage and neutralization systems altogether, which cuts the physical footprint by 40%.
- Certified worldwide. Full ISO, CE, and ROHS certification means the system meets the tough safety and environmental rules that international markets require.
Implementation and Service Capability
Guangdong Morui supports global clients through a structured implementation lifecycle, from initial feedwater analysis to final site commission. With nearly two decades of expertise, we provide remote diagnostics and rapid spare parts dispatch to ensure minimal downtime in Middle Eastern and African regions. Technical training is provided to local operators to ensure long-term system stability and optimal performance.
Typical Application Case
A pharmaceutical lab in Southeast Asia needed a reliable supply of ultrapure water. Its old system kept breaking down because the resin was exhausted. Once the MR-EDI-500L was installed, the facility ran at a continuous 500LPH flow with no chemical handling at all. Within three months, the project had cut O&X costs by 30% and brought the site into full compliance with regional environmental discharge regulations.
Technical Consultation
Detailed system configurations and performance projections are available for specific industrial feedwater conditions to ensure optimal equipment selection.
The MR-EDI-500L system ensures stable ultrapure water production while maintaining low operational costs and environmental compliance.
FAQs
1. What defines a high-performance 500LPH EDI equipment for industrial ultrapure water production?
A high-performance 500LPH EDI equipment, such as our MR-EDI-500L, is characterized by its ability to produce consistent ultrapure water without chemical regeneration. Unlike traditional ion exchange, this system utilizes electrodeionization technology, combining ion-exchange resins and membranes with a DC electrical field. Key performance indicators to look for include a salt rejection rate of 99.99% and a stable recovery rate, which in our model is optimized at 55%. Additionally, energy efficiency is crucial; our system operates at a power consumption of approximately 3kw/hour. When selecting equipment, ensure it facilitates a continuous process that eliminates the need for hazardous acid and caustic handling, thereby reducing operational downtime and environmental impact. For specific flow requirements or water quality standards, we recommend consulting with Guangdong Morui to ensure the system configuration matches your local source water profile.2. How can I verify the reliability and expertise of an EDI system manufacturer like Guangdong Morui?
Verifying a supplier’s strength is essential for long-term project success. A reliable manufacturer should have extensive industry experience; for instance, Guangdong Morui Environmental Technology Co.,Ltd has been specializing in water treatment since 2005. You should look for international certifications such as ISO for quality management, alongside CE and ROHS compliance, which are vital for markets in Europe and Southeast Asia. A reputable provider will offer detailed technical specifications for their 500LPH EDI equipment and demonstrate a proven track record across diverse markets, including South America, the Middle East, and Africa. We suggest requesting case studies or technical documentation regarding the MR-EDI-500L to verify that the equipment can meet the stringent resistivity requirements of your specific industrial application.3. What regulatory and certification standards should my 500LPH EDI equipment meet for use in Europe or Southeast Asia?
When importing 500LPH EDI equipment to Europe, Southeast Asia, or the Middle East, compliance with international safety and environmental standards is paramount. Typically, equipment should carry the CE mark to demonstrate conformity with European health, safety, and environmental protection standards. ROHS certification is also critical to ensure the absence of hazardous substances in electrical components. Furthermore, an ISO-certified manufacturing process ensures consistent quality control. While these certifications are standard for Guangdong Morui products, specific regional regulations—such as local water discharge limits or electrical safety codes—may apply depending on the project location. We advise clients to confirm local compliance requirements during the planning phase. Our team can provide the necessary documentation for the MR-EDI-500L to facilitate smooth customs clearance and regulatory approval in your target market.4. How does the 500LPH EDI equipment handle feedwater variations in regions like the Middle East and Africa?
In regions like the Middle East and Africa, feedwater often presents challenges such as high salinity or fluctuating mineral content. The 500LPH EDI equipment is designed as a polishing stage, meaning it performs best when paired with a robust Reverse Osmosis (RO) pre-treatment system. Our MR-EDI-500L model features a 99.99% salt rejection rate, which ensures that even if the RO permeate has slight fluctuations, the EDI stack maintains the production of high-purity water. To optimize performance in these climates, it is important to monitor parameters like Silica and CO2 levels in the feed water, as these can impact the 55% recovery rate. We recommend a comprehensive water analysis before installation so that Guangdong Morui can suggest the ideal pre-treatment configuration to protect the EDI membranes and maintain the 3kw/hour energy efficiency.5. Can Guangdong Morui provide technical support and installation guidance for projects in South America or Southeast Asia?
Yes, Guangdong Morui provides comprehensive technical support for our international clients across South America, Southeast Asia, and beyond. Since 2005, we have developed a robust support framework that includes detailed installation manuals, remote video commissioning assistance, and deep-dive technical consultations. For the 500LPH EDI equipment, we provide precise electrical and plumbing schematics to ensure your local engineering team can integrate the MR-EDI-500L seamlessly into your existing water plant. While the system is designed for high durability and minimal maintenance, we offer guidance on routine membrane cleaning and stack voltage optimization. If your project requires specific on-site training or site-specific adjustments due to local environmental conditions, please contact us to discuss a tailored service agreement that ensures the long-term reliability of your ultrapure water supply.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.