

Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
membrane bioreactor supplier
Verified Membrane Bioreactor Systems for International Water Infrastructure
For procurement managers seeking a verified membrane bioreactor manufacturer in South America, Southeast Asia, Europe, the Middle East, or Africa, ensuring technical reliability and supplier authenticity is the first step toward project success. A membrane bioreactor (MBR) represents the pinnacle of modern water treatment technology, integrating biological degradation with advanced membrane filtration to replace traditional secondary clarifiers. This dual-action process ensures the removal of suspended solids and pathogens, producing high-quality permeate that meets increasingly stringent global environmental standards.
In the complex landscape of global water treatment, operators frequently encounter challenges ranging from strict regional discharge regulations to extreme land scarcity for facility expansion. In regions like Southeast Asia and the Middle East, high-salinity or high-temperature influent can compromise the stability of biological systems, while European markets demand rigorous compliance with CE and ROHS standards. Common pain points include high operational energy costs, frequent membrane fouling requiring intensive chemical cleaning, and the logistical difficulty of securing technical support and spare parts in remote project sites. These factors make the selection of a robust, certified filtration system essential for maintaining continuous operation and minimizing lifecycle costs.
Guangdong Morui Environmental Technology Co., Ltd, established in 2005, provides specialized membrane bioreactor solutions designed to address these specific industrial and municipal challenges. As an ISO-certified manufacturer, the company focuses on delivering high-durability filtration components that streamline the procurement process for international engineers. The flagship Model MR-MBR-193 utilizes premium PVDF material, known for its superior mechanical strength and chemical resistance, to ensure long-term stability in diverse climates from the humid tropics of Southeast Asia to the arid regions of Africa. These systems are engineered to facilitate rapid installation and integration, backed by nearly two decades of expertise in the water treatment sector.
Key technical advantages of these systems include:
- Advanced PVDF Membrane Material: The use of high-quality PVDF with a 0.2µm micron rating provides a precise physical barrier against bacteria and solids, ensuring consistent effluent quality for industrial reuse.
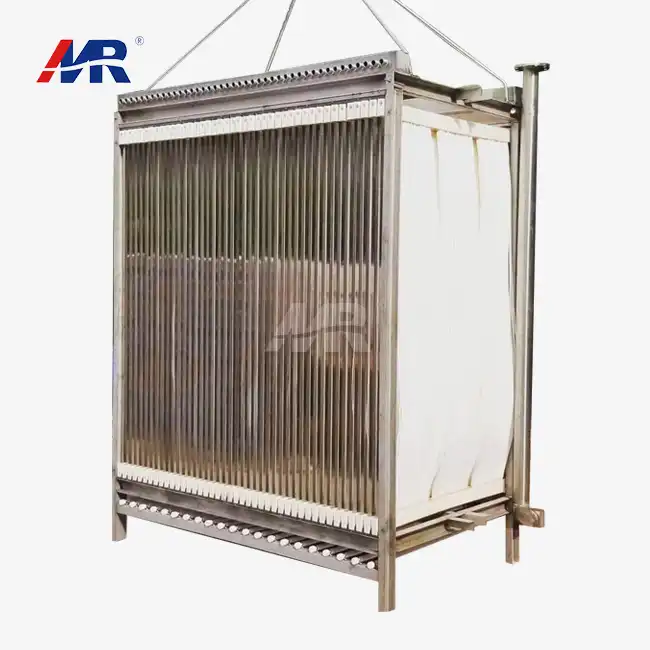
- Optimized Filtration Surface: Each MR-MBR-193 unit offers an effective filtration area of 22.4m², allowing for high-volume processing within a compact dimension of 1300x1250x30mm to maximize space efficiency.
- International Regulatory Compliance: Full adherence to ISO, CE, and ROHS standards ensures that these membrane bioreactor solutions meet the legal and safety requirements of European and South American markets.
- Reduced Operational Maintenance: The specialized 0.2um pore structure and material properties are designed to minimize fouling rates, thereby reducing the frequency of backwashing and chemical consumption.
- Proven Manufacturing Legacy: With a production history dating back to 2005, the manufacturing process incorporates rigorous quality control measures to guarantee the structural integrity of every membrane module.
Navigating the complexities of large-scale water treatment projects requires access to detailed technical documentation and verified performance data. Procurement teams can access comprehensive specifications and compatibility charts to ensure that the chosen filtration technology aligns with local environmental regulations and specific plant configurations. Expert technical consultation is available to assist in system sizing and the optimization of biological treatment parameters for various effluent profiles. High-precision filtration through 0.2µm PVDF membranes ensures consistent effluent quality across diverse industrial and municipal wastewater applications.
Related Products
About Guangdong Morui Environmental Technology Co., Ltd.
Guangdong Morui Environmental Technology Co., Ltd. has been dedicated to water treatment since 2005, and as a membrane bioreactor supplier, we design and build high-performance membrane bioreactor systems. Our customers come from South America, Southeast Asia, Europe, the Middle East, and Africa.
We've got close to twenty years of hands-on experience, and we know high-durability PVDF microfiltration inside and out. Take our flagship MR-MBR-193 series. It runs a 0.2um pore size and replaces traditional secondary clarifiers, so solid-liquid separation works better. We build these systems, as a membrane bioreactor supplier, to yield high-purity permeate that suits industrial reuse and irrigation. That answers real problems at municipal wastewater plants and large industrial sites.
ISO, CE, and ROHS certifications stand behind our reliability claims. Every 22.4m² membrane unit goes through a strict quality management system and advanced testing protocols. That is how we keep a high qualification rate and ship on time for complex international infrastructure projects.
To keep operations running smoothly, Morui gives full technical support, from remote debugging to onsite training for operators in the markets we serve. We supply the expertise needed to get the most out of microbial degradation and to extend system life. As a trusted partner in water treatment, Guangdong Morui delivers lasting value through advanced membrane bioreactor solutions.
PVDF Membrane Bioreactor Systems That Scale for Global Water Security
Wastewater Treatment Applications
The membrane bioreactor (MBR) is now a core technology in water management, and picking the right membrane bioreactor supplier can be just as crucial as the treatment process itself. It's especially important when both effluent quality and footprint are hard requirements. Industrial and municipal operators use it mainly for:
- Industrial wastewater reclamation is a real challenge. Textile, food and beverage, and pharmaceutical operations often carry high organic loads. They need intensive biological treatment plus fine filtration from a reliable membrane bioreactor supplier to reuse process water.
- Municipal sewage upgrading. To meet stricter nitrogen and phosphorus removal standards, urban plants replace traditional secondary clarifiers.
- Decentralized treatment systems. These are a good fit for hotels, resorts, and remote residential complexes in areas with limited infrastructure. They provide local water recycling for irrigation.
Regional Challenges and Client Pain Points
Dealing with environmental regulations across South America, Southeast Asia, Europe, the Middle East, and Africa brings unique challenges:
- Compliance is no longer optional. Discharge limits for Chemical Oxygen Demand (COD) and Total Suspended Solids (TSS) keep getting tighter across Europe and the Middle East. Conventional systems can't keep up.
- Hot climates bring real operating headaches. In the Middle East and Africa, high ambient temperatures can throw off biological activity and damage membrane integrity. If left unmanaged, that leads to early fouling.
- Space is tight in crowded Southeast Asian cities, and land doesn't come cheap. The big footprint of a Conventional Activated Sludge (CAS) system just doesn't make economic sense there.
- Maintenance and know-how matter as well. Buyers in regions with few onsite technicians often hesitate because they worry about membrane lifespan and how complex automated cleaning (CIP) can be.
Guangdong Morui Integrated Solution
Guangdong Morui Environmental Technology Co.,Ltd started in 2005. The company builds a modular membrane bioreactor system designed to hold up in different parts of the world. Its MR-MBR-193 module pairs with advanced biological processes for a turnkey approach. Raw wastewater goes in, high-purity permeate comes out. The system meets ISO, CE, and ROHS standards, so it's reliable across many international markets.
System Architecture and Key Components
The solution is built around a multi-stage design for stability and high flux:
- The pre-treatment unit uses fine screens (1-2mm) to catch hair and fibrous debris before they reach the membranes. This protection significantly extends the service life of the PVDF material.
- The MBR membrane module uses the MR-MBR-193 model, with a 22.4m² surface area and a 0.2um micron rating. PVDF gives it strong chemical resistance and mechanical strength.
- An automated control system with a PLC-based interface tracks trans-membrane pressure (TMP) and runs backwash cycles automatically. This keeps permeability at its best.
- The CIP maintenance module includes a built-in Clean-In-Place system. It handles periodic chemical cleaning without taking the module apart, so downtime stays low.
Measurable benefits and advantages of the solution
- Space optimization. The solution cuts facility footprint by 40–60% compared with traditional clarifier-based systems.
- Superior effluent quality. It achieves turbidity below 0.1 NTU and removes pathogens through the 0.2um filtration barrier.
- Enhanced durability. PVDF hollow fiber membranes have high tensile strength, so fibers don't break during high-aeration scouring.
- Energy Efficiency: The optimized aeration design cuts the energy needed for membrane scouring by up to 20%.
Global Implementation and Service Capability
For international projects, Guangdong Morui provides thorough technical consulting and fast spare parts delivery. The service includes remote diagnostics and detailed installation supervision, which helps local teams in South America or Southeast Asia run operations effectively. Operators also get detailed training to reduce the learning curve.
Typical Application Case: Textile Reuse in Southeast Asia
A large textile facility faced rising water costs and strict local discharge limits. After adopting the MR-MBR-193 solution, the plant achieved:
- Suspended solids fell by 95%.
- 70% of treated water is directly reused for non-critical dyeing processes.
- The plant operated stably under high-fouling conditions for over 24 months.
Project Consultation and Technical Support
Detailed technical specifications, CAD drawings, and site-specific flux calculations are available to engineering partners for integrating advanced filtration modules into new or existing wastewater treatment infrastructure.
Complex wastewater streams contain pathogens and suspended solids. High-performance microfiltration membranes act as a robust barrier against both.
FAQs
1. How does a membrane bioreactor improve wastewater treatment quality compared to conventional systems?
A membrane bioreactor (MBR) integrates biological degradation with advanced membrane filtration, effectively replacing the traditional secondary clarifier. By using a semi-permeable barrier—such as the PVDF membranes found in our MR-MBR-193 model—the system physically removes suspended solids, bacteria, and most pathogens. This results in high-purity effluent that meets stringent discharge limits and is often suitable for irrigation or industrial reuse. For facility owners, the primary advantages are a significantly smaller footprint and a more consistent output, even when influent quality fluctuates. Guangdong Morui Environmental Technology Co.,Ltd has specialized in this technology since 2005, ensuring our 0.2um pore size membranes provide a reliable barrier that eliminates issues like sludge bulking. We recommend evaluating your required biochemical oxygen demand (BOD) reduction to determine if the 22.4m2 filtration area per module fits your specific flow requirements.2. What are the key parameters to consider when selecting a membrane bioreactor for industrial applications?
Selecting the right membrane bioreactor requires a balance between flow volume, wastewater characteristics, and available space. Key technical parameters include the flux rate (the volume of water passing through the membrane per unit area), the membrane material, and the micron rating. For instance, our MR-MBR-193 uses PVDF (Polyvinylidene Fluoride), which offers superior chemical resistance and durability compared to standard materials. With a dimension of 1300X1250X30mm and an effective area of 22.4m2, this model is designed for high-density packing in compact tanks. We suggest clients provide their daily peak flow rates and Chemical Oxygen Demand (COD) levels so our engineers can calculate the optimal number of modules. Since every industrial site has unique contaminants, contacting Guangdong Morui Environmental Technology Co.,Ltd for a custom flux analysis is a vital step in ensuring long-term system stability.3. How does the MBR system perform in the high-temperature and high-humidity climates of Southeast Asia or the Middle East?
In regions like Southeast Asia, the Middle East, and parts of Africa, high ambient temperatures can accelerate biological activity but also increase the risk of organic membrane fouling. Our membrane bioreactor modules are engineered using reinforced PVDF, which maintains structural integrity and filtration efficiency at higher operating temperatures. The 0.2um micron rating is specifically calibrated to prevent deep-pore clogging while allowing for efficient backwashing. To maintain performance in these climates, we recommend implementing a robust automated aeration system to keep membranes scoured and preventing sludge accumulation. Additionally, ensuring a stable pH and nutrient balance within the bioreactor is crucial for microbial health. If you are operating in these regions, we advise a routine Maintenance Cleaning (MC) protocol using specific chemical concentrations to preserve the 22.4m2 surface area's permeability. You can consult with our technical team for specific chemical cleaning intervals based on local water hardness.4. What certifications and compliance standards are necessary for importing a membrane bioreactor to Europe or South America?
When importing water treatment technology to markets in Europe, South America, or Southeast Asia, verifying international quality standards is essential for both legal compliance and operational safety. A reputable membrane bioreactor should carry ISO 9001 certification for quality management, alongside CE marking for European safety standards and ROHS compliance for hazardous substance control. Guangdong Morui Environmental Technology Co.,Ltd holds ISO, CE, and ROHS certifications, ensuring our MR-MBR-193 modules meet global benchmarks for environmental protection and mechanical safety. While these certifications cover broad international requirements, importers should confirm specific local environmental regulations, as some regions in Europe may have stricter nitrogen or phosphorus removal mandates. We provide comprehensive documentation and test reports to assist in the local permitting process. We recommend checking with your local environmental agency to see if additional third-party laboratory validations are required for your specific discharge permit.5. Can Guangdong Morui Environmental Technology Co.,Ltd provide technical support and installation guidance for MBR projects in Africa or Southeast Asia?
Yes, supporting international projects in Africa, Southeast Asia, and South America is a core part of our service. Having been established in 2005, Guangdong Morui Environmental Technology Co.,Ltd has nearly two decades of experience in exporting and supporting membrane bioreactor installations globally. For remote projects, we provide detailed technical drawings, installation manuals, and video guidance to ensure the MR-MBR-193 modules are correctly positioned within the bioreactor tanks. While we primarily offer remote commissioning support and technical consultation, on-site assistance can sometimes be coordinated depending on the project scale and location. We emphasize the importance of a correct "clean water test" before introducing activated sludge to the system. For clients with complex influent parameters, we suggest sending a water quality report to our team so we can provide a tailored aeration and trans-membrane pressure (TMP) monitoring strategy to maximize the lifespan of your PVDF membranes.
Best Selling Products
Related Blogs
Related Search
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.