



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
1000LPH EDI equipment supplier
Reliable 1000LPH EDI Equipment for Global Industrial Ultrapure Water
When procurement managers across South America, Southeast Asia, Europe, the Middle East, and Africa are looking for reliable 1000LPH EDI equipment, they begin with one question: how deep does the 1000LPH EDI equipment supplier's technical know-how go, and what does its manufacturing record look like? Get that call wrong, and stable operations are at risk. EDI, or electrodeionization, is a later, more advanced step in water treatment. It combines ion-exchange resins, selective membranes, and a DC electrical field to keep water deionizing. Industries that need high-purity water depend on it, because it eliminates the logistics and safety headaches that come with chemical regeneration of resin.
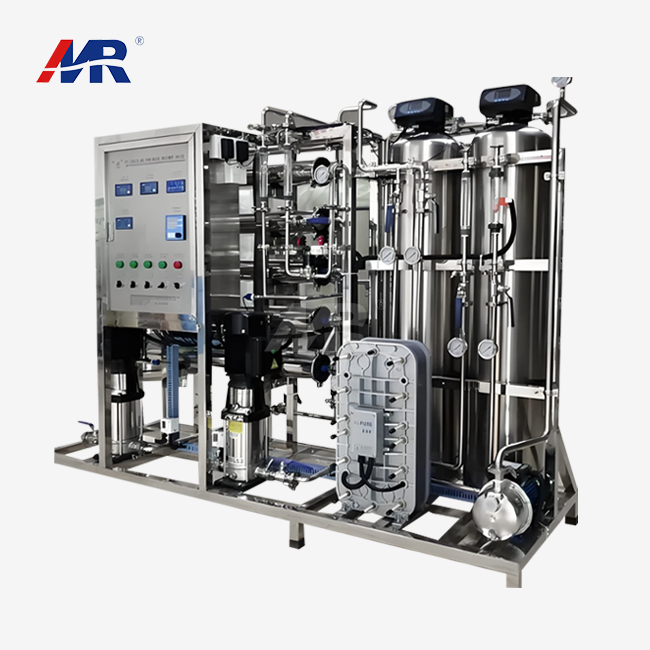
Industrial plants across Southeast Asia and Africa often deal with high running costs, and they also carry the environmental burden of getting rid of hazardous waste. Older ion exchange systems have to shut down often for acid and caustic cleaning. That pushes costs up and raises environmental compliance risks. Competition only makes things tougher. In Europe and South America, high-tech manufacturing cannot run without steady water resistivity of up to 18.2 MΩ·cm. For buyers everywhere, the main challenges come down to three points: finding a 1000LPH EDI equipment supplier that can handle local power fluctuations, meets strict CE and ISO certifications, and keeps total cost of ownership low through energy efficiency.
Guangdong Morui Environmental Technology Co.,Ltd was set up in 2005 and answers this demand with precision-engineered water treatment systems. Its focus is robust 1000LPH EDI equipment built to slot into complex industrial workflows. The Model: MR-EDI-1TH was developed for ultrapure water production, with long-term membrane integrity and steady salt rejection as the priorities. Morui works to ISO, CE, and ROHS standards, which gives procurement professionals the technical assurance they need that their water treatment infrastructure clears both local regulations and global quality benchmarks.
- High-Precision Salt Rejection: The Model: MR-EDI-1TH reaches a salt rejection rate of 99.99%, so critical water treatment applications get the highest possible purity.
- Low energy use: This 1000LPH EDI unit is built to run efficiently. It draws just 4kw per hour. That sharply lowers utility costs and carbon footprint for facilities across the Middle East and Africa.
- Certified quality standards: Morui is an established manufacturer of 1000LPH EDI equipment. Each unit meets ISO, CE, and ROHS certifications, so it can slot into industrial zones in Europe and South America.
- Sustainable water recovery: The system holds a 55% recovery rate. That balance draws as much ultrapure water from the process as possible while keeping wastewater discharge as low as possible.
- The electrochemical regeneration process is chemical-free and runs 24/7. Workers don't have to handle any hazardous chemicals. That improves workplace safety and helps meet modern environmental ESG goals.
Verifying technical specifications and reviewing performance certifications allows engineering teams to confirm the compatibility of the MR-EDI-1TH with specific site conditions. Detailed analysis of energy consumption data and salt rejection benchmarks provides a clear trajectory for calculating long-term return on investment. The availability of comprehensive technical documentation assists in the validation of system performance for high-stakes industrial ultrapure water applications.
Related Products




About Guangdong Morui Environmental Technology Co., Ltd
Guangdong Morui Environmental Technology Co., Ltd was founded back in 2005. We make high-performance industrial water treatment systems, and we've grown into one of the leading manufacturers in the field. After nearly two decades of technical work, we now focus on 1000LPH EDI equipment, and as a 1000LPH EDI equipment supplier we serve demanding industries in South America, Southeast Asia, Europe, the Middle East, and Africa.
Our core strength is stable, chemical-free ultrapure water, and we deliver it with the MR-EDI-1TH model. Built for high-precision applications, this system from a 1000LPH EDI equipment supplier reaches a 99.99% salt rejection rate. With no resin regeneration, you get no downtime and none of the hazards that come with it. We've spent years working through the regulatory landscapes of Europe and Southeast Asia, so our systems meet strict local standards for high-resistivity water.
Quality and compliance sit at the center of how we operate. Morui is ISO-certified, and our 1000LPH EDI equipment holds CE and ROHS certifications, a reflection of how we meet international safety and environmental standards. Energy consumption is focused at 4kw/hour, so the systems are optimized for performance and for operational economy.
We support our global partners for the long term with full technical service, including remote debugging and on-site training. Morui Environmental Technology is committed to sustainable, high-purity water systems that drive your industrial growth.

Sustainable Ultrapure Water Solutions for Global Industrial Standards
Application Scenarios
If you run a water treatment facility and need a steady supply of chemical-free ultrapure water, 1000LPH EDI equipment is a dependable pick, and a 1000LPH EDI equipment supplier can help you keep that supply consistent. Common applications:
- Pharmaceutical Production: We meet USP/EP standards for purified water used in reagent prep and equipment rinsing, working with a trusted 1000LPH EDI equipment supplier to keep that quality consistent.
- Semiconductor Fabrication: Supplies the low-conductivity water needed to clean wafers. Even trace ions cause manufacturing defects.
- Power Generation: Supplies high-pressure boiler feed water. This prevents scale buildup and protects turbine integrity in thermal plants.
Regional Obstacles and Customer Pain Points
Industrial operators in South America, Southeast Asia, Europe, the Middle East, and Africa run into major operational problems that traditional systems can't solve:
- Environmental Regulations: Markets in Europe and Southeast Asia are increasingly limiting the release of hazardous chemical waste (acids and caustics) from traditional resin regeneration.
- Logistical Complexity: In remote parts of Africa and South America, the high cost and safety risks of moving and storing bulk chemicals for water treatment put constant strain on operations.
- Resource Management: High energy costs in the Middle East and global water scarcity make the 55% recovery rate and 4kw/hour energy consumption of the MR-EDI-1TH critical for controlling total cost of ownership.
- Quality Instability: Traditional ion exchange beds let resistivity drift as the resin exhausts. That drift can contaminate a batch and take the line down without warning.
The Morui 1000LPH EDI Integrated Solution
Guangdong Morui Environmental Technology Co.,Ltd takes a complete, modular approach built around the MR-EDI-1TH model. This unit combines electrodialysis and conventional ion exchange into one electrochemical process. Chemical regeneration is no longer needed, and the salt rejection rate stays at 99.99%. It is built as a turnkey engineering package that fits straight into existing RO (Reverse Osmosis) permeate lines.
System Architecture and Key Components
- Pre-Treatment and RO Barrier: A multi-stage filtration unit pulls out suspended solids and organics. A primary Reverse Osmosis stage then follows to lower the bulk ion load.
- MR-EDI-1TH Core Module: In the 1000LPH EDI stack, ion-selective membranes pair with a DC electrical field. Together they keep pushing ions out of the feed stream, and power use holds steady at 4kw/hour.
- PLC Automation Suite: Industrial controllers (PLC) and real-time resistivity sensors come built in. The system adjusts voltage on its own to hold water quality steady, even when the feed shifts.
- Cleaning-In-Place (CIP) Module: Built-in maintenance valves let you sanitize the stack on a schedule without taking it apart. That keeps membranes healthy over the long run, even in high-temperature or high-fouling conditions.
Quantifiable System Advantages
- Consistent High Purity: Salt rejection reaches 99.99%. Output stays stable and high in resistivity.
- Operational Efficiency: It draws just 4kw/hour, so energy costs can fall by as much as 30% compared with older electrochemical designs.
- Reduced Footprint: The modular skid-mounted design can save up to 50% of floor space that bulky chemical regeneration tanks would otherwise take up.
- Zero Chemical Hazards: No more buying, storing, or disposing of hazardous acids and caustics, which removes those costs entirely.
- Certified Reliability: It fully complies with ISO, CE, and ROHS standards, giving you international quality verification.
Global Implementation and Service Capability
Specialized engineering teams have backed deployments on five continents since 2005. For clients in the Middle East and Africa, remote diagnostics allow real-time troubleshooting. A strong global supply chain also delivers replacement membranes and spare parts fast, which keeps downtime to a minimum.
Typical Application Case Study
A pharmaceutical plant in Southeast Asia faced frequent downtime. Its traditional deionization beds also created hazardous waste disposal problems. After installing the 1000LPH MR-EDI-1TH solution, the plant got a continuous supply of ultrapure water with a 99.99% salt rejection rate. The switch cut annual maintenance costs by 40% and removed the need for chemical handling. It also brought the plant fully in line with local environmental sustainability mandates.
Technical Analysis and Verification
Comprehensive technical documentation and site-specific engineering drawings assist in verifying performance metrics against regional water chemistry profiles. Detailed validation reports for ISO and CE audits provide the necessary transparency for high-stakes industrial procurement and regulatory compliance. Continuous electrodeionization modules deliver stable high-resistivity output through automated electrochemical resin regeneration technology.
FAQs
1. What are the primary advantages of using 1000LPH EDI equipment compared to traditional ion exchange?
The 1000LPH EDI equipment, specifically our MR-EDI-1TH model, offers a continuous, chemical-free process for ultrapure water production. Unlike traditional Ion Exchange (IX) which requires hazardous acid and caustic chemicals for resin regeneration, Electrodeionization (EDI) utilizes electricity, ion-selective membranes, and resin to remove ions. This eliminates downtime associated with regeneration cycles and removes the need for chemical storage and neutralization systems. For facilities requiring a steady flow of 1,000 liters per hour, this technology ensures stable water quality with a salt rejection rate of 99.99%. By switching to an EDI system, industrial users significantly reduce their environmental footprint and operational risks. If you are looking to modernize your water treatment line, Guangdong Morui can provide detailed comparative data based on your current chemical consumption.2. How do I determine if the 1000LPH EDI equipment is the right fit for my industrial ultrapure water needs?
Selecting the right 1000LPH EDI equipment involves evaluating your required flow rate, energy efficiency, and output resistivity. The MR-EDI-1TH is designed for high-demand applications, consuming approximately 4kw per hour while maintaining a recovery rate of 55%. When choosing a system, you should first ensure your pre-treatment—typically a Double Pass Reverse Osmosis system—is capable of providing high-quality permeate, as EDI modules are sensitive to hardness and CO2 levels. You should also consider the "total cost of ownership," which includes membrane longevity and power stability. With over 19 years of experience since 2005, Guangdong Morui Environmental Technology Co.,Ltd recommends checking the salt rejection rates; our systems achieve 99.99% rejection, ensuring the highest purity for electronics or pharmaceutical applications. Feel free to share your raw water analysis for a customized configuration.3. Does the 1000LPH EDI equipment from Guangdong Morui meet international standards for the European and Middle Eastern markets?
Yes, our 1000LPH EDI equipment is engineered to meet stringent international quality and safety standards, making it highly suitable for export to Europe, the Middle East, and beyond. Guangdong Morui has been an ISO-certified manufacturer since 2005, and our products carry CE and ROHS certifications, ensuring compliance with European safety and environmental directives. In the Middle East, where water conservation and durability are paramount, our systems are built to withstand demanding industrial environments. While our equipment meets these global benchmarks, we always advise clients to verify local grid requirements and specific regional environmental regulations regarding wastewater discharge. Our technical team can provide the necessary documentation and certifications to streamline your local compliance and import processes.4. How does the 1000LPH EDI equipment perform in regions with challenging water conditions, such as Southeast Asia or Africa?
In regions like Southeast Asia or Africa, where source water may have high salinity or varying mineral content, the performance of 1000LPH EDI equipment relies heavily on effective pre-treatment. Since EDI is the final polishing stage, it requires the feed water to be pre-processed by Reverse Osmosis (RO) to remove the bulk of dissolved solids. Our MR-EDI-1TH model is designed to handle the permeate from these systems, delivering a 99.99% salt rejection rate to produce ultrapure water. To prevent scaling or fouling in tropical or arid climates, we recommend implementing robust filtration and softening stages before the EDI unit. Guangdong Morui provides specialized guidance on integrating RO-EDI systems to ensure the 55% recovery rate remains consistent even in difficult environments. We suggest contacting us for a specific pre-treatment design tailored to your local water characteristics.5. What technical support and installation services are available for projects in South America or Africa?
Guangdong Morui Environmental Technology Co.,Ltd provides comprehensive technical support for our 1000LPH EDI equipment across South America, Africa, and other global markets. Recognizing the geographical distance, we offer a multi-tiered support system that includes detailed installation manuals, video commissioning guides, and 24/7 remote technical assistance. For large-scale industrial projects, we can coordinate on-site technical supervision or work closely with local engineering partners to ensure the MR-EDI-1TH is integrated correctly into your facility. Our 4kw/hour low-power design is particularly beneficial for regions with high energy costs. Since 2005, we have successfully exported water treatment solutions worldwide, and we maintain a ready stock of essential components to ensure long-term reliability. We encourage international buyers to discuss their specific logistics and local service requirements with our export department.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.