



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
industrial sewage treatment plant supplier
Industrial Sewage Treatment Plants Built for High Performance and Global Compliance
Picture yourself as a procurement manager hunting for a reliable industrial sewage treatment plant in South America, Southeast Asia, Europe, the Middle East, or Africa. You want an industrial sewage treatment plant supplier with real technical depth. That decision will shape how the plant runs for years. A treatment plant is critical infrastructure. It breaks down tough pollutants, heavy metals and high-strength organic loads among them, before the effluent leaves the site or gets reused. These systems keep a facility inside environmental rules. They also shield local ecosystems from the hazardous byproducts of manufacturing.
Operators in many regions hit serious trouble when they buy wastewater equipment. In Europe and South America, strict rules mean effluent quality has to be precise. Over in Southeast Asia and Africa, plants often face high energy costs and struggle to find specialized maintenance teams nearby. Wastewater from chemical or pharmaceutical processes is tougher to treat. It calls for a system that rides out fluctuating pollution loads without constant membrane fouling or a biological system failure. And picking an industrial sewage treatment plant supplier isn't easy either, as long lead times and weak documentation for ISO or CE compliance often stall projects. Operational risk climbs, and the owner can end up facing environmental penalties.
Guangdong Morui Environmental Technology Co.,Ltd has been in business since 2005. The company engineers sturdy industrial sewage treatment plant solutions for demanding environments worldwide. Nearly two decades of expertise go into serving what procurement teams actually need. Morui supplies fully certified systems that narrow the gap between regulatory compliance and cost-efficiency. Its engineering pairs advanced biological processes with high-end filtration. That keeps water reclamation stable even when loads run high.
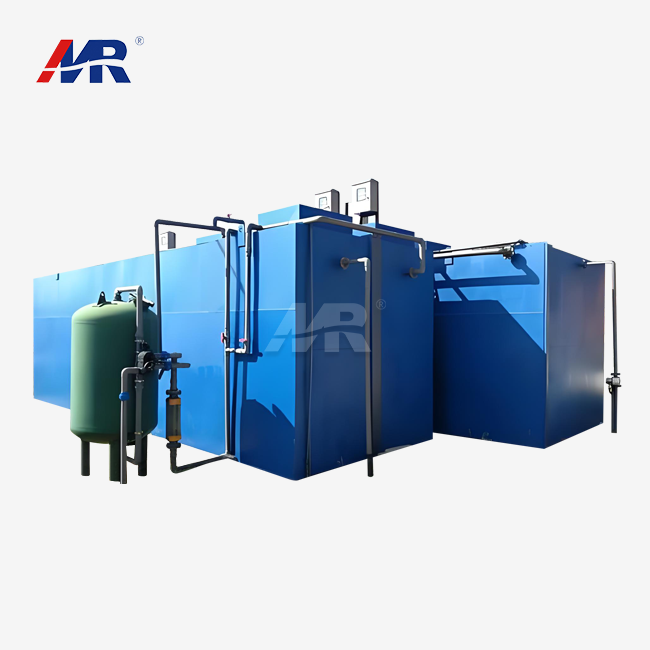
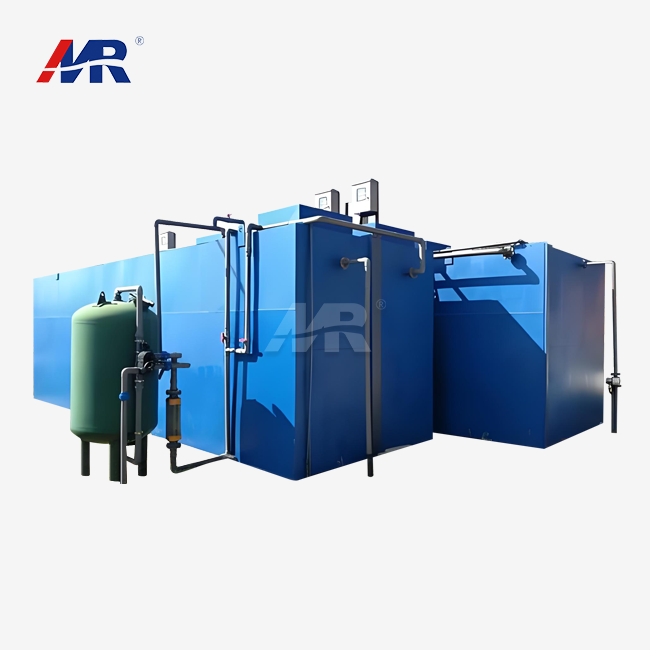
The MR-MBR-10TH is a good example of what this technical capability looks like in practice. It runs an AAO+MBR flow process, which removes nitrogen and phosphorus at high rates. This industrial sewage treatment plant is built for 200m³/day. Its 12x2x2.4-meter footprint is compact, so it works well on tight sites. Morui is a direct manufacturer of industrial sewage treatment plants. Every unit meets ISO, CE, and ROHS standards, so it lasts and is easy to maintain. A professional technical team can also help with remote selection and site-specific configuration.
- Advanced AAO+MBR Process: Anaerobic-Anoxic-Oxic and Membrane Bioreactor technology work together here. The result is high-quality effluent you can reuse in many industrial wastewater treatment applications.
- Global Compliance and Quality Assurance: Every system is made to ISO, CE, and ROHS standards. That helps it move through customs more easily and gain regulatory approval in Europe and South America.
- Optimized Space Efficiency: The system fits a 12x2x2.4-meter footprint but still handles a high treatment capacity of 200m³/day. Civil engineering needs stay low.
- Proven in the region: These plants have a track record in the Middle East and Southeast Asia going back to 2005. They are built to handle the wide range of climates and operating conditions found there.
- Manufacturer credibility you can verify: The company is an established industrial sewage treatment plant manufacturer. It provides complete technical documentation and performance data to support procurement decisions.
To further evaluate how the MR-MBR-10TH can integrate into an existing facility, procurement professionals can obtain comprehensive technical specifications or a case study portfolio from the engineering department. Technical specialists are available to discuss specific influent parameters and provide a detailed quotation aligned with international shipping and installation requirements. Establishing a technical dialogue ensures that the selected configuration addresses both current discharge limits and future expansion needs.
The implementation of modular membrane technology ensures consistent effluent quality and reduced sludge production in modern manufacturing environments.
Related Products




About Guangdong Morui Environmental Technology Co., Ltd.
Founded in 2005, Guangdong Morui Environmental Technology Co., Ltd. is a leading maker of high-performance systems for industrial sewage treatment. We've spent almost two decades in the water treatment industry worldwide, and that work has earned us a strong name as an industrial sewage treatment plant supplier for reliable systems in South America, Southeast Asia, Europe, the Middle East, and Africa.
We design systems that handle complex industrial wastewater, including flows from petrochemical, pharmaceutical, and textile operations. Our systems are built to neutralize high-strength organic loads and hazardous chemicals, and as an industrial sewage treatment plant supplier, we make sure they meet strict environmental regulations. The MR-MBR-10TH model is a good example of what we can do. This 200m³/day plant uses an advanced AAO+MBR process to reach high effluent reclamation and Zero Liquid Discharge (ZLD) targets.
Quality and reliability come first in our operations. Morui is ISO, CE, and ROHS certified and follows strict quality management standards. We support our international clients with a full range of technical services. These range from remote commissioning and onsite training to long-term maintenance support. The result is stable operations in different geographic environments.
Guangdong Morui is here to be your long-term partner in sustainable wastewater management. Solid engineering and worldwide service work together to keep your industrial sewage treatment plant delivering steady, high-quality results.

Industrial Sewage Treatment Plants for Reliable Global Sustainability
Application Overview
For modern manufacturers, an industrial sewage treatment plant is essential infrastructure. It keeps production running and helps protect the environment. For industries that produce high-load wastewater as a byproduct, Guangdong Morui Environmental Technology Co.,Ltd serves as an industrial sewage treatment plant supplier with specialized systems. Textile and dyeing is one common use: complex dyes and high salinity need to be neutralized. Drug manufacturing requires breaking down active ingredients and solvents. Petrochemical plants focus on separating oils and phenolic compounds to protect local ecosystems.
Customer Challenges and Pain Points
Factories across South America, Southeast Asia, Europe, the Middle East, and Africa run into different problems, yet the rules are every bit as strict. In Europe, meeting REACH and the Water Framework Directives comes down to high-precision filtration, which often means relying on a industrial sewage treatment plant supplier that understands the regulations. In Southeast Asia and Africa, high energy costs and a shortage of skilled workers often make it tough to keep complex systems running. Companies that fail to meet these standards face heavy discharge fees, legal risks, and environmental harm. In dry regions such as the Middle East, a lack of process water turns Zero Liquid Discharge (ZLD) into a financial necessity, not just a regulatory hurdle.
Guangdong Morui Industrial Sewage Treatment Solution
Guangdong Morui Environmental Technology Co.,Ltd has been building integrated, modular systems since 2005. They help connect complex industrial waste with environmental safety. Our main focus is the AAO+MBR process (Anaerobic-Anoxic-Oxic + Membrane Bioreactor). It provides strong biological treatment in a small footprint. We deliver these systems as turnkey packages, so setup is fast and onsite civil work is minimal. That matters for international projects in remote locations or places with limited space.
System Architecture and Key Components
The MR-MBR-10TH is the top model in our modular lineup. It has a 12X2X2.4-meter footprint and can process 200m³/day.
- Pre-treatment Unit: Advanced screening and equalization hold the influent pH steady and take out solids. This protects the biological units downstream from shock loads.
- AAO Biological Unit: The process moves through three stages: anaerobic, anoxic, and oxic. It targets high nitrogen and phosphorus removal, and it takes on heavy organic loads (BOD/COD) well.
- MBR Membrane Module: A high-flux membrane replaces traditional secondary clarifiers. The result is cleaner effluent, and it often exceeds international discharge standards for reuse.
- Automated Control System: PLC and SCADA modules come built in. They let you watch the process live and run diagnostics from a distance. Operators no longer need to stay on site at all times.
Solution Advantages and Quantifiable Benefits
- Footprint Efficiency: Set against traditional activated sludge systems, the MR-MBR-10TH cuts land use by as much as 50%.
- Superior Water Quality: The effluent is clean enough for irrigation. It also works as cooling tower makeup water.
- Lower labor costs: With full automation and CIP (Clean-In-Place), there is almost no manual cleaning.
- Energy savings: Daily power consumption drops by around 15-20% thanks to better aeration protocols.
- Global Compliance: Every system we build meets ISO, CE, and ROHS standards. That means regulators around the world accept them.
Implementation and Global Service Capability
Guangdong Morui Environmental Technology Co.,Ltd supports international clients through every stage of service, from the first water quality analysis to final commissioning. Our logistics network delivers modular units safely to South America, Europe, and other regions. Remote technical support is available, along with standard spare parts kits that ship in short lead times, so downtime stays at zero. Onsite operators get localized training, and that gives them the confidence to run the system.
Typical Application Scenario
A textile plant in Southeast Asia faced rising fines for its discharge because of high colority and COD levels. After installing the MR-MBR-10TH solution, the plant cut suspended solids by 98% and achieved significant decolorization. The modular 200m³/day system let the factory reuse 60% of its wastewater for secondary processes. That lowered water purchasing costs and helped it meet all local environmental mandates within three months of installation.
Industrial operators around the world use technical documentation and customized engineering specifications to stay compliant with environmental rules and keep operations efficient over the long term.
FAQs
1. What are the key factors to consider when selecting an industrial sewage treatment plant for a new manufacturing facility?
Selecting the right industrial sewage treatment plant requires a comprehensive analysis of your daily wastewater volume and the specific chemical composition of the influent. At Guangdong Morui Environmental Technology Co.,Ltd, we recommend three primary steps: first, conduct a professional water quality test to identify levels of COD, BOD, and heavy metals; second, define your discharge goals, whether they involve local municipal sewer standards or Zero Liquid Discharge (ZLD) for environmental reuse; and third, evaluate the available footprint at your site. For instance, our MR-MBR-10TH model utilizes a compact 12X2X2.4 meter design, making it ideal for facilities with limited space. Since our establishment in 2005, we have found that choosing a system with high-quality components and recognized certifications like ISO and CE is essential for long-term operational stability and regulatory compliance.2. Why is the AAO+MBR process preferred for modern industrial wastewater treatment systems?
The AAO (Anaerobic-Anoxic-Oxic) combined with MBR (Membrane Bioreactor) process is widely regarded as a gold standard for an industrial sewage treatment plant because it offers superior effluent clarity and a smaller physical footprint. The AAO stages are specifically designed to remove nitrogen and phosphorus through biological degradation, while the MBR serves as a high-precision filtration barrier that replaces traditional secondary sedimentation tanks. This combination, found in our MR-MBR-10TH system, ensures that even complex industrial effluents are treated to a level suitable for recycling or safe environmental discharge. With a capacity of 200m3/day, this technology effectively handles high-strength organic loads and provides a consistent water output that meets stringent international standards. If you are dealing with fluctuating pollutant concentrations, we suggest contacting our technical team to discuss how this process can be customized for your specific flow requirements.3. How does Guangdong Morui support the installation and maintenance of an industrial sewage treatment plant in regions like Southeast Asia, the Middle East, or Africa?
For international projects in the Middle East, Southeast Asia, and Africa, Guangdong Morui Environmental Technology Co.,Ltd provides comprehensive technical support to ensure the long-term reliability of your industrial sewage treatment plant. Our MR-MBR-10TH units are often pre-assembled and skid-mounted within standard dimensions (12X2X2.4m) to simplify shipping and onsite setup. We provide detailed installation manuals, video guidance, and remote technical debugging to assist local engineering teams. Given the high-temperature environments often found in these regions, we utilize durable materials and components that meet CE and ROHS standards to prevent premature wear. We recommend establishing a routine maintenance schedule—such as monthly membrane cleaning and sensor calibration—to optimize performance. For large-scale projects, we can also coordinate specialized onsite commissioning to ensure the system is tuned to the specific environmental conditions of your region.4. What certifications and compliance standards should an industrial sewage treatment plant meet for export to Europe and South America?
When exporting an industrial sewage treatment plant to demanding markets like Europe or South America, adherence to international quality and safety standards is non-negotiable. Typically, systems must carry CE marking for the European market to demonstrate compliance with health, safety, and environmental protection standards. ISO 9001 certification is also critical as it verifies the manufacturer’s quality management consistency. Furthermore, ROHS compliance ensures that the components used in the plant do not contain hazardous substances. While these certifications provide a baseline for equipment safety, discharge limits are often governed by local environmental agencies. We advise clients to verify specific regional parameters for COD and TDS (Total Dissolved Solids), as these may vary significantly between countries. Guangdong Morui has been navigating these international regulatory landscapes since 2005, ensuring our solutions are built to satisfy both global and local requirements.5. Can a standard industrial sewage treatment plant handle complex wastewater from the textile or pharmaceutical industries?
Standard systems often struggle with the complex synthetic dyes or active pharmaceutical ingredients (APIs) found in these industries. However, a specialized industrial sewage treatment plant like the MR-MBR-10TH can be optimized for these challenges. In textile applications, we often integrate advanced oxidation or decolorization steps before the MBR process to tackle high salinity and stubborn colorants. For pharmaceutical manufacturing, the biological degradation phase is tuned to neutralize solvent residues. To ensure the 200m3/day capacity is utilized effectively, we recommend a pilot test or a detailed analysis of your raw wastewater. By adjusting the AAO+MBR parameters, Guangdong Morui can help your facility achieve high-quality effluent reclamation, reducing your environmental footprint and avoiding high discharge levies. Please provide your specific water quality parameters so we can provide a tailored technical proposal for your project.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.