



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
ro membrane supplier
High-Performance RO Membrane Solutions for Water Treatment Worldwide
Procurement managers and engineers oversee water treatment projects in South America, Southeast Asia, Europe, the Middle East, and Africa. For them, finding a dependable ro membrane supplier matters because a reliable RO membrane is the foundation of a system's longevity. It is the core functional component in reverse osmosis systems. The membrane acts as a molecular sieve. Its semi-permeable polyamide layer can remove up to 99% of dissolved solids. That gives high-purity water for industrial, agricultural, and municipal use.
Water treatment facilities all over the world hit local snags. Coastal areas in the Middle East often deal with high salinity. In Southeast Asia, feedwater turbidity can swing constantly. A common pain point is rapid membrane fouling. It causes too much chemical cleaning and shortens element lifecycles. Energy is another one. Keeping permeate flux steady under high pressure costs a lot, and a ro membrane supplier that gets it wrong can strain the operational budget. Procurement teams also have a hard time checking whether performance data is real. They also need to ensure compliance with international environmental standards like CE and ROHS. That becomes especially tough when remote project sites bring logistics challenges.
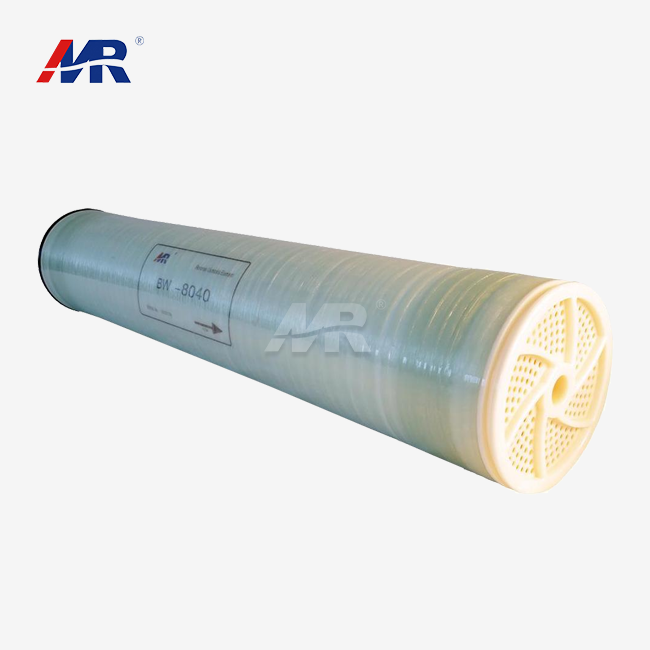
Guangdong Morui Environmental Technology Co., Ltd was established in 2005. The company meets these challenges with RO membrane solutions made for high-fouling and high-salinity conditions. As a veteran RO membrane manufacturer, it focuses on balancing permeate quality with energy efficiency. Our Model MR-BW-4040 is built for brackish water applications and offers a robust 99.5% salt rejection rate. These elements are made under ISO-certified manufacturing protocols, so they give the consistency that large-scale desalination and industrial process water systems need in markets around the world.
These high-performance elements deliver a few clear benefits:
- Exceptional salt rejection. The 99.5% rejection rate removes both monovalent and divalent ions. That meets the strict purity demands of the power and pharmaceutical sectors.
- Optimized flux for industrial capacity. Each element has an effective membrane area of 7.2m² and produces a flow of 2500 GPD. This allows compact system footprints without losing total output.
- Lower operating pressure. The MR-BW-4040 runs at a standard 1.55Mpa. That reduces the energy demand on high-pressure pumps and directly lowers kilowatt-hour consumption per cubic meter of water produced.
- Global Certification Compliance: Full ISO, CE, and ROHS documentation comes with every order. That paperwork helps contractors clear regulatory approval in Europe and South America, and it keeps their supply chain simple.
- Spiral-Wound Mechanical Durability: The multi-layer build resists physical compaction well. Performance stays steady through the temperature swings you see in Africa and the Middle East.
Technical teams and procurement specialists are encouraged to submit their specific feedwater analysis to receive tailored performance simulations and customized scaling projections. Professional support is available to assist in the selection of appropriate spacers and configurations to maximize the efficiency of existing water treatment infrastructures.
The integration of advanced thin-film composite technology ensures long-term chemical stability and consistent permeate quality across varying feedwater conditions.
Related Products




Guangdong Morui Environmental Technology Co., Ltd.: A Leading RO Membrane Manufacturer
Guangdong Morui Environmental Technology Co., Ltd., founded in 2005, has grown into a premier manufacturer. Our work centers on research and, as a ro membrane supplier, on producing high-performance RO membrane solutions. Nearly two decades in water treatment have taken us across South America, Southeast Asia, Europe, the Middle East, and Africa. Large industrial water projects rely on us as a dependable partner.
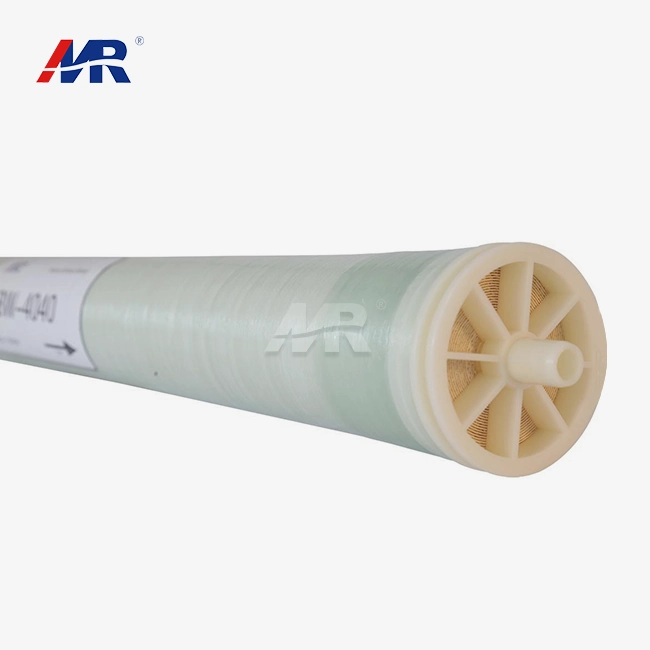
Take the MR-BW-4040. Products like this one really show what we can do, and as a ro membrane supplier, we make sure every unit is built to handle tough conditions. These high-precision membranes use a multi-layered spiral-wound structure with a 7.2m² effective area. At 1.55Mpa operating pressure, they deliver a 99.5% salt rejection rate and a flow of 2500 GPD. So they're a good fit for demanding applications like industrial boiler feedwater and seawater desalination. In those settings, mechanical pressure resistance and low fouling tendencies are critical to stable operations.
We adhere to ISO, CE, and ROHS standards. Our production facility runs rigorous tests on thin-film polyamide layers to keep quality consistent. Across our product range, we maintain high mechanical durability and pH stability. Every RO membrane then meets the strict purity requirements of the pharmaceutical and semiconductor sectors.
We support our international customers with local technical help. That includes remote commissioning and maintenance training, so our systems fit smoothly into the water treatment setups you already have. Guangdong Morui is committed to long-term value. We deliver it through strong technical work and dependable service worldwide. You can count on us as a trusted source for advanced filtration technology.

Innovative RO Membrane Technologies for Sustainable Global Water Security
I. Application Overview
In water treatment today, Reverse Osmosis (RO) membranes serve as the key barrier for filtration at the molecular level. High-performance RO membrane solutions, sourced from your ro membrane supplier, are crucial in industrial boiler feedwater systems to stop scaling, in large-scale seawater desalination (SWRO) for municipal supplies, and in ultrapure water production for the pharmaceutical and semiconductor sectors. These roles call for steady permeate flux. They also need membranes that can handle changes in feed water quality while still meeting strict purity standards.
II. Customer Problems and Challenges
Operators in South America, Southeast Asia, Europe, the Middle East, and Africa face hurdles that vary by location and regulation, and the ro membrane supplier they work with can add another layer:
- High Salinity and Fouling: In the Middle East and Southeast Asia, high TDS (Total Dissolved Solids) and organic biofouling sharply shorten membrane life and increase energy use.
- Strict Regulatory Compliance: Markets in Europe and South America expect strict compliance with ISO, CE, and ROHS standards. That keeps water treatment components environmentally safe and free of heavy metals.
- Operational Costs and Downtime: Remote sites in Africa and parts of South America face high maintenance costs. Membranes that resist mechanical pressure poorly need frequent replacement, and that can bring a system down completely.
III. Guangdong Morui Environmental Technology Co.,Ltd Solutions
Guangdong Morui Environmental Technology Co.,Ltd was founded in 2005. We supply integrated, modular RO membrane solutions built to solve these problems around the world. We do more than sell parts. We deliver optimized membrane arrays that focus on energy efficiency and long-term chemical stability, and we back them with nearly two decades of technical know-how.
IV. System Architecture & Key Components
Our comprehensive solution is centered around high-stability membrane modules and intelligent control systems:
- RO Main Membrane Array: The MR-BW-4040 model uses a multi-layered spiral-wound structure with a thin polyamide selective layer. Its 7.2m² active area is made for brackish water applications that need high throughput.
- Pre-treatment Unit: multi-media filtration that pulls down the Silt Density Index (SDI). This keeps the primary membrane from fouling too early.
- Automated Control System: built-in PLC/SCADA interfaces track the 1.55Mpa operating pressure live, so flow rates stay at their best.
- CIP (Clean-in-Place) Module: a separate unit for maintenance. It runs pH-stable protocols (pH 2-11) to bring membrane performance back, with no need to take anything apart.
V. Solution Advantages & Quantifiable Benefits
- Superior Rejection: Rejects 99.5% of salt, so the permeate stays high-purity for sensitive industrial processes.
- High Productivity: Each element delivers 2500 GPD. That flow rate helps keep system footprints smaller while still meeting high volume demands.
- Energy Efficiency: Built for 1.55Mpa operating pressure. This cuts electricity use by up to 15% compared with standard high-pressure membranes.
- Global Certification: Full compliance with ISO, CE, and ROHS. That makes it easy to integrate into regulated international markets.
- Durability: The tough polysulfone support layer resists mechanical stress from pressure surges.
VI. Implementation Process & Service Ability
We start with a detailed water chemistry analysis. Then we move to custom array configuration and professional onsite commissioning. For clients in Southeast Asia, the Middle East, and beyond, we offer local technical support and an efficient spare parts supply chain. Remote diagnostics let our engineers troubleshoot in real time. That greatly reduces the risk of unplanned downtime in critical infrastructure.
VII. Typical Application Case
A textile plant in Southeast Asia had high conductivity in its process water. That hurt dye quality. The plant installed a multi-stage system with the MR-BW-4040 RO membrane and achieved:
- 99.5% reduction in feedwater salinity.
- Stable 2500 GPD flow per module despite high ambient temperatures.
- Compliance with local environmental discharge regulations through improved water recovery.
- A 20% extension in the interval between chemical cleanings.
VIII. Technical Consultation
Detailed engineering specifications and performance projections are available upon the submission of specific raw water quality parameters. Technical teams provide customized flux calculations and energy recovery evaluations to ensure the most cost-effective configuration for site-specific requirements. The integrated spiral-wound architecture ensures long-term operational stability and superior permeate quality across diverse global environments.
FAQs
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.