
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
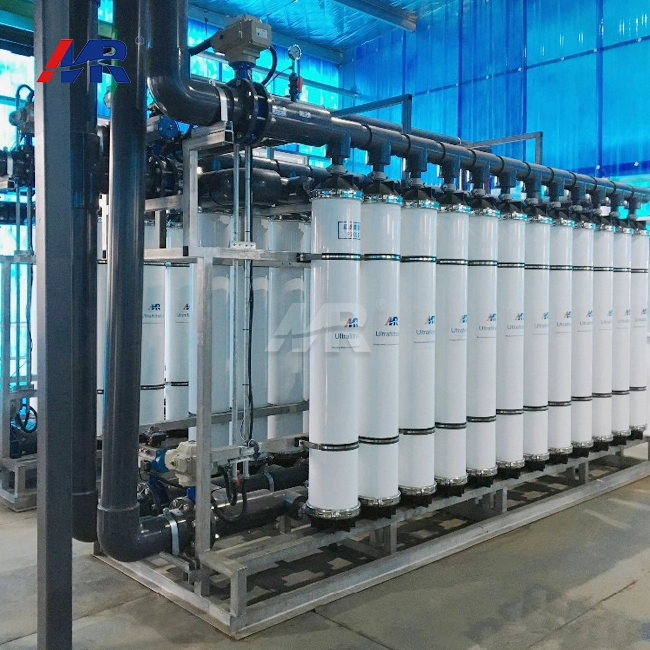
200m3/hour ultrafiltration equipment supplier
High-Performance 200m3/hour Ultrafiltration Equipment for Industrial Applications
Finding a trusted source for 200m3/hour ultrafiltration equipment supplier is important for buying managers in charge of big water treatment projects in South America, Southeast Asia, Europe, the Middle East, and Africa to keep operations running smoothly. Ultrafiltration is a complex membrane process that blocks bacteria, suspended solids, and high-molecular-weight organics. When treating industrial wastewater, this big piece of equipment makes sure that large amounts of process water are properly cleared. This protects systems further down the line and meets strict environmental release standards.

When putting in large-scale filtering systems, industrial sites in places like Southeast Asia and Africa often face big problems. Local rules are very strict and require uniform wastewater quality, which is hard to do when the features of the feed water change. Also, high operational costs caused by machinery that uses a lot of energy and membrane replacements that happen all the time put a huge strain on profit margins. In industrial zones that are far away and don't have quick access to expert help, system instability can cause costly downtime. So, one of the main goals of technical teams is to find 200m3/hour ultrafiltration equipment that works well with high flux and uses little energy.
Guangdong Morui Environmental Technology Co., Ltd. was founded in 2005 and is an expert in designing strong water treatment systems that work in harsh environments around the world. Heavy-duty wastewater recycling is hard to do, but the MR-UF-200TH type is made to handle it. This company that makes 200m3/hour ultrafiltration equipment uses modern hollow fiber membranes with a 0.02um micron grade to create a constant physical barrier that guaranties high-quality permeate. Morui makes sure that all of its systems meet foreign safety and quality standards by getting ISO, CE, and ROHS certificates. This makes it easier for projects in Europe and South America to work together and follow the rules.
- Industrial Wastewater Optimization: The MR-UF-200TH is engineered for high-load applications, delivering a recovery rate of 70-90% to maximize water reuse and minimize waste discharge.
- Energy-Efficient Operation: This 200m3/hour ultrafiltration equipment features a power consumption of only 30kw/hour, significantly reducing the carbon footprint and lifecycle costs of large-scale water treatment plants.
- Precision Filtration Performance: Utilizing a 0.02um pore size, the system effectively removes viruses, bacteria, and colloids, providing superior RO pretreatment to extend the lifespan of downstream components.
- Global Compliance and Durability: Built according to ISO and CE standards, the equipment uses chemical-resistant materials suitable for the diverse climatic conditions found across the Middle East and Southeast Asia.
- Scalable Modular Design: The 200m3/hour ultrafiltration equipment solutions are designed for easy integration into existing infrastructure, allowing for rapid deployment and simplified maintenance routines in diverse industrial sectors.
The first step in making sure you have a long-term plan for managing water is to look at the technical details and the manufacturer's reputation. By looking at the molecular weight cut-off and flow rates, it is possible to find the best design for different industry wastes. Procurement teams can make decisions that are good for the environment in the long run by using data to figure out the total cost of ownership, which includes everything from the initial power draw to the membrane's lifespan. Standardized membrane configurations and high-recovery parts make filtration work reliably in a wide range of industrial settings around the world.
Guangdong Morui: A Worldwide Leader in High-Capacity Water Treatment
Guangdong Morui Environmental Technology Co.,Ltd got its start in 2005. We build advanced water treatment systems. After nearly twenty years in this field, we've grown into a major global supplier of large-scale filtration equipment and a 200m3/hour ultrafiltration equipment supplier for industrial clients. Our flagship system is a 200m3/hour ultrafiltration unit. It is built to handle the hard demands of industrial process engineering.
We've completed projects all over South America, Southeast Asia, Europe, the Middle East, and Africa. That's our track record. The MR-UF-200TH is built for industrial wastewater treatment. Its high-performance membranes feature a 0.02μm pore size. They trap suspended solids and pathogens. The unit achieves a 70-90% recovery rate and draws only 30kw/hour at optimized power. International manufacturing groups and local utility plants rely on it, and as a 200m3/hour ultrafiltration equipment supplier, we help them stay compliant and keep operations efficient.
Quality and reliability come first in our production. Our plant follows a strict ISO 9001 management system. That means every 200m3/hour ultrafiltration unit meets CE and ROHS certifications. Our on-time delivery rate is 98%. Strict testing backs that rate. It guarantees consistent flux rates and chemical resistance, even when feed water conditions change.
Guangdong Morui offers full technical support to keep systems performing over the long term. This covers remote system debugging and on-site training for local engineers in the markets we serve. We want to be a transparent, capable partner. Your next large-scale water treatment project needs technical depth and lasting value, and we bring both.
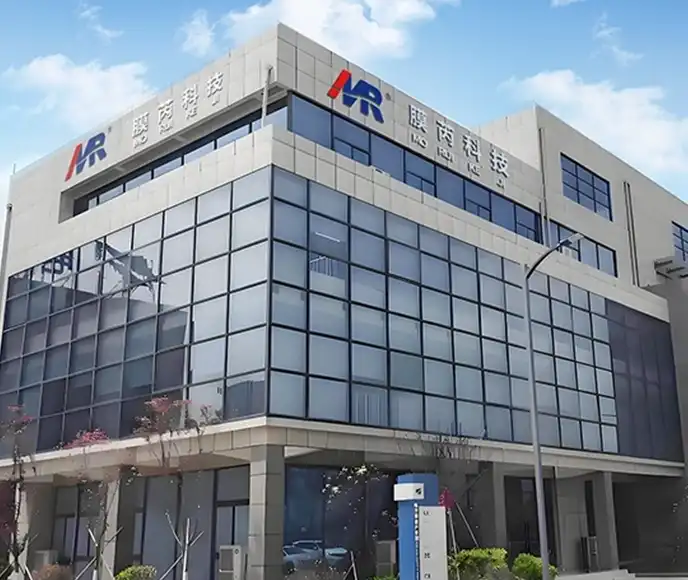
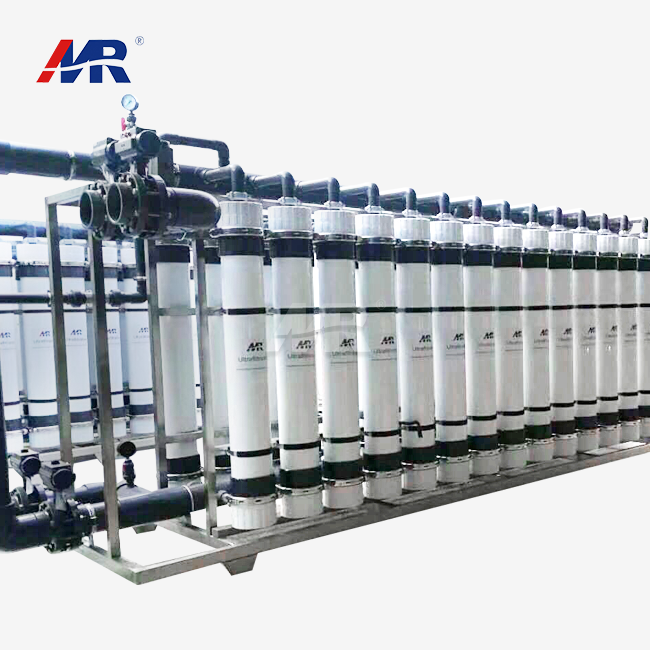
High Capacity Industrial Wastewater Recovery with 200m3/hour Ultrafiltration Systems
I. Application Scenarios
The 200m3/hour ultrafiltration equipment supplier is a key barrier for getting rid of suspended solids and macromolecules in industrial water treatment. Usually, this high-capacity system is used in
Textile and Dyeing Wastewater: Creating a physical barrier to get rid of organics and microscopic matter that change color, so water can be recycled.
RO pre-treatment lowers the Silt Density Index (SDI) to protect the Reverse Osmosis membranes further downstream in large-scale desalination or boiler feed water systems.
Pulp and Paper Effluent: Handling large amounts of waste to meet strict environmental standards while also getting process water back.
II. Customer Pain Points and Challenges
South America, Southeast Asia, Europe, the Middle East, and Africa all have their own problems that industrial managers have to deal with:
Strict Regulatory Compliance: To meet EU standards (ROHS) or specific environmental discharge permits, the effluent quality must be stable, which is something that regular sand filters can't promise.
High Operating Costs: Africa and the Middle East have big problems with energy use; systems that don't work well cause electricity bills that can't be paid.
Feed Water Changes: In Southeast Asia, changes in the clarity of raw water that happen with the seasons can cause membranes to get clogged up often and cause unplanned downtime.
Maintenance Barriers: In remote areas, a small problem can become a system failure that lasts for weeks because there isn't enough local technical know-how or extra parts.
III. Guangdong Morui Environmental Technology Solution
The Guangdong Morui Environmental Technology Co., Ltd company was founded in 2005 and offers a modular solution based on the MR-UF-200TH model. Twenty years of technical experience have been put into this small, high-performance package for treating industrial wastewater. The system is a reliable "plug-and-play" design that keeps permeate quality stable even when feed conditions change. It is made with ISO-certified materials and a focus on reliability.
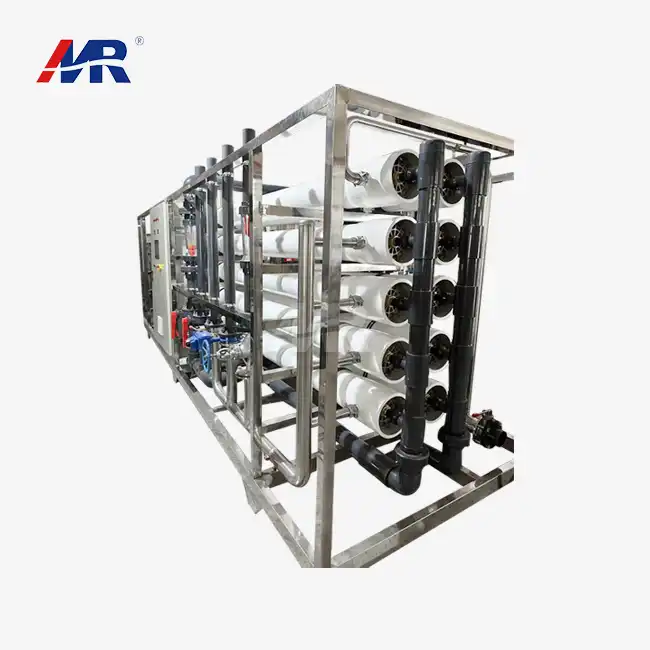
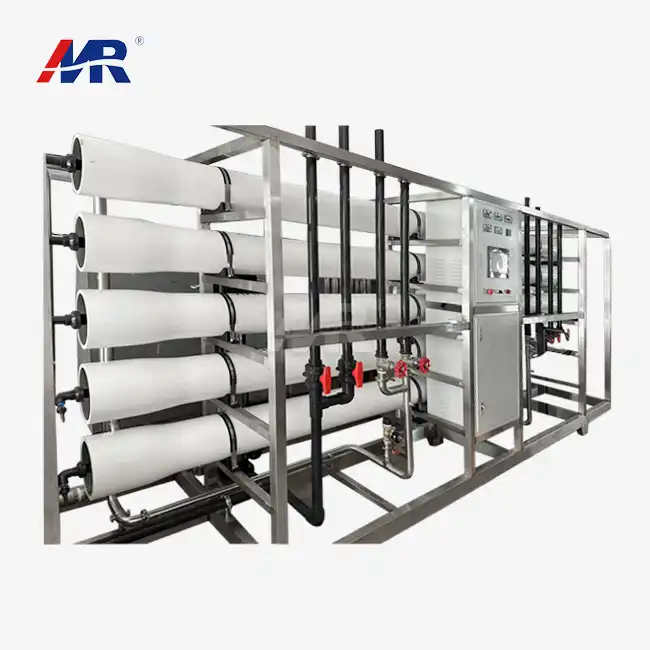
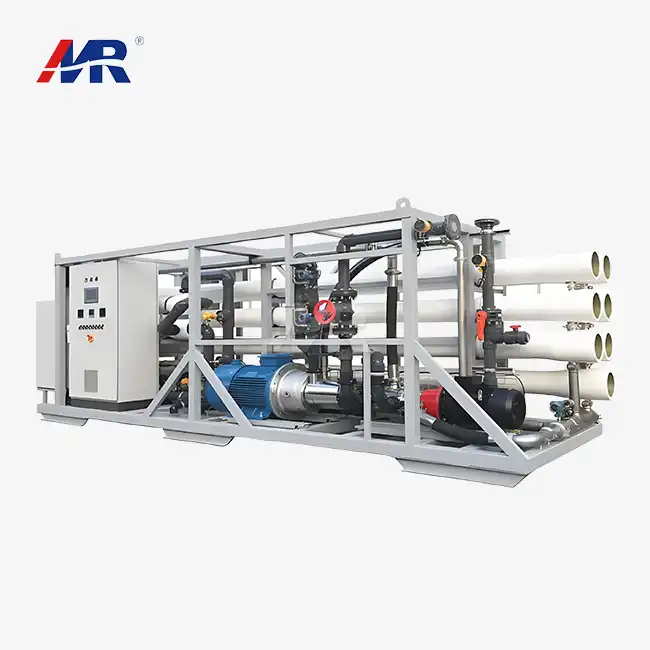
IV. System Architecture and Key Components
The 200m3/hour system is engineered for maximum reliability and minimal manual intervention:
- Automated Pre-treatment Unit: Utilizes multi-media or self-cleaning strainers to remove large particles, protecting the 0.02um membranes from physical damage.
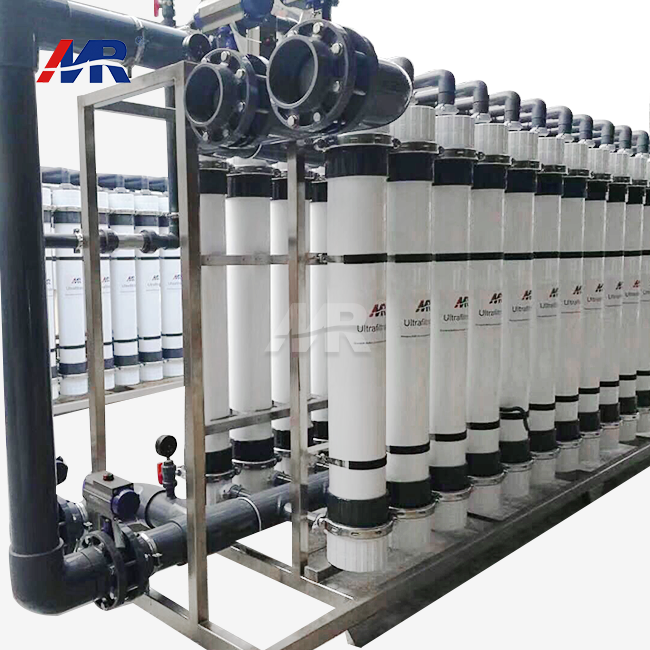
- MR-UF-200TH Core Membrane Module: Featuring a 0.02um micron rating, this unit effectively rejects bacteria, viruses, and colloidal silica, maintaining a high recovery rate of 70-90%.
- Intelligent PLC Control System: A centralized SCADA-compatible interface manages the 30kw/hour power consumption through variable frequency drives, ensuring the system operates at peak efficiency.
- Clean-In-Place (CIP) Module: An integrated chemical cleaning skid facilitates automated maintenance cycles, extending membrane life by effectively removing organic and inorganic scaling.
V. Solution Advantages and Quantifiable Benefits
- Enhanced Water Recovery: The system achieves a 70-90% recovery rate, significantly reducing raw water intake costs.
- Superior Filtration Precision: The 0.02um pore size ensures consistent effluent quality, meeting strict industrial reuse standards.
- Low Energy Footprint: Optimized hydraulic design limits power consumption to approximately 30kw per hour for the entire 200m3/h flow.
- Space Efficiency: The skid-mounted modular design reduces the installation footprint by up to 30% compared to conventional clarification.
- Certified Reliability: Full compliance with ISO, CE, and ROHS standards ensures global compatibility and safety.
VI. Implementation Flow and Global Service
A full water chemistry study is the first step in the application process. Next comes a unique system design and factory acceptance testing (FAT). Clients in South America, Southeast Asia, and the Middle East can get remote diagnostic help and a structured supply chain for spare parts. The technical teams set up the spot and train the staff so that the local workers can do daily upkeep and fixing well.
VII. Typical Application Case
A large-scale manufacturing plant in Southeast Asia required a solution to treat 200m3/h of high-turbidity industrial effluent for cooling tower makeup. The existing system suffered from frequent RO membrane fouling. By installing the MR-UF-200TH solution, the plant achieved a stable SDI < 3.0 and reduced chemical consumption by 40%. The project resulted in a 20% reduction in overall water procurement costs within the first year of operation.
VIII. Technical Consultation
Consulting with technical experts allows for the precise matching of membrane materials and flux rates to specific wastewater characteristics. Detailed case reports and pilot study data are available to assist in the verification of system performance for large-scale industrial deployments across diverse geographic regions.
The high-performance PVDF membrane architecture ensures stable permeate quality while significantly lowering the total cost of ownership for large-scale industrial water reclamation projects.
FAQs
1. What are the key performance benefits of deploying 200m3/hour ultrafiltration equipment for industrial wastewater treatment?
Implementing a high-capacity system like the MR-UF-200TH offers significant advantages in large-scale operations. With a filtration precision of 0.02um (microns), this equipment acts as a physical barrier against suspended solids, bacteria, and macromolecules. One of its primary benefits is the high recovery rate of 70-90%, which significantly reduces water waste. Furthermore, the 200m3/hour ultrafiltration equipment serves as an ideal pretreatment stage for Reverse Osmosis (RO), protecting downstream membranes from colloidal fouling. Guangdong Morui Environmental Technology Co., Ltd. designs these systems to operate at low transmembrane pressures, ensuring stable flux even under fluctuating feed water conditions. For optimal results, we recommend monitoring the Molecular Weight Cut-Off (MWCO) and maintaining consistent backwash cycles to preserve the 0.02um membrane integrity over long-term industrial use.2. How can I verify the manufacturing capability and authenticity of a supplier for a 200m3/hour ultrafiltration equipment?
When investing in large-scale water treatment assets, verifying supplier credibility is crucial for long-term reliability. A reputable manufacturer should demonstrate extensive industry experience; for instance, Guangdong Morui Environmental Technology Co., Ltd. has been specialized in water treatment since 2005. You should look for international certifications such as ISO 9001 for quality management, alongside CE and ROHS compliance, which are essential for markets in Europe and beyond. To verify strength, request technical drawings of the Model MR-UF-200TH and evidence of previous installations in your region, whether in Southeast Asia, the Middle East, or South America. We suggest reviewing the supplier’s ability to provide detailed energy consumption data—such as our optimized 30kw/hour rating—and post-purchase technical support to ensure you are partnering with a genuine factory rather than a middleman.3. In regions with high-fouling water like Southeast Asia or Africa, how does the 200m3/hour ultrafiltration equipment ensure stable operation?
Industrial wastewater in tropical or developing regions often contains high organic loads that can lead to rapid membrane fouling. Our 200m3/hour ultrafiltration equipment utilizes high-performance membranes (typically PVDF or PES) that offer superior chemical resistance to oxidative cleaning agents like Sodium Hypochlorite. The 0.02um pore size is specifically selected to balance high flow rates with rigorous particle rejection. To maintain the 70-90% recovery rate in these environments, we recommend a three-step approach: first, ensuring proper chemical enhanced backwash (CEB) protocols; second, utilizing the system’s modular design for easy maintenance; and third, monitoring the 30kw/hour power consumption to detect early signs of pressure buildup. If your project faces specific local water challenges, Guangdong Morui can provide customized flux calculations to ensure the equipment meets local industrial standards.4. What international certifications and local regulations apply to 200m3/hour ultrafiltration equipment in Europe and South America?
Exporting water treatment technology to Europe, South America, or the Middle East requires strict adherence to safety and environmental standards. The 200m3/hour ultrafiltration equipment from Guangdong Morui is manufactured under ISO standards and carries CE and ROHS certifications, ensuring it meets European health, safety, and environmental protection requirements. In South America, while specific national regulations (such as those from ANVISA in Brazil or similar bodies) may apply depending on the application, having CE and ISO 9001 certification generally streamlines the local approval process. We recommend that buyers confirm specific local discharge limits for industrial wastewater, as these will dictate the necessary recovery rate and post-treatment requirements. Our team can assist in providing the technical documentation needed to prove compliance with both international and regional water quality directives.5. How does the 30kw/hour energy consumption of the 200m3/hour ultrafiltration equipment impact long-term operational costs?
Energy efficiency is a critical factor for large-scale industrial projects. Our 200m3/hour ultrafiltration equipment is engineered to consume approximately 30kw/hour, which is highly competitive for a system processing 200 cubic meters of water per hour. By operating at a lower transmembrane pressure compared to traditional filtration methods, the MR-UF-200TH reduces the electrical load on feed pumps. To maximize cost-efficiency, we suggest: 1) Implementing automated variable frequency drives (VFDs) to match pump speed with demand; 2) Regularly cleaning the 0.02um membranes to prevent "pressure creep" which increases power draw; and 3) Optimizing the recovery rate between 70-90% to balance water output with energy input. Since 2005, Guangdong Morui has focused on lowering the Total Cost of Ownership (TCO), and we invite you to contact us for a detailed energy ROI analysis based on your local utility rates.
Best Selling Products
Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.