



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
50m3/hour ultrafiltration plant factory
Precision-Engineered 50m3/h UF Systems for Global Industrial Factories
In fast-industrializing spots like Southeast Asia and the Middle East, big manufacturing plants often deal with raw water quality that swings around and throws production schedules off, plus it can wear out downstream equipment. If you source water treatment hardware through middlemen, you often end up with technical mismatches and maintenance that drags. That is why it pays to work directly with a 50m3/hour ultrafiltration plant factory that knows what high-volume, continuous water purification really demands.
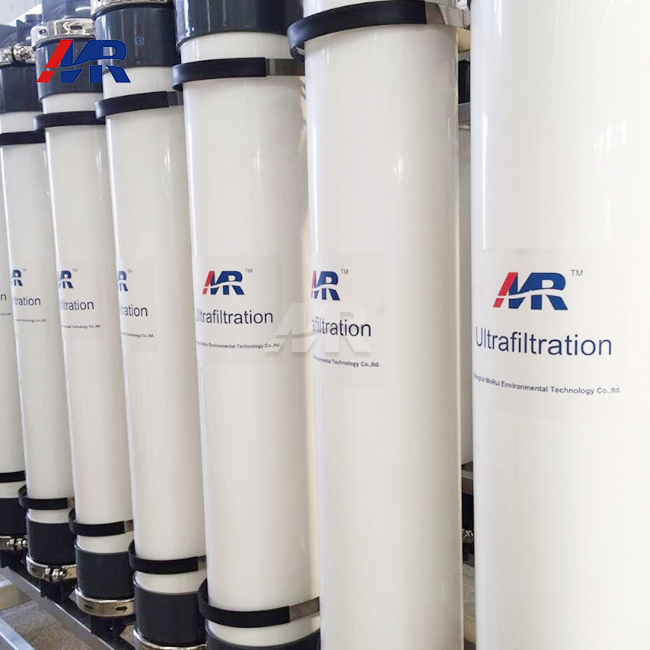
For textile or food processing plants in South America and Africa, unplanned downtime due to membrane fouling can result in significant financial losses. A direct factory partnership ensures that the MR-UF-50TH model is not just a catalog item but a ready-to-deploy solution with predictable lead times and verified performance metrics. Unlike trading companies, a dedicated manufacturing facility manages the entire assembly line, allowing for a month-on-month capacity assurance that supports projects ranging from single 50 m³/h units to integrated multi-line clusters. By working with the source, factories secure critical components and PVDF membranes at lower procurement costs while receiving the direct technical documentation required for local environmental compliance.
Operating at a low pressure of 0.1-0.3Mpa, our systems are specifically engineered to handle the high turbidity, SS, and COD levels typical in European industrial wastewater recycling. Choosing a professional manufacturer allows for deep customization, such as integrating specific PLC controls or adapting the 7.5kw/hour power consumption to local energy grid requirements. Our factory-tested recovery rates of 70-90% ensure that facilities can maximize water reuse, a vital factor in regions where water scarcity directly impacts operational overhead. This level of technical transparency and accountability is only possible when the supplier owns the production floor and the quality control laboratory.
Guangdong Morui Environmental Technology Co.,Ltd leverages decades of manufacturing expertise to bridge the gap between complex water treatment needs and reliable engineering. In the following sections, you’ll see how our 50m3/hour ultrafiltration plant solutions optimize operational stability through automated backwashing and robust physical barriers against bacteria and suspended solids. Each MR-UF-50TH unit reflects a commitment to energy-efficient filtration and long-term membrane integrity for diverse global industrial environments.
Related Products




About Guangdong Morui Environmental Technology Co.,Ltd
Guangdong Morui Environmental Technology Co.,Ltd began back in 2005. Since then, we've grown into a leading high-tech company focused on researching, developing, and building advanced water treatment systems. Our home base is in Guangdong's industrial heart, and as a 50m3/hour ultrafiltration plant factory we've made membrane technology our go-to solution for tough hard water purification challenges. Over the past 18 years, we've built a complete operation that spans engineering design, precision equipment fabrication, and technical support around the world.
We take pride in our 50m3/hour ultrafiltration plant factory, which embodies Ultrafiltration Manufacturing Excellence for 50m³/hour operations.
We're a direct manufacturer. Our plant is set up for high-capacity units such as the Model MR-UF-50TH. These 50m³/hour ultrafiltration plants are made for serious industrial needs. They strip out turbidity, suspended solids (SS), and COD with high efficiency. Because the line is factory-direct, every unit stays energy-lean. It draws only 7.5kw/hour, yet it still reaches an impressive water recovery rate of 70-90%.
Strict quality management, aligned with ISO standards, guides our manufacturing. That keeps operations consistent on large-scale projects. Every plant we ship carries CE certification, so you know it meets European safety and performance rules. We also follow ROHS directives. That means our membrane components and structural materials are environmentally responsible and free of hazardous substances. Need a specific setup? With OEM/ODM capabilities, we can customize operating pressures (0.1-0.3Mpa) and filtration stages to match your local water chemistry.
Global Reach, Proven Reliability
We hold our work to high standards. That's why customers in five major regions trust us: South America, Southeast Asia, Europe, the Middle East, and Africa. Thousands of water treatment projects have shipped under our name. Our clients come from many sectors, ranging from municipal utilities to pharmaceutical and food processing operations. Pick Morui and you're working with a manufacturer that brings nearly two decades of technical expertise, along with a solid track record in international compliance and dependable logistics.

Advanced Manufacturing Excellence for 50m3/hour Industrial Ultrafiltration Plants
Solution Overview for 50m3/hour Ultrafiltration Plant Factory
Guangdong Morui Environmental Technology Co.,Ltd builds a heavy-duty 50m3/hour ultrafiltration (UF) plant for tough industrial sites. Standard off-the-shelf units are a different story. Our factory-engineered MR-UF-50TH is designed to tackle large-scale water treatment problems, including high turbidity, suspended solids (SS), and COD removal. Because we are the direct manufacturer, every 50m3/hour unit that leaves our 50m3/hour ultrafiltration plant factory is built for structural integrity and stable long-term operation. This factory-first approach helps connect complex engineering needs with reliable onsite execution. It's a good fit for clients in the Middle East and Southeast Asia who need high-throughput systems that can handle changing raw water quality.
Precision Engineering and Regional Customization
Our engineering team designs the MR-UF-50TH with energy efficiency and regional adaptability in mind. It uses only 7.5kw/hour. That makes this 50m3/hour ultrafiltration plant a good fit for regions such as Africa and South America, where operating costs and power stability are major concerns. We set the system to run within a 0.1-0.3Mpa pressure range, so it reaches a high recovery rate of 70-90%. Our factory can adjust membrane materials, such as PVDF or PAN, to meet pH requirements from 2 to 12. All technical designs follow local environmental regulations across Europe and other target markets. The modular setup allows quick deployment and easy integration into existing industrial water circuits.
Factory Production and Manufacturing Control
As a dedicated ultrafiltration plant factory, Guangdong Morui keeps strict control over the full production lifecycle. Our manufacturing facility uses advanced assembly lines. Key components, such as high-precision UF membranes and automated control valves, go through rigorous testing before final assembly. We run a multi-stage quality control process. It centers on pressure testing and flux rate verification, so each MR-UF-50TH meets its rated capacity of 50m3/hour. For large-scale projects, we offer optimized delivery cycles and batch production to meet tight construction schedules. In a recent project for a Southeast Asian manufacturing hub, our factory delivered and commissioned a multi-unit UF system within an accelerated timeframe. Permeate quality stayed consistent even under challenging inlet conditions.
Global Compliance and Technical Lifecycle Support
Different continents have different regulatory landscapes. That takes a manufacturer with deep compliance expertise. Our 50m3/hour ultrafiltration plant systems are built to meet international standards for water purification, safety, and mechanical durability. Beyond manufacturing, the factory offers full technical support. This includes detailed installation guidance and operator training for local teams. We know that for industrial facilities in remote parts of Africa or the Middle East, downtime is not an option. So our systems include automated backwashing protocols and specialized Clean-In-Place (CIP) systems. These extend membrane life and make routine maintenance simpler. We also provide remote diagnostic support, so the 50m3/hour system keeps running at peak efficiency throughout its entire service life.
Strategic Value of Factory-Direct UF Solutions
Choosing a factory-direct partner for your 50m3/hour ultrafiltration plant offers distinct competitive advantages for industrial operations:
- Enhanced Energy Performance: The MR-UF-50TH’s 7.5kw power consumption profile significantly reduces long-term overhead for high-capacity industrial users.
- Superior Particle Removal: COD, SS, and turbidity are effectively targeted by advanced membrane technology. That keeps downstream processes, such as Reverse Osmosis, protected.
- Reliable Water Recovery: Recovery rates can reach as high as 90%. That lowers wastewater discharge and makes resource use as efficient as possible in regions where water is scarce.
- Transparent Quality Assurance: Every component goes through factory-level inspections. Those checks confirm it meets the specific pressure and temperature thresholds that industrial durability requires.
- Direct Engineering Access: Work directly with the manufacturer. That cuts out communication barriers and gets you customized spare parts and technical expertise faster.
The MR-UF-50TH model delivers high-capacity water purification through energy-efficient membrane filtration and precision-engineered industrial components.
FAQs
1. How does the MR-UF-50TH 50m3/hour ultrafiltration plant work, and what are its primary industrial applications?
The MR-UF-50TH 50m3/hour ultrafiltration plant operates on a sophisticated size exclusion principle, utilizing semi-permeable membranes to remove contaminants like bacteria, viruses, colloids, and suspended solids. This specific model is engineered to handle high-capacity demands, effectively reducing turbidity, SS, and COD from raw water sources. It is widely applied in pre-treatment for Reverse Osmosis (RO) systems, pharmaceutical water production, and industrial wastewater recycling across Southeast Asia and the Middle East. By maintaining an operating pressure of 0.1-0.3Mpa, the system ensures a high recovery rate of 70-90%. Whether you are managing a municipal water project or a large-scale food and beverage facility, this plant provides a consistent permeate flow that meets stringent international safety standards, ensuring that downstream equipment is protected from fouling and premature degradation.2. What are the key technical specifications and energy efficiency benefits of the 50m3/hour ultrafiltration plant?
Efficiency is a core advantage of the MR-UF-50TH model. This 50m3/hour ultrafiltration plant is designed with a low power consumption profile of just 7.5kw/hour, making it an ideal choice for regions with high energy costs, such as Europe and parts of Africa. Technologically, the system utilizes PVDF or PAN membrane materials, which support a wide pH range of 2 to 12, allowing for versatile chemical cleaning options. With a stable recovery rate of up to 90%, the plant minimizes water wastage, which is critical for sustainable water management in water-stressed areas like the Middle East. The compact design and automated control systems allow for real-time monitoring of flux rates and pressure differentials, ensuring the plant operates at peak performance while reducing the total cost of ownership for industrial users.3. What routine maintenance is required to ensure the longevity of a 50m3/hour ultrafiltration plant?
To maintain the integrity of the membranes and ensure the long-term reliability of the 50m3/hour ultrafiltration plant, a structured maintenance protocol is essential. This includes automated backwashing cycles to dislodge particles from the membrane surface and periodic Clean-In-Place (CIP) procedures using mild acidic or alkaline solutions to remove organic fouling and scaling. Operators should monitor the inlet water quality, ensuring turbidity remains below 5NTU and temperature is ideally maintained near 25°C for optimal permeability. Guangdong Morui Environmental Technology provides detailed technical manuals and training for maintenance staff, especially for clients in South America and Africa where local technical support might be remote. By following these manufacturer-recommended protocols and replacing pre-filters regularly, users can significantly extend the lifespan of the UF membranes, preventing costly downtime and maintaining high-quality water output.4. How does your 50m3/hour ultrafiltration plant factory ensure quality control and compliance for international exports?
As a professional 50m3/hour ultrafiltration plant factory, Guangdong Morui Environmental Technology Co.,Ltd. adheres to rigorous ISO9001 quality management standards. Every unit, including the MR-UF-50TH, undergoes a comprehensive 48-hour pressure test and membrane integrity verification before dispatch. We recognize the specific regulatory requirements in markets like Europe and South America; therefore, our components often carry CE or relevant material certifications. Our factory is open for third-party inspections (such as SGS or BV) to verify our manufacturing capacity and the authenticity of the materials used. By controlling the entire production process—from frame welding to PLC programming—we ensure that every 50m3/hour ultrafiltration plant factory shipment meets the exact specifications promised in the technical datasheet, providing global buyers with the confidence that they are receiving a robust, industrial-grade system.5. What are the lead times and logistics support provided by the factory for projects in Southeast Asia and Africa?
Choosing a direct manufacturer like Guangdong Morui offers significant advantages in terms of customization and logistics. For a standard 50m3/hour ultrafiltration plant, our factory typically maintains a production lead time of 4 to 6 weeks, depending on the specific customization of the control system or material requirements. We have extensive experience shipping to major ports in Southeast Asia (such as Jakarta and Manila) and Africa (such as Lagos and Durban), handling all export documentation and offering CIF or DDU terms to simplify the process for our clients. Beyond delivery, our 50m3/hour ultrafiltration plant factory provides dedicated remote technical support and can dispatch engineering teams for on-site commissioning for large-scale infrastructure projects. This end-to-end service ensures that our international partners receive not just a product, but a fully operational water treatment solution tailored to their local environmental conditions.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.