

Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
150m3/hour reverse osmosis plant supplier
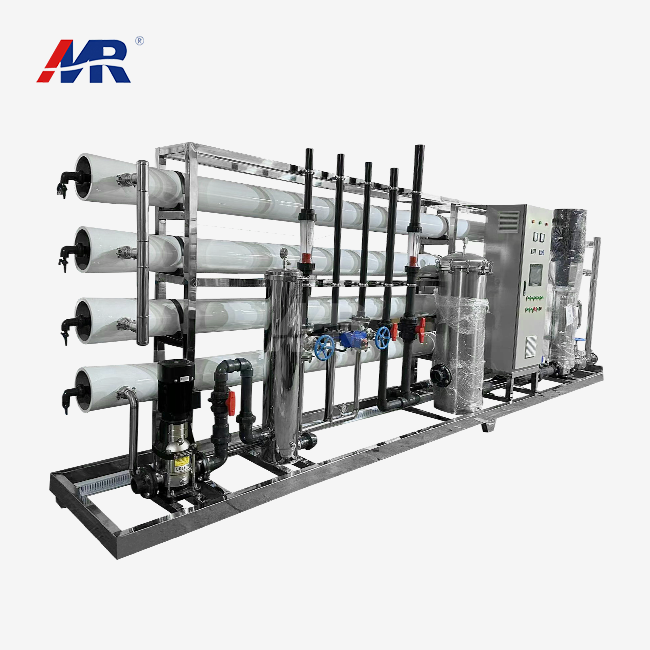
Engineering and Supply for a Certified Industrial 150m3/hour Reverse Osmosis Plant
Procurement managers running large industrial water treatment projects in South America, Southeast Asia, Europe, the Middle East, and Africa need a dependable 150m3/hour reverse osmosis plant to keep operations running. This plant, sourced through a reliable 150m3/hour reverse osmosis plant supplier, is central to high-capacity purification. Semi-permeable membranes strip out up to 98% of dissolved salts and contaminants from feedwater. Power generators, large manufacturers, and other operators count on systems like this one. Water quality affects how long equipment lasts and whether product integrity holds up.
Industrial water treatment in the Middle East and Southeast Asia often runs into problems that can put a project's ROI at risk. Feedwater salinity tends to shift, which shortens membrane life and causes downtime you didn't plan for. Energy use is still a major hurdle in African and South American markets, where power stability varies and operating costs are watched closely. Projects in Europe have to meet strict ISO and CE compliance. It is also hard to confirm how strong a distant supplier's manufacturing really is, so many teams look for a 150m3/hour reverse osmosis plant supplier that can prove its capabilities before committing. All of this adds up to serious risk across a long procurement cycle.
Guangdong Morui Environmental Technology Co., Ltd started in 2005 and has nearly two decades of experience. The company makes the MR-BWRO-150TH, a rugged 150m3/hour reverse osmosis plant. We build our systems for tough and varied industrial water treatment settings, from the humid tropics of Southeast Asia to the dry climates of the Middle East. Morui holds ISO, CE, and ROHS certifications. Every 150m3/hour reverse osmosis plant we produce meets international safety and quality standards. That helps ease customs clearance and site integration in global markets. Our long history in this field gives buyers the transparency and technical know-how to check supplier capability before they commit large-scale capital.
- High-efficiency salt rejection: The MR-BWRO-150TH reaches a 98% salt rejection rate. This produces high-purity permeate for demanding industrial water treatment processes.
- Optimized energy performance: At 150kw/hour, this 150m3/hour reverse osmosis plant keeps output high while reining in power use. That lowers overall OPEX.
- Adaptive recovery rates: The system provides a flexible recovery rate of 55-75%. Operators can tune water yield to suit local feedwater availability and environmental rules in Africa or South America.
- Global compliance and durability: We use ISO-certified manufacturing and high-grade pressure vessels. The plant stands up to corrosive conditions often found in large-scale 150m3/hour reverse osmosis plant solutions.
If you're the one making the technical call, pull the full specs for the MR-BWRO-150TH. Set them next to your site's feedwater analysis. We also supply detailed documentation. That includes P&ID diagrams and energy efficiency reports. Use those to confirm the purchase is the right fit and to satisfy local regulatory standards. Need pre-treatment stages designed for your region? Our experienced engineers can customize them to handle local water issues, such as high turbidity or organic fouling.
The MR-BWRO-150TH pairs high-rejection membrane technology with energy-optimized high-pressure pumps. That combination delivers consistent water quality for industrial use.
Guangdong Morui Environmental Technology: High-Capacity Water Treatment Leader
Founded in 2005, Guangdong Morui Environmental Technology Co., Ltd has grown into a top global provider of large-scale industrial water treatment systems. Nearly two decades of expertise have made us a top-tier manufacturer of heavy-duty systems, and as a 150m3/hour reverse osmosis plant supplier, we have built a reputation for reliable performance. We serve critical infrastructure needs across South America, Southeast Asia, Europe, the Middle East, and Africa.
The Model MR-BWRO-150TH is made for tough industrial settings. It delivers a 98% salt rejection rate and an optimized recovery rate of 55-75%. We have put these systems to work at international brand factories and municipal projects. Our "plug-and-play" containerized designs, supported by our work as a 150m3/hour reverse osmosis plant supplier, solve complex onsite construction challenges. We stick to ISO, CE, and ROHS certifications. That ensures every 150m3/hour reverse osmosis plant meets the highest international safety and performance standards.
Rigorous factory acceptance testing (FAT) verifies quality and confirms a stable power consumption of 150kw/hour. Our mature supply chain helps us keep a high on-time delivery rate, even on multi-unit international orders.
Morui supports customers worldwide with a full range of technical services, including remote commissioning, on-site installation training, and localized maintenance support in regions like the Middle East and Southeast Asia. We are committed to long-term value in water treatment. Our sustainable, efficient purification systems drive industrial growth.
150m3/h Reverse Osmosis Solutions, Optimized for Large-Scale Industry
I. Application Scenarios at a Glance
Large industrial water treatment relies on critical infrastructure. When you're running a 150m3/hour reverse osmosis plant for high-volume operations, picking the right 150m3/hour reverse osmosis plant supplier matters. Guangdong Morui Environmental Technology Co.,Ltd, founded in 2005, designs these systems. They're built for sites where water quality directly affects production efficiency. Typical applications include:
- Power plant boiler feed: ultra-pure water from a 150m3/hour reverse osmosis plant supplier keeps high-pressure boilers free from scaling and corrosion.
- Large-scale textile and dyeing: steady water chemistry keeps color precise and protects fabric integrity.
- Centralized industrial parks: the system serves as a utility hub. It supplies treated process water to several manufacturing units at once.
II. Common Customer Pain Points
Running high-capacity water systems brings regional hurdles of its own in markets like Southeast Asia, the Middle East, and Africa:
- Regulatory Compliance: Plants in Europe and South America must meet strict ISO and CE standards. These rules are not optional. Miss them, and you face legal liability or trade barriers.
- High Operational Costs: Power use runs at 150kw/hour, so energy efficiency is a major concern. If a system wastes power, OPEX goes up and your margins shrink.
- Water Scarcity and Discharge Limits: In dry areas like the Middle East, water is scarce. To cut raw water intake and keep brine discharge low, you need a recovery rate of 55-75%.
- Maintenance Downtime: In remote parts of Africa or Southeast Asia, membrane fouling can stop an entire production line. Each hour of downtime costs thousands of dollars.
III. Morui's Industrial Solution
Guangdong Morui provides a modular, turnkey system built around the Model: MR-BWRO-150TH. We bring nearly two decades of experience. Our approach has shifted from basic filtration to a "smart utility" model. Advanced membranes work with automated diagnostics to maintain a 98% salt rejection rate. When raw water quality changes, that gives you reliable protection.
IV. System Design and Key Parts
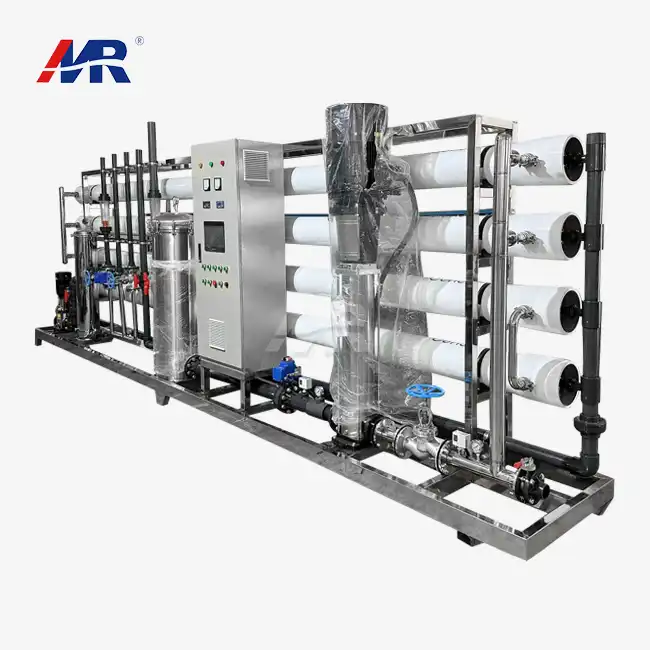
Advanced Pretreatment Unit
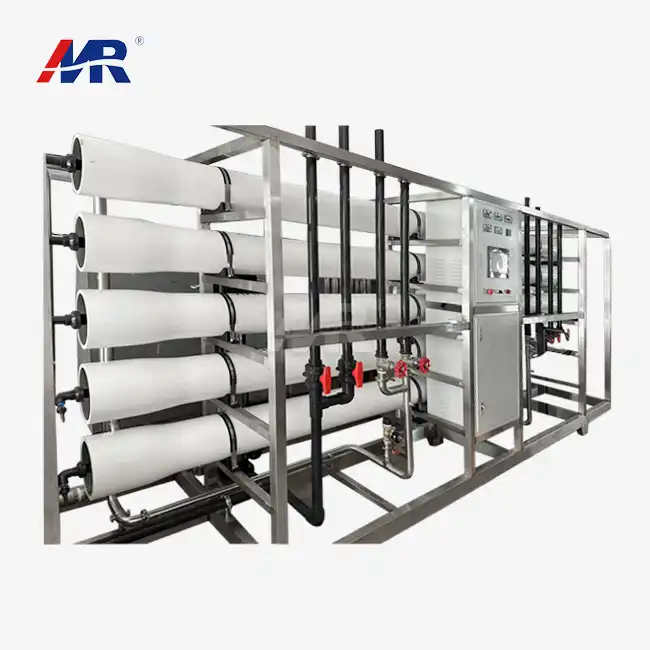
Tropical climates mean high turbidity and heavy organic loads. This unit handles both. Automated multimedia filters and carbon towers handle the prep work up front, so the primary RO membranes don't foul ahead of schedule.
High-Flux RO Membrane Rack
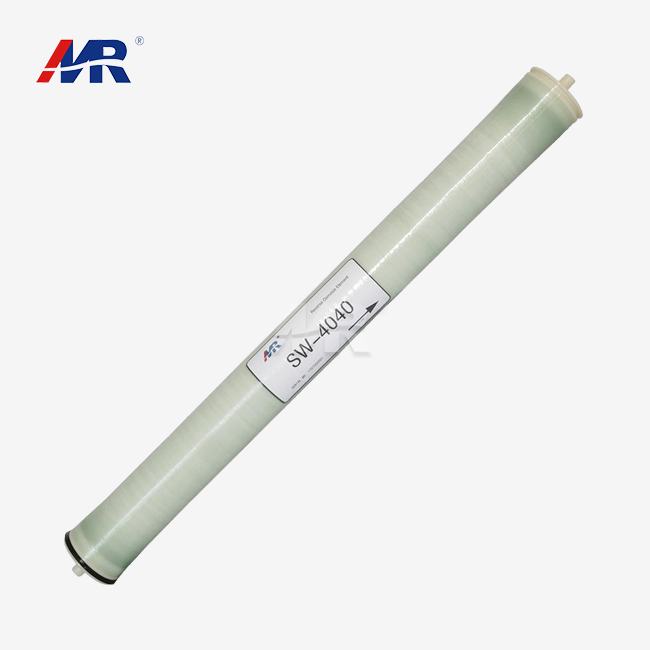
At the center of the 150m3/hour plant sit premium brackish water membranes. Their layout squeezes the most out of the flux-to-pressure ratio, turning a 150kw/hour power draw into the highest permeate output it can reach.
Automated Control and SCADA Integration
PLC-based automation lets the system read flow rates and conductivity as they happen. That matters a great deal in European markets, where buyers require digital traceability and strict operational safety standards.
Integrated Cleaning-in-Place (CIP) Module
Maintenance was a worry, so the package includes a dedicated CIP skid. It carries out automated chemical cleaning cycles. That stretches membrane life and trims the manual labor bill in high-cost regions.
V. Solution Benefits and Quantifiable Gains
- High purity. Salt rejection holds steady at 98%, meeting the highest industrial water standards.
- Better resource use. Recovery rates climb as high as 75%, which sharply lowers the cost per cubic meter of treated water.
- Energy control. The system is designed to hold a steady 150 kW/hour load, so energy use stays level.
- Global certification. Full compliance with ISO, CE, and ROHS lets it fit into international supply chains without friction.
- Lower total cost of ownership. The modular design trims on-site installation time by up to 40% against traditional builds.
VI. Implementation and Global Service Capability
Guangdong Morui supports the full lifecycle of the 150m3/hour plant. We start with water analysis and engineering that fits the site, then stay through final commissioning. Our projects span South America and the Middle East. We also handle remote diagnostics and a fast spare parts supply chain, keeping operations stable over the long term in different locations.
VII. Example Application: Industrial Park in Southeast Asia
Rising salinity in the groundwater at a big manufacturing hub in Southeast Asia put production at risk. The plant installed the MR-BWRO-150TH system, and it now holds a steady 150m3/h flow of high-purity water. Chemical costs dropped 25%, and corrosion on equipment fell sharply throughout the factory.
VIII. Help with Technical Selection
Want a setup built around your feedwater TDS and what you pay for energy locally? Ask us for technical data sheets and project reports from your region.
Across every industrial sector, anywhere in the world, high-performance membrane technology keeps permeate quality steady.
FAQs
1. What are the key technical specifications and performance expectations for a 150m3/hour reverse osmosis plant?
A 150m3/hour reverse osmosis plant, such as the Guangdong Morui Model MR-BWRO-150TH, is designed for large-scale industrial water treatment. Key performance metrics include a salt rejection rate of 98%, which measures the system's efficiency in removing dissolved salts, minerals, and impurities from the feed water. This model typically operates with a recovery rate between 55% and 75%, balancing water output with waste reduction. In terms of energy, users should account for a power consumption of approximately 150kw/hour. For optimal performance, we recommend regular monitoring of the RO membranes and ensuring the pre-filtration stage effectively removes larger particles and chlorine to prevent premature fouling. If you have specific influent water quality data, our team can provide a more precise projection of your treated water quality.2. How should I choose the right 150m3/hour reverse osmosis plant for industrial facilities in Southeast Asia or South America?
Selecting a 150m3/hour reverse osmosis plant for regions like Southeast Asia or South America requires considering local environmental factors such as high humidity, ambient temperature, and raw water turbidity. First, conduct a comprehensive water analysis to identify potential scaling or organic fouling issues common in these climates. Second, evaluate the energy efficiency; our systems are optimized at 150kw/hour to balance operational costs with high-volume output. Third, prioritize durability by choosing high-quality materials like stainless steel or FRP (Fiber Reinforced Plastic) for pressure vessels. With Guangdong Morui’s experience since 2005, we suggest looking for "plug-and-play" or containerized designs for easier mobilization to remote project sites. Always verify that the supplier can provide a robust spare parts kit for local maintenance.3. What certifications are necessary for a 150m3/hour reverse osmosis plant to comply with European or Middle Eastern standards?
When importing a 150m3/hour reverse osmosis plant into Europe or the Middle East, compliance with international quality and safety standards is mandatory. The equipment should carry ISO 9001 certification for quality management, CE marking for European safety requirements, and ROHS compliance for hazardous substance restriction. These certifications ensure the industrial water treatment system meets rigorous structural and electrical safety benchmarks. Additionally, while the equipment itself is certified, you must ensure the final water output meets local environmental discharge or potable water regulations, which vary by country. Guangdong Morui Environmental Technology Co., Ltd maintains these global certifications to facilitate smoother customs clearance and project approvals. We recommend consulting with our technical experts to confirm that the specific materials used meet your local regional health and safety codes.4. How does the MR-BWRO-150TH model handle high-energy costs and membrane fouling in industrial water treatment?
Energy consumption and membrane fouling are the two biggest operational challenges in large-scale water treatment. Our 150m3/hour reverse osmosis plant is engineered with a recovery rate of 55-75%, allowing for significant water reuse while managing energy at a steady 150kw/hour. To combat fouling—the buildup of particles on the membrane—the system incorporates advanced pre-filtration stages to remove sediment and chlorine. We also recommend implementing an automated Clean-In-Place (CIP) system to periodically wash the membranes without disassembly. This maintains the 98% salt rejection rate over a longer lifespan. For industries in Africa or the Middle East where water source quality fluctuates, adding an ultrafiltration (UF) pre-treatment stage can further protect the RO membranes and lower long-term maintenance costs.5. Can Guangdong Morui provide on-site installation and technical support for a 150m3/hour reverse osmosis plant in remote international markets?
Yes, Guangdong Morui Environmental Technology Co., Ltd, established in 2005, has extensive experience supporting projects across Southeast Asia, the Middle East, and Africa. For a 150m3/hour reverse osmosis plant, we offer comprehensive technical support ranging from initial site assessment to final commissioning. Our service typically includes providing detailed installation manuals, remote video guidance, or dispatching expert engineers for on-site supervision, depending on the project scope. To ensure long-term reliability in international markets, we offer training for your local operators on routine maintenance and troubleshooting of the 150kw/hour power system. We highly recommend discussing your specific site infrastructure and logistics requirements with us early in the planning phase to ensure a seamless integration of the RO plant into your facility.
Best Selling Products
Related Blogs
Related Search
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.