



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
electro deionizer system supplier
Advancing Ultrapure Water Standards with Electro Deionizer System Technology
Procurement managers in industrial markets across South America, Southeast Asia, Europe, the Middle East, and Africa have a tough job. Before they sign off on an electro deionizer system supplier, they need to be sure the supplier's technical skills are solid. That check matters for keeping operations running well over the long term. An electro deionizer system is a water treatment setup. Electricity, ion exchange membranes, and a special resin work together to pull dissolved ions out of water continuously. When those parts work as one, the system can produce high-purity water. This setup avoids the environmental dangers and shipping headaches that come with traditional chemical regeneration.
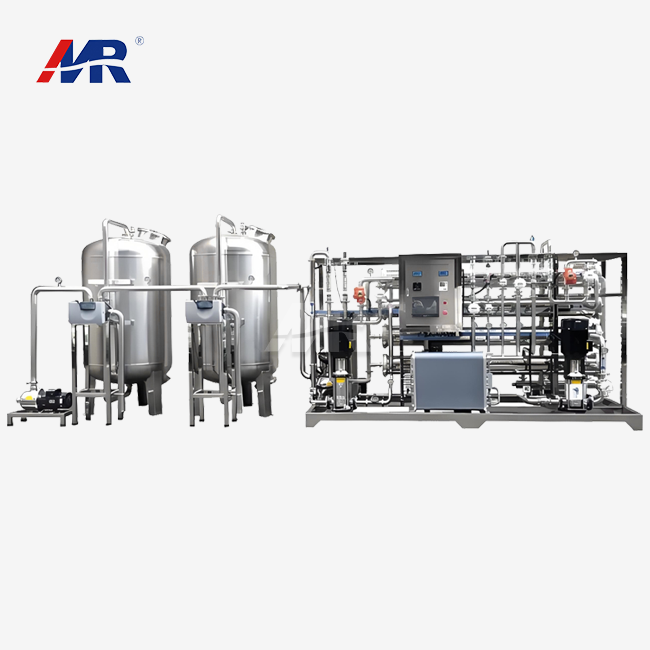
In places like Southeast Asia and Africa, plants often face two problems: feed water quality that shifts, and energy that costs a lot. Buyers have other headaches too. Local rules require ISO and CE compliance. Inefficient power use drives up operating costs. And keeping salt rejection rates high is hard when the climate varies so much. Thin technical documentation is another issue, along with downtime risks from complex maintenance. Either one can threaten the stability of ultrapure water production lines.
Guangdong Morui Environmental Technology Co., Ltd. started in 2005. The company takes on these global challenges with engineered electro deionizer system solutions. Reliability and performance that buyers can verify come first. Morui specializes in making electro deionizer systems. Its equipment, such as the MR-EDI-5TH model, is built for ultrapure water use in demanding sectors. The system keeps resource use and output in balance, with a 60% recovery rate and a 99.99% salt rejection rate. It also holds ISO, CE, and ROHS certifications. Those marks show it meets international quality benchmarks. For buyers, that gives a clear framework for technical verification during procurement.
- The MR-EDI-5TH delivers high-precision salt rejection: a 99.99% rate. That rate keeps ultrapure water production steady for high-tech industrial water treatment applications.
- Energy-Efficient Operation: The electro deionizer draws 16kw/hour. That design cuts both the carbon footprint and the operating cost in markets where energy prices matter, such as Europe and the Middle East.
- International Compliance Standards: ISO, CE, and ROHS certifications guide our manufacturing. That way, every unit meets the safety and environmental rules required for use in South America and Southeast Asia.
- Optimized Resource Recovery: A 60% recovery rate lets a facility make the most of its water. In water-stressed parts of Africa, that matters for industrial sustainability.
- Chemical-Free Deionization Technology: The system regenerates electrically, so no hazardous acids or caustics are needed. That makes the workplace safer and removes the cost of chemical waste disposal.
Technical specs still get careful review. That step remains key to securing a steady supply of high-purity water for industrial operations worldwide. For large-scale infrastructure investment, complete system design and certified manufacturing processes provide the needed assurance. The MR-EDI-5TH model shows a commitment to high-performance deionization. It rests on precise engineering and rigorous international certification standards.
Related Products
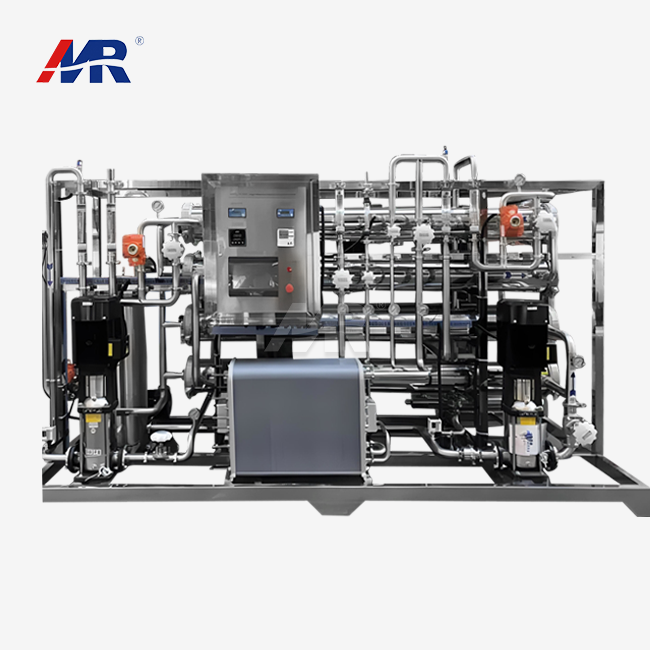




Reliable Ultrapure Water Solutions: About Guangdong Morui Environmental Technology Co., Ltd.
Guangdong Morui Environmental Technology Co., Ltd. was founded in 2005. We're a leading manufacturer focused on water treatment. With nearly two decades of experience, we've become a top electro deionizer system supplier known for high-performance solutions. Our systems serve mission-critical industries across Southeast Asia, Europe, the Middle East, South America, and Africa.
Our MR-EDI-5TH series is a good example of our technical strength: a high-efficiency electro deionizer system built for ultrapure water production. We designed these systems to replace traditional chemical-intensive deionization, and as a electro deionizer system supplier, we achieve a 99.99% salt rejection rate and a 60% recovery rate. You'll often find them in power plant boiler feed and high-precision manufacturing, where consistent, chemical-free water purity is a must.
We put quality and safety first. Our quality management system is demanding and holds ISO, CE, and ROHS certification. Our equipment is designed to run efficiently. The MR-EDI-5TH model, for instance, uses only 16kw/hour. This keeps the workflow sustainable and automated, with very little operator intervention.
To support our global clientele, we provide a robust service network offering remote technical debugging, onsite training, and comprehensive maintenance packages. Whether you are operating in the industrial hubs of Southeast Asia or the emerging markets of Africa, Morui Environmental ensures your ultrapure water needs are met with precision and reliability. Partner with us for scalable, long-term excellence in electro deionization technology.

Intelligent High-Purity Water via Advanced Electro Deionization Systems
I. Application Scenario Overview
High-precision industries can't do without ultra-pure water. An electrodeionization (EDI) system, the kind an electro deionizer system supplier can supply, takes care of the last polishing step in water treatment. It does the same job as traditional mixed-bed resin tanks. Common uses include:
- Power generation: High-quality boiler feed water from a trusted electro deionizer system supplier prevents scaling and corrosion in high-pressure turbines.
- Electronics & Semiconductors: Ultrapure water (UPW) cleans wafers. Even tiny amounts of ionic impurities can drag yields down.
- Pharmaceutical production: Injection-grade water has to meet strict pharmacopeia standards. This method meets them without the risks of handling chemicals.
II. Customer Struggles and How Regions Differ
Plant operators in South America, Southeast Asia, Europe, the Middle East, and Africa all face their own day-to-day problems:
- Chemical Logistics and Safety: Take Europe and South America. Strict environmental rules like REACH and ISO 14001 drive up the cost of handling and disposing of the acid and caustic soda used to regenerate resin. The legal side is also getting harder to manage.
- High Operating Costs: In the Middle East and Africa, energy efficiency and water recovery come first. Utility bills run high, and water is scarce.
- Technical Skill Shortages: Traditional deionization needs a lot of hands-on work. Many facilities in Southeast Asia have trouble keeping up. Downtime is common, and water quality varies.
III. Guangdong Morui’s EDI Solution
Guangdong Morui Environmental Technology Co., Ltd, established in 2005, provides a chemical-free, modular solution centered on the MR-EDI-5TH series. Our approach integrates electricity, ion-exchange membranes, and resin to continuously deionize water. This "Green Technology" eliminates the need for hazardous regeneration chemicals, providing a stable, automated supply of ultrapure water that meets ISO, CE, and ROHS certifications.
IV. System Architecture and Key Components
- Advanced Pre-treatment Unit: To protect the EDI stack from hardness scaling, we implement high-precision RO filtration, ensuring feedwater meets the necessary conductivity and low-hardness thresholds.
- MR-EDI-5TH Host Module: The core unit utilizes a specialized DC electric field to drive ion migration. With a salt rejection rate of 99.99%, it ensures the highest purity levels for sensitive industrial loops.
- Power & Control Logic: Optimized for efficiency, the system consumes only 16kw/hour, utilizing a PLC-based interface for fully autonomous operation without manual supervision.
- Continuous Regeneration (CEDI): Unlike batch systems, our design allows for in-situ resin regeneration via water molecule splitting, maintaining a 60% recovery rate during constant flow.
V. Solution Advantages and Benefits You Can Measure
- Superior Purity: Salt rejection reaches 99.99%. The water it produces holds a steady resistivity of 15-18 MΩ·cm.
- Reduced Footprint: The modular design takes up far less floor space than bulky mixed-bed ion exchangers.
- Energy Efficiency: Power draw is low at 16kw/hour. Over time, that lowers operating costs by about 20-30%.
- Environmental compliance: The system needs no wastewater neutralization. That means it meets environmental standards in Europe and South America.
- Reliable uptime: The system runs without stopping. Chemical regeneration cycles typically mean 8-12 hours of downtime. This system does not have that problem.
VI. Implementation and Service Capabilities
Serving diverse global markets, we provide comprehensive engineering support from initial site analysis to final commissioning. Our service framework for international clients includes remote diagnostic capabilities and a robust supply chain for rapid spare parts delivery in Southeast Asia and the Middle East. We provide detailed technical training to local staff to ensure long-term system integrity and performance.
VII. Typical Application Case
A large-scale power plant in Southeast Asia required a stable boiler feed solution to replace an aging chemical-intensive system. By implementing the MR-EDI-5TH solution, the facility eliminated the procurement of hazardous chemicals and achieved a 99.99% reduction in dissolved solids. The automated control system reduced the need for specialized on-site chemists, while the 16kw/hour efficiency profile lowered monthly energy costs significantly.
VIII. Engineering Specifications and Value
Technical documentation includes detailed flow diagrams, energy consumption profiles, and ionic rejection benchmarks for specific feed water conditions. Robust construction and ISO-certified manufacturing keep the system at peak performance in harsh industrial environments.
Continuous ion removal keeps ultrapure water stable for critical industrial processes.
FAQs
1. What is an electro deionizer system and why is it preferred over traditional mixed-bed deionization?
An electro deionizer system (EDI) is a sustainable, advanced technology that combines ion exchange membranes and electricity to produce ultrapure water without the need for hazardous chemical regeneration. Unlike traditional systems that require acids and caustics to regenerate resin beads, an EDI system uses a DC electric field to continuously split water molecules into hydrogen and hydroxyl ions. This process keeps the resin active in situ, ensuring a stable, high-purity output with a salt rejection rate of up to 99.99%. Guangdong Morui Environmental Technology Co.,Ltd, with expertise dating back to 2005, designs these systems to eliminate the risks of chemical handling and the environmental burden of neutralized wastewater discharge. For modern industries, switching to EDI provides a continuous, automated solution for high-purity water needs.2. How do I determine the right capacity and model for an electro deionizer system for my facility?
Selecting the appropriate electro deionizer system depends on your specific ultrapure water requirements and operational efficiency goals. For example, our MR-EDI-5TH model is designed for high-performance industrial applications, offering a recovery rate of approximately 60% and power consumption of 16kw/hour. When evaluating a system, you should prioritize parameters such as feed water conductivity, desired flow rate, and energy efficiency. Since 2005, we have helped clients across Southeast Asia and Europe balance these parameters to ensure long-term reliability. We recommend analyzing your daily peak flow requirements and the footprint available in your plant. Please contact Guangdong Morui Environmental Technology with your project specifications for a detailed selection report and a customized configuration.3. In regions like the Middle East or Southeast Asia, what pre-treatment is necessary for an electro deionizer system?
In regions like the Middle East and Southeast Asia, raw water often contains high levels of hardness or dissolved minerals, which can lead to scaling within an electro deionizer system. Calcium carbonate buildup is a primary concern as it can clog internal membranes and significantly reduce the efficiency of the ion exchange process. To protect your investment, a robust pre-treatment stage—typically involving a high-quality Reverse Osmosis (RO) system—is essential to lower the incoming water's hardness and total organic carbon (TOC) levels. We suggest strictly monitoring the feed water parameters to ensure they meet the specific input requirements of the EDI module. If you are operating in areas with challenging water conditions, our technical team can help design a multi-stage pre-treatment solution to maximize system longevity.4. Does your equipment comply with international standards for export to Europe, South America, or Africa?
Yes, our water treatment solutions are designed to meet rigorous international quality and safety benchmarks. Guangdong Morui Environmental Technology holds ISO, CE, and ROHS certifications, which are critical for importing an electro deionizer system into markets like Europe, South America, and Africa. These certifications verify that our equipment meets essential health, safety, and environmental protection standards. While our products comply with these broad international frameworks, we always advise clients to verify specific local grid requirements or regional environmental discharge regulations within their specific country. Our team is experienced in preparing the necessary documentation and technical specifications to ensure smooth customs clearance and compliance for your local industrial infrastructure projects.5. Can Guangdong Morui Environmental Technology provide technical support and installation for projects located in South America or Africa?
Guangdong Morui Environmental Technology Co.,Ltd understands the complexities of managing water treatment projects in remote or international locations like South America and Africa. We provide comprehensive technical support, which includes remote video guidance and, depending on the project scale, on-site installation and commissioning services. Since our founding in 2005, we have developed a streamlined process to assist international clients with system setup and operator training to ensure the MR-EDI-5TH operates at peak performance. Our electro deionizer systems are engineered for ease of use with minimal supervision, but we remain available to troubleshoot performance issues or advise on membrane maintenance. For large-scale industrial projects, we can coordinate technical resources to ensure your ultrapure water system is reliable from day one.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.