



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
1000LPH EDI plant supplier
Reliable 1000LPH EDI Plant for Global High-Purity Water Standards
If you're buying equipment for a company in South America, Southeast Asia, or the Middle East and you need a dependable 1000LPH EDI plant, the 1000LPH EDI plant supplier you go with decides how well that system holds up over the years. A 1000LPH EDI plant is an electrodeionization setup. Ion exchange membranes and DC voltage work together to produce ultrapure water nonstop, without the shipping hassle or safety hazards that come with chemical regeneration. Guangdong Morui Environmental Technology Co.,Ltd has led the way in this technology since 2005, building tough systems for water treatment operations worldwide.
Plants in Africa and Southeast Asia often deal with two issues: how long the equipment lasts and how much it costs to run. Feed water quality swings, and picking a solid 1000LPH EDI plant supplier matters because that scales the EDI stack. Power is expensive in remote industrial areas. Meeting strict environmental rules without hazardous acids or alkalis is another tough part. Many sites also lack technical support nearby, so when standard parts fail, downtime stretches out and total cost of ownership climbs.
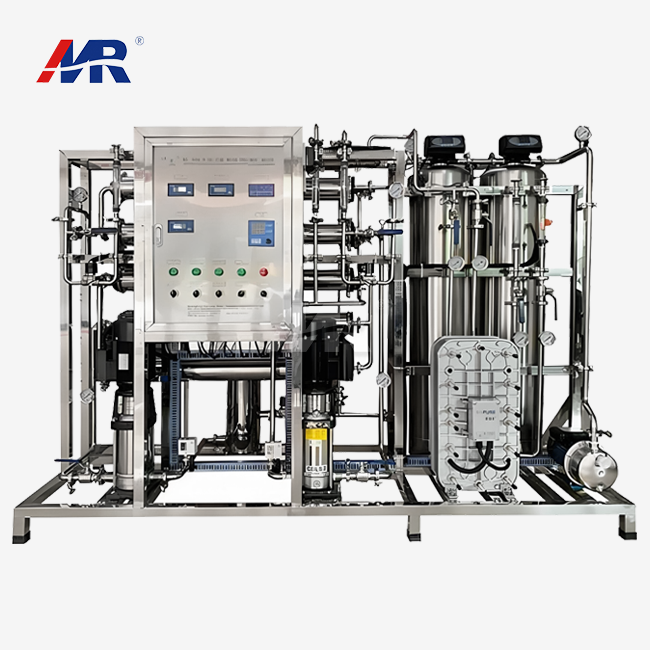
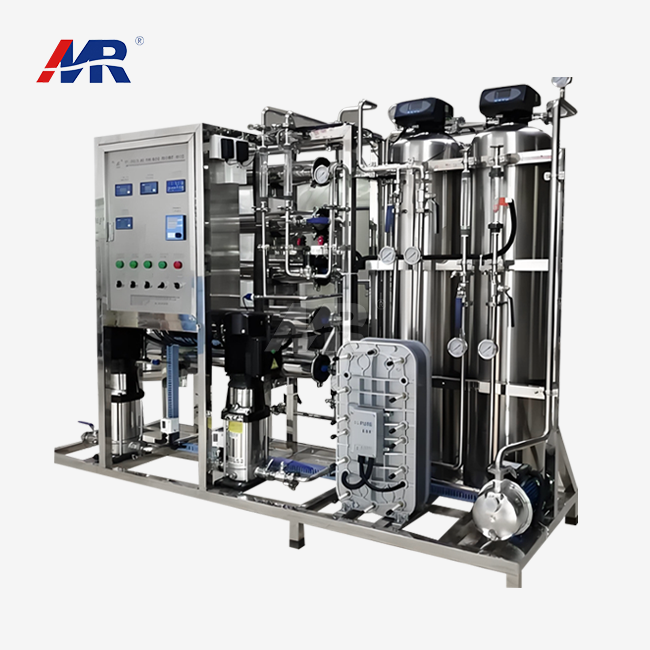
Guangdong Morui Environmental Technology Co.,Ltd builds high-performance 1000LPH EDI plant solutions for customers around the world. Our MR-EDI-1TH model is made for ultrapure water production. It keeps efficiency high across very different climates, from the humid air of Southeast Asia to the dry heat of the Middle East. The systems carry ISO, CE, and ROHS certifications, so they guarantee compliance with international safety and quality standards. We also make buying simple, with nearly two decades of manufacturing experience and a strong global supply chain behind every 1000LPH EDI plant.
- Optimized energy efficiency: The MR-EDI-1TH runs on just 4kw/hour. That significantly lowers operating costs for large-scale water treatment projects.
- Strong deionization: This 1000LPH EDI plant has a salt rejection rate of 99.99%. It delivers steady output resistivity, which suits pharmaceutical and electronic manufacturing.
- Certified quality assurance: Full ISO, CE, and ROHS compliance. That makes customs clearance easier and helps secure local regulatory approval in European and South American markets.
- Durable Industrial Design: The system is made to run nonstop and holds a steady 55% recovery rate. That balance saves water and extends the life of the deionization modules.
- Expert Technical Documentation: The provision of comprehensive data sheets and validation support streamlines the verification process for international procurement departments and engineering firms.
Guangdong Morui Environmental Technology Co.,Ltd offers technical consultations. They help engineers match the MR-EDI-1TH specs to conditions at their site, so the system performs at its best. Professional support teams can also supply detailed technical drawings and performance simulations. That makes it easier to fit the system into infrastructure you already have. Because the deionization is electrically driven, ultrapure water is produced continuously. For modern high-tech manufacturing facilities, that means a sustainable alternative with no chemicals involved.
Related Products




Reliable Water Treatment Solutions: Guangdong Morui Environmental Technology
Guangdong Morui Environmental Technology Co.,Ltd got its start in 2005. We're a leading water treatment specialist worldwide. We design and build high-precision purification systems. Our main focus is the 1000LPH EDI plant for industrial ultrapure water. We work with customers across South America, Southeast Asia, Europe, the Middle East, and Africa. They need steady water quality and reliable operation, and as a dependable 1000LPH EDI plant supplier, we help make that happen.
Take the MR-EDI-1TH model, for example. It delivers a 99.99% salt rejection rate and holds resistivity steady, all without hazardous chemical regeneration. Designed for a 1m³/h flow rate, our systems use only 4kw/hour. That makes them a green, cost-effective replacement for traditional ion exchange. We're an ISO, CE, and ROHS-certified manufacturer. Every 1000LPH EDI plant we make, and we're a 1000LPH EDI plant supplier you can count on, meets strict international safety and performance standards.
We support our global partners with full technical services, such as remote commissioning and specialized training for local engineering teams. We keep a high on-time delivery rate and run strict factory acceptance testing (FAT), so installation is plug-and-play. Work with Guangdong Morui for sustainable, high-purity water solutions that extend your system's life and lower total cost of ownership.

Efficient 1000LPH EDI Systems for Global Ultrapure Water Production
Industrial Application Scenarios
High-purity water is a workhorse utility in many industries. The 1000LPH EDI plant works well for sites that want steady water quality without the hassle of chemical regeneration, and a dependable 1000LPH EDI plant supplier can make that setup even easier to run. In pharma, it delivers USP-grade purified water for formulation and equipment rinsing. Electronics and semiconductor plants in Southeast Asia use it to strip trace ions during wafer fabrication. Power plants in Europe and the Middle East depend on it to feed high-pressure boilers and help prevent scaling and corrosion.
Regional Hurdles and Customer Pain Points
Running ultrapure water systems in varied climates, from South America to Africa, brings its own problems. In Europe, rules like CE and ROHS call for strong environmental compliance, so working with a 1000LPH EDI plant supplier helps you avoid costly missteps. In Southeast Asia, many industries often struggle with high conductivity in their feed water.
- Chemical Management: Traditional ion exchange calls for bulk storage of acid and alkali. It brings major safety risks and high costs to dispose of neutralized waste.
- Operational Stability: Water quality in developing regions often changes. That can exhaust resin fast and cause unplanned downtime.
- Energy and Space: A lot of facilities face higher power bills and tight floor space. Older systems are bulky and draw too much power, so they no longer make sense.
Guangdong Morui Environmental Technology Co.,Ltd: The Solution
The solution draws on nearly two decades of expertise since 2005. At its core is a modular, integrated RO-EDI approach. It pairs membrane-based pre-treatment with the MR-EDI-1TH electrodeionization module. Together, they create a chemical-free, continuous production cycle. This turn-key engineering approach ensures the 1000LPH output meets stringent international standards. It also keeps the footprint compact for global shipping and installation.
System Design and Key Components
The 1000LPH EDI plant is split into purpose-built units. Each one helps the system last longer and keep water purity high:
- Advanced Pre-treatment Unit: It uses multi-media filtration and softening. These protect the downstream membranes from scaling and fouling. The unit is tuned for the high-hardness water often seen in the Middle East.
- MR-EDI-1TH Core Stack: This is the heart of the system. It combines high-efficiency ion-exchange membranes with resin. Together they reach a 99.99% salt rejection rate and hold resistivity between 10 and 16 MΩ·cm.
- Integrated Control Logic: A PLC runs the automation and tracks 4kw/hour power consumption along with flow rates. Remote monitoring is included, so operators rarely need to step in by hand.
- Recovery Optimization: The system is calibrated to hit a 55% recovery rate. That is the balance point between saving water and still flushing concentrate where TDS levels run high.
Quantifiable Solution Advantages
- Chemical-Free Purity: You never have to store or handle hazardous chemicals, which makes it easy to stay compliant with ROHS and ISO environmental standards.
- High Efficiency: Power draw is tuned to 4kw/hour. That keeps running costs lower than traditional thermal or chemical deionization.
- Stable performance: The EDI stack regenerates nonstop, so you avoid the quality "breakthrough" that resin beds often show.
- Compact integration: The 1000LPH skid-mounted design trims installation time by up to 40%.
- High rejection: the system consistently removes 99.99% of ions, which stops minerals from building up and protects sensitive equipment downstream.
Implementation and Global Service Capability
Guangdong Morui Environmental Technology Co.,Ltd facilitates a comprehensive implementation process, from initial water analysis to final commissioning. For clients in South America, Africa, and beyond, the company provides remote diagnostic support and a robust supply chain for spare parts. The systems are delivered with full documentation for CE certification, ensuring smooth integration into local industrial infrastructures.
Representative Case Study
A semiconductor manufacturer in Southeast Asia needed a stable ultrapure water supply to expand production. The facility had to deal with high salinity in its feed water and very little space. By installing the MR-EDI-1TH 1000LPH solution, the client achieved a stable resistivity of 15 MΩ·cm and reduced hazardous waste output by 100%. The modular design meant the system was running within two weeks of arriving on site.
With continuous deionization, critical industrial processes get a reliable supply of ultrapure water.
FAQs
1. How do I select the right 1000LPH EDI plant for my industrial ultrapure water production?
Selecting an efficient system like the Model MR-EDI-1TH requires a clear understanding of your required water quality and raw water source. A 1000LPH EDI plant is ideal for industries requiring high-purity water without chemical regeneration, such as pharmaceuticals or electronics. You should prioritize systems that offer a high salt rejection rate—Guangdong Morui’s units achieve 99.99%—to ensure the removal of residual ions. Additionally, evaluate the power efficiency; our system operates at 4kw/hour, balancing performance with operational costs. Since 2005, we have recommended that clients verify their feed water’s Total Organic Carbon (TOC) and hardness levels, as these parameters dictate the necessary pre-treatment. For a tailored configuration that matches your specific flow requirements, we suggest contacting Guangdong Morui Environmental Technology Co.,Ltd with your water analysis report.2. What are the long-term operational advantages of installing a 1000LPH EDI plant compared to traditional DI resin beds?
The primary advantage of a 1000LPH EDI plant is its continuous, chemical-free operation. Unlike traditional ion exchange (DI) resin beds that require downtime for acid and alkali regeneration, Electrodeionization (EDI) uses electricity to continuously regenerate the resin beads. This eliminates the need for hazardous chemical storage and reduces labor costs. Our MR-EDI-1TH model features a recovery rate of 55% and is designed for high-stability ultrapure water production. Technically, this translates to a lower Total Cost of Ownership (TCO) over a 3-to-5-year period due to reduced waste disposal and energy consumption of only 4kw/hour. For global markets like Europe and Southeast Asia, this "green" technology also helps facilities comply with increasingly strict environmental regulations regarding wastewater discharge.3. For projects in Southeast Asia or the Middle East, what feed water conditions are critical for a 1000LPH EDI plant?
In regions like Southeast Asia and the Middle East, source water often contains high levels of dissolved CO2 or mineral hardness, which can lead to scaling within the EDI stack. When deploying a 1000LPH EDI plant in these environments, it is essential to ensure robust Reverse Osmosis (RO) pre-treatment. Proper pre-treatment prevents calcium and magnesium from fouling the membranes, maintaining the system's 99.99% salt rejection capability. We also recommend installing a degasifier if CO2 levels exceed 5mg/L to protect the stack's efficiency. Guangdong Morui’s systems are engineered to maintain stable resistivity even under varying temperatures common in tropical or arid climates. To ensure your 1000LPH EDI plant performs optimally in these specific regional conditions, we advise a thorough water test to determine if additional softening or degasification stages are required.4. Does the 1000LPH EDI plant comply with international standards like CE or ISO for the European and South American markets?
Yes, compliance with international standards is vital for ensuring equipment safety and reliability. Guangdong Morui Environmental Technology Co.,Ltd is an ISO-certified manufacturer, and our 1000LPH EDI plant models, including the MR-EDI-1TH, carry CE and ROHS certifications. These qualifications ensure the system meets rigorous safety, health, and environmental protection requirements necessary for the European and South American markets. Generally, these projects involve adherence to specific electrical codes and pressure vessel regulations; however, exact requirements should be confirmed based on the project's local jurisdiction. Our equipment is designed to produce water that meets USP or ASTM Type I/II standards, making it suitable for high-end laboratory and industrial applications globally. Selecting a certified supplier ensures that your ultrapure water system is both legally compliant and technically sound.5. Can Guangdong Morui provide technical support and installation for a 1000LPH EDI plant in Africa or Southeast Asia?
Guangdong Morui has been a specialized water treatment provider since 2005, with extensive experience supporting projects across Africa, Southeast Asia, and the Middle East. For a 1000LPH EDI plant, we offer comprehensive technical support ranging from initial site evaluation to remote or on-site commissioning. The MR-EDI-1TH model is designed for ease of integration, but we understand that local infrastructure can vary. We provide detailed installation manuals, video guidance, and real-time technical consultations to ensure the 4kw/hour power system is configured correctly for your local grid. If your project is located in a remote region, we can discuss specialized maintenance kits to ensure long-term uptime. For large-scale industrial installations, we encourage you to contact us to discuss how our engineering team can support your local installation and operator training needs.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.