



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
mobile container reverse osmosis equipment supplier
Industrial Mobile Container Reverse Osmosis Equipment Supplier Strength
Procurement managers in South America, Southeast Asia, or the Middle East who need dependable water treatment know the score: before you commit, check how well a mobile container reverse osmosis equipment manufacturer knows its trade. That check, when you're dealing with a mobile container reverse osmosis equipment supplier, protects the project over the long run. Mobile container reverse osmosis equipment acts as a central, plug-and-play desalination unit. It packs pre-treatment, membrane filtration, and controls into a standard shipping container, so it can get to work fast in tough conditions.
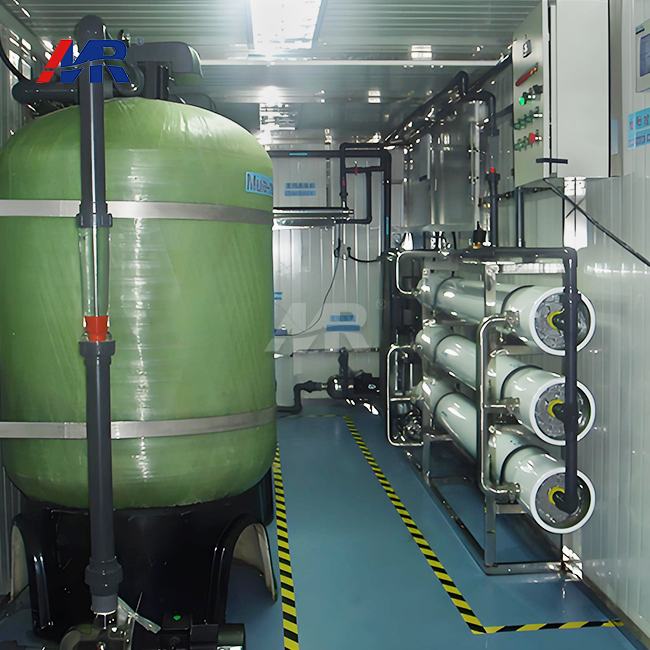
Industrial water treatment projects in places like Africa and Southeast Asia often run into real obstacles. Underground water can be very salty, and power grids can be unreliable. Common problems include high operating costs from inefficient energy use, the hard job of servicing systems in remote areas, and the need to meet strict international standards such as CE or ROHS for work in Europe and South America. Long delivery cycles and missing technical documentation can also hold up infrastructure development. That's why picking an experienced manufacturer matters for stable operations.
Guangdong Morui Environmental Technology Co.,Ltd has been around since 2005. The company tackles these problems with engineered mobile container reverse osmosis equipment that balances high output with the durability industrial sites need. Its ISO, CE, and ROHS certifications show every system meets global safety and quality benchmarks, which helps with customs clearance and getting equipment set up on site. The systems are built to handle the heavy pollution loads common in underground water desalination. Advanced membrane technology keeps a steady supply of purified water flowing for industrial processes.
Key technical advantages of the Morui containerized systems include:
- High-efficiency desalination performance: The MR-CTRO-25TH model reaches a 98% salt rejection rate. That turns brackish underground water into high-purity process water for industrial use.
- Optimized Energy Consumption: Built to run efficiently, the system draws 32kw per hour. That's a big drop in carbon footprint and utility costs, which counts for a lot in energy-sensitive regions like Africa.
- Superior Water Recovery Rates: Made for places where water is scarce, this mobile container reverse osmosis unit keeps a recovery rate of 55-65%. It gets the most out of the feedwater you have.
- Ruggedized for Harsh Climates: The container housing blocks out the extreme heat and humidity common in Southeast Asia and the Middle East. That helps the internal membrane elements last longer.
- Standardized Compliance and Safety: The system meets ISO and ROHS standards. That means every material and electrical component fits the strict rules found in Europe and South America.
Procurement professionals are encouraged to review comprehensive technical data sheets and case studies to validate the field performance of these systems. Engaging with technical engineers during the design phase allows for the customization of the mobile container reverse osmosis equipment to meet specific feed water chemistries and flow requirements. The integration of high-performance membranes and automated PLC controls within a reinforced enclosure provides a resilient solution for decentralized water purification requirements across diverse global landscapes.




Guangdong Morui Environmental Technology Co.,Ltd
Guangdong Morui Environmental Technology Co.,Ltd was founded back in 2005 and builds water treatment systems. We stay focused on high-performance equipment. As a mobile container reverse osmosis equipment supplier, we design and engineer mobile container reverse osmosis units. We also supply reliable purification systems to industrial and municipal clients across South America, Southeast Asia, Europe, the Middle East, and Africa.
The MR-CTRO-25TH is a solid showcase of what our tech team can do. It's a containerized system built for underground water desalination, and as a mobile container reverse osmosis equipment supplier, we designed it to keep salt rejection at 98% while recovery runs between 55-65%. Output stays high, and energy use holds steady at 32kw/hour. The modular units are quick to deploy, too. They work well for remote mining sites, offshore platforms, and local industrial plants that need a plug-and-play water supply right away.
Quality is the foundation of our work. Our manufacturing processes are certified under ISO 9001, and our products carry CE and ROHS marks. They meet international safety standards. Tight quality control and a strong supply chain help us keep an on-time delivery rate above 98% on projects worldwide.
Morui provides full technical support to keep operations running well long term. That support covers remote PLC debugging, on-site commissioning, and maintenance training adapted to the environmental conditions in our target markets. We're committed to being a partner you can trust, delivering water infrastructure that is sustainable and scalable for complex global needs.

Mobile Desalination Solutions for Challenging Remote Water Environments
Industrial Application Scenarios
Containerized reverse osmosis units earn their keep wherever local water systems are missing or have failed. In remote parts of South America and Africa, mining and energy firms use these systems, often from a mobile container reverse osmosis equipment supplier, to desalinate underground water. There, the units supply process water that operations rely on. In Southeast Asia, they provide backup for emergency municipal supply. And on construction sites in the Middle East, they act as temporary water stations, treating high-salinity groundwater until it meets industrial standards.
Regional Challenges and Everyday Pain Points
Water treatment systems operate in markets that differ widely, from Europe to the Middle East to Southeast Asia. Each region brings its own challenges, so a mobile container reverse osmosis equipment supplier can be a huge help:
- Regulatory compliance: ISO, CE, and ROHS standards are mandatory. They keep operations legal and environmentally safe, especially in Europe and South America.
- Energy and Resource Efficiency: Remote sites tend to use a lot of power and recover very little water. That drives running costs past what a project can sustain. When a system manages energy poorly, the project's profitability takes a hit right away.
- Maintenance and Durability: Harsh conditions wear parts out quickly. Take the heavy humidity in Southeast Asia or the extreme heat in the Middle East. The result is frequent downtime and high labor costs for repairs.
The Morui Containerized Engineering Approach
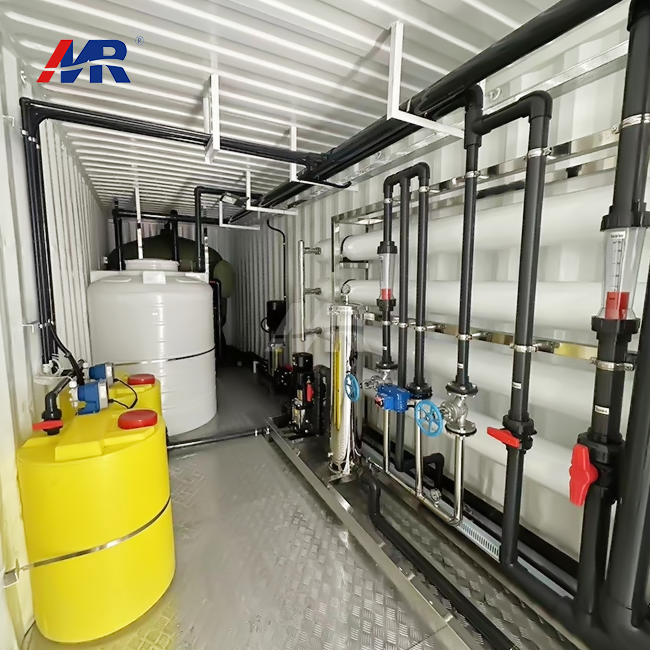
Guangdong Morui Environmental Technology Co.,Ltd, established in 2005, provides a comprehensive modular solution designed to bypass the complexities of traditional onsite construction. The mobile container reverse osmosis equipment is a "plug-and-play" turnkey system housed within reinforced shipping containers. This approach ensures rapid deployment and protects sensitive components from external environmental stressors, offering a stable water source regardless of local infrastructure limitations.
System Architecture and Technical Specifications
The MR-CTRO-25TH model brings several high-performance modules together in one mobile unit:
- Pre-treatment Module: Advanced filtration removes suspended solids and protects the RO membranes from fouling. It is designed to handle the high turbidity that groundwater often carries.
- RO Core (MR-CTRO-25TH): This central unit delivers 98% salt rejection and 55-65% recovery. Brackish or saline sources come out as high-purity permeate.
- Automated Control System: PLC and HMI give you real-time monitoring of flux and conductivity. That means less constant manual oversight.
- Energy Management: The system is built to run at 32kw/hour. That balances high-volume output with industrial energy efficiency.
Quantifiable Solution Benefits
- Rapid Commissioning: Because it's containerized, onsite installation takes up to 80% less time than with a traditional build.
- High Purity Output: A steady 98% salt rejection keeps water quality in line with industrial boiler and process requirements.
- Operational Savings: Optimized 32kw/hour energy consumption profile lowers the total cost of ownership in high-cost energy zones.
- Certified Reliability: Full compliance with CE, ISO, and ROHS standards guarantees long-term asset safety and international trade compliance.
Global Implementation and Service Capability
Guangdong Morui Environmental Technology Co.,Ltd supports operations worldwide with a structured process: site-specific water analysis, custom engineering, and international logistics. Technical support covers remote diagnostic capabilities and localized spare parts supply chains. This helps minimize downtime in South American and African markets.
Typical Application Example
A mining operation in a high-salinity region required consistent desalination for underground water. By implementing the MR-CTRO-25TH mobile containerized solution, the facility achieved a stable recovery rate of 60% and successfully reduced feedwater TDS to levels compliant with sensitive equipment specifications, all while operating within a compact 20-foot container footprint.
The mobile container reverse osmosis equipment integrates high-performance desalination technology with ruggedized housing for sustainable water production in decentralized locations.
FAQs
1. What are the primary advantages of using mobile container reverse osmosis equipment for underground water desalination in remote areas?
Mobile container reverse osmosis equipment offers a "plug-and-play" solution that is ideal for remote sites in Africa or Southeast Asia where permanent infrastructure is lacking. Unlike traditional fixed plants, these systems are housed in standard shipping containers, providing excellent protection against harsh environmental factors like blowing sand or high humidity. For instance, the MR-CTRO-25TH model is specifically engineered for underground water desalination, achieving a stable salt rejection rate of 98% and a recovery rate between 55-65%. Since Guangdong Morui Environmental Technology Co.,Ltd has been manufacturing these systems since 2005, the design emphasizes modularity and ease of transport. We recommend that users evaluate the raw water TDS (Total Dissolved Solids) and ensure the container includes integrated climate control to protect sensitive PLC electronics from extreme ambient temperatures.2. How does the energy consumption of the MR-CTRO-25TH model compare to standard industrial water treatment systems?
Energy efficiency is a critical factor for projects in regions with high utility costs, such as Europe or parts of South America. The MR-CTRO-25TH mobile container reverse osmosis equipment is designed with an optimized power profile, consuming approximately 32kw/hour during standard operation. By utilizing high-efficiency high-pressure pumps and advanced membrane technology, the system maximizes permeate output while maintaining an industrial-grade recovery rate. To further optimize energy use, we suggest implementing automated PLC controls that adjust flow rates based on real-time demand. For facilities looking to verify long-term operational costs, it is important to consider both the power draw and the durability of components like SS316L stainless steel piping, which reduces maintenance-related downtime. Guangdong Morui provides detailed energy profiles to help clients calculate the precise ROI for their specific site conditions.3. What international certifications and quality standards should I verify when selecting a supplier for mobile water treatment solutions?
When verifying the strength and reliability of a supplier, certifications act as a benchmark for safety and performance. A reputable manufacturer of mobile container reverse osmosis equipment should hold ISO 9001 for quality management, along with CE and ROHS certifications to ensure compliance with European safety and environmental standards. These credentials verify that the electrical systems and pressure vessels meet rigorous international requirements. Furthermore, ensure the equipment uses components that adhere to ASME standards for pressure safety. Guangdong Morui Environmental Technology Co.,Ltd maintains these certifications to support projects in global markets, including the Middle East and Europe. We suggest requesting a compliance dossier that includes material test reports and certificate authenticity to ensure the equipment meets the specific regulatory frameworks of your project’s home country.4. Can mobile container reverse osmosis equipment be customized to handle the specific water chemistry of different geographic regions?
Yes, customization is essential because underground water quality varies significantly between Southeast Asia and the Middle East. A robust mobile container reverse osmosis equipment system must include a tailored pre-treatment stage—such as multimedia filters or anti-scalant dosing—to protect the RO membranes from scaling and fouling. For example, if your source water has high iron content or high salinity, the system configuration must be adjusted to maintain the 98% salt rejection rate. We recommend providing a comprehensive water analysis report to our technical team; this allows us to calibrate the MR-CTRO-25TH model for optimal performance. Key parameters to monitor include pH levels, turbidity, and chemical oxygen demand (COD). Guangdong Morui can adapt the modular design to include specialized membrane elements or additional filtration stages depending on these local water characteristics.5. What kind of technical support and installation assistance is available for containerized RO systems in South America and Africa?
For international projects, the modular nature of mobile container reverse osmosis equipment significantly simplifies the installation process. Most units are pre-assembled, pre-piped, and factory-tested, meaning they only require connection to a power source and water inlet/outlet upon arrival. Guangdong Morui Environmental Technology Co.,Ltd provides comprehensive technical support, including detailed installation manuals, video guidance, and remote PLC monitoring capabilities to assist local engineers. If a project requires on-site commissioning in regions like South America or Africa, we can coordinate technical supervision to ensure the 55-65% recovery rate is achieved under local conditions. We encourage clients to establish a routine maintenance schedule involving membrane cleaning (CIP) and filter replacements, and our team remains available to provide spare parts and troubleshooting advice to ensure the long-term stability of the water supply.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.