



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
reverse osmosis membrane supplier
High-Performance Reverse Osmosis Membranes for Industrial Use Worldwide
If you're a procurement manager sourcing a reliable reverse osmosis membrane for large industrial projects in South America, Southeast Asia, Europe, the Middle East, and Africa, start by figuring out how deep a supplier's technical knowledge really goes. The membrane is the engine of a water treatment system, and any reverse osmosis membrane supplier worth their salt should know that inside and out. It's a semi-permeable thin-film composite barrier. Under hydraulic pressure, it strips out dissolved salts, minerals, and organic contaminants. Because it separates solutes at the molecular level, the system can deliver the high-purity permeate that many industrial applications need.
Plants in regions like Southeast Asia and the Middle East often deal with harsh operating conditions that hurt the bottom line. High Total Dissolved Solids (TDS) and feed water temperatures that keep swinging lead to inconsistent permeate quality and membrane fouling that keeps coming back. Energy costs add more pressure, and a reliable reverse osmosis membrane supplier can help you avoid paying for wasted energy. An inefficient membrane needs higher operating pressure to hold its flow rate, and that shows up on the bill. Then there are the complex international compliance standards to meet. For projects in remote areas or tightly regulated territories, keeping a system stable over the long term while cutting maintenance downtime is still the main concern.
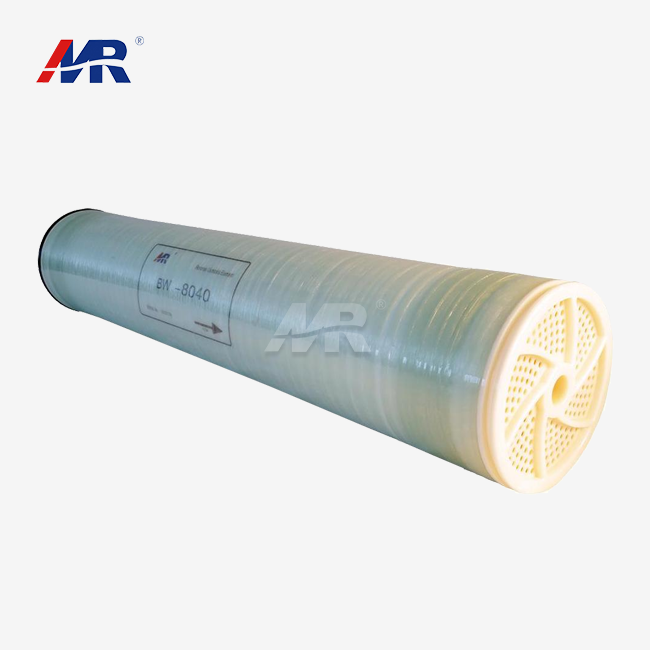
Guangdong Morui Environmental Technology Co., Ltd was founded in 2005 and offers specialized reverse osmosis membrane solutions built to ease these industrial problems. The company is a reverse osmosis membrane manufacturer certified to ISO, CE, and ROHS. Its focus is precision engineering for high-flux, high-rejection elements. The flagship Model MR-BW-8040 is made for brackish water. It pairs a salt rejection rate of 99.5% with an optimized flow of 10,500 GPD. With a standard 34.37m² filtration area, these membranes deliver high-capacity output at a steady operating pressure of 1.55Mpa, which helps bring down the energy footprint of the filtration process.
Here is what these specialized membranes bring to the table technically:
- High-Efficiency Salt Rejection: The MR-BW-8040 holds a 99.5% rejection rate. That gives you steady water quality for boiler feed and industrial process water, even in tough conditions.
- Optimized Energy Consumption: Built to run at 1.55Mpa, this reverse osmosis membrane helps cut the specific energy consumption behind every cubic meter of water produced.
- International Regulatory Compliance: The products carry full ISO, CE, and ROHS certification. They meet the strict safety and environmental rules of the European and South American markets.
- Strong Permeate Flow: These modules are rated at 10,500 GPD. That gives them enough capacity for high-volume water treatment. It also means fewer membrane replacements over time.
- Better Fouling Resistance: The thin-film composite build is made to withstand chemical cleaning cycles and resist organic scaling. That leads to a longer service life for the whole system.
Start by looking closely at your project details. That means feed water chemistry and the recovery rates you need. Procurement teams can review the full technical data sheets and selection charts. From there, they can check whether the membrane fits the pressure vessels and the system layout you already have. Need help estimating permeate quality and energy savings for your local climate and water conditions? Technical consultations are available. In industrial desalination plants, high-surface-area 8040 elements deliver big gains in volumetric efficiency.




Reliable Reverse Osmosis Membrane Solutions from Guangdong Morui
Guangdong Morui Environmental Technology Co., Ltd. started back in 2005. We make water treatment equipment, and as a reverse osmosis membrane supplier, we've focused mainly on reverse osmosis membranes for nearly twenty years. Today, customers across South America, Southeast Asia, Europe, the Middle East, and Africa rely on us for high-performance membrane solutions that take on a wide range of industrial jobs.
We take on tough desalination and purification problems. Our systems pull out contaminants efficiently, a must for any reverse osmosis membrane supplier facing high TDS levels or heavy metals that need to be separated. ISO, CE, and ROHS certifications back our work, so buyers on large infrastructure and industrial projects know we meet international safety and quality standards.
At Morui, quality comes down to numbers. Our MR-BW-8040 reverse osmosis membrane holds a steady 99.5% salt rejection rate and delivers 10,500 GPD of permeate flow at 1.55Mpa. Batch testing and strict quality management help us keep permeate quality consistent and the membrane durable, even in tough conditions.
We support customers worldwide with technical services. That includes remote commissioning, onsite training, and maintenance guidance to prevent fouling and cut energy use. Work with Guangdong Morui, and you get dependable, long-term value for your next water treatment project.

Precision Membrane Engineering for High-Performance Brackish Water Desalination
Industrial Applications
All over the world, industrial water treatment relies on the reverse osmosis membrane. It is the main barrier that keeps process water pure, and for many plants, working with a dependable reverse osmosis membrane supplier is just as important. Guangdong Morui Environmental Technology Co., Ltd builds specialized systems for industries that need very pure water in large volumes.
- Boiler feed water treatment is a must for power plants in the Middle East and Europe, and a reverse osmosis membrane supplier can provide the right membranes to stop scale and corrosion from forming in high-pressure steam systems.
- Industrial Wastewater Reclamation: In manufacturing hubs across Southeast Asia, this process recovers water from textile or electronic rinse operations and meets strict discharge regulations.
- Municipal Brackish Water Treatment: This process turns salty groundwater into drinking water. It helps ease drinking water shortages in dry parts of Africa and South America.
Customer Pain Points and Hurdles by Region
High-capacity water systems have to work in wildly different climates. That is not easy. In the Middle East and Africa, salinity runs high and feed water temperatures swing up and down. Membranes foul fast, and energy use gets too high. In Europe and Southeast Asia, plants must meet ISO, CE, and ROHS rules. Suppliers feel the pressure to show they hit the technical marks. If the solution is not solid, plants face frequent unplanned shutdowns, high labor costs for manual cleaning, and possible regulatory fines when permeate quality is inconsistent.
The Morui Integrated Membrane Solution
Guangdong Morui Environmental Technology Co., Ltd, established in 2005, offers a modular, high-efficiency solution centered around the MR-BW-8040 series. Our approach integrates advanced membrane chemistry with system-level automation to ensure long-term stability. This "Turnkey-Ready" configuration is designed to maximize salt rejection while minimizing the hydraulic footprint, specifically engineered to withstand the challenging feed water conditions of tropical and desert environments.
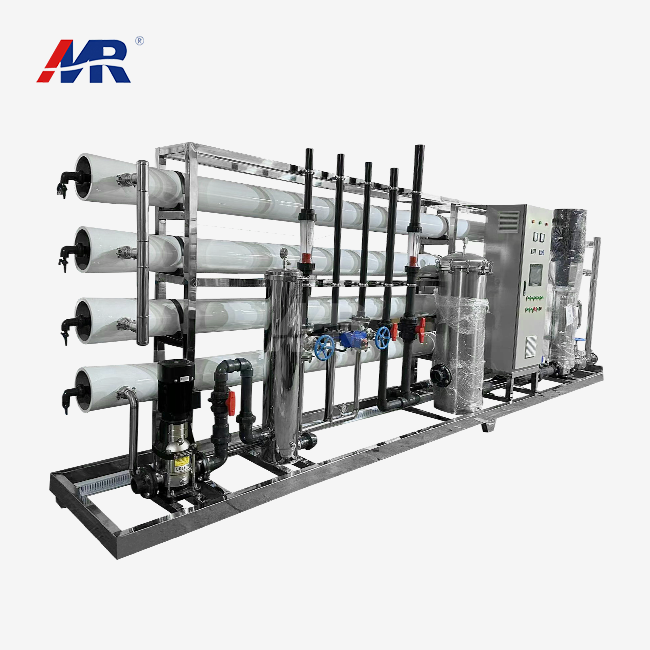
System Layout and Main Components
- Pre-filtration Module: Multi-media and carbon filtration remove suspended solids and chlorine. This protects the polyamide layers inside the RO core. Those layers damage easily.
- MR-BW-8040 Membrane Array: Every element offers 34.37m² of active area. The unit runs at an optimized pressure of 1.55Mpa and puts out a steady 10500 GPD.
- Automated Control System: Built-in PLC/SCADA interfaces track conductivity and trans-membrane pressure (TMP) in real time. As a result, predictive maintenance becomes possible.
- CIP (Cleaning-In-Place) Unit: This separate module handles chemical cleaning. It brings flux back up and holds the 99.5% salt rejection rate steady, with no need to take the pressure vessels apart.
Measurable Benefits and Strategic Gains
- Better Permeate Quality: Rejection stays at 99.5%, so TDS levels remain very low. That counts for sensitive industrial processes.
- Lower Energy Use: Specific energy consumption (SEC) can drop by up to 15% at 1.55 MPa, compared with standard high-pressure membranes.
- High Throughput: One MR-BW-8040 element delivers 10,500 GPD. That shrinks system footprints and lowers capital expenditure.
- Regulatory Peace of Mind: Full compliance with CE and ISO certifications ensures seamless integration into regulated European and South American markets.
Implementation and Service Capabilities
Since 2005, our engineering teams have refined a lean process for deploying systems. It centers on water analysis for each site, custom membrane selection, and commissioning onsite. For customers in South America and the Middle East, we provide full remote diagnostic support and a guaranteed spare parts supply chain. That keeps downtime to a minimum.
Typical Application: Brackish Water Desalination
A textile plant in Southeast Asia had groundwater that was high in minerals. It needed a high-rejection system to treat it. With a multi-stage array of MR-BW-8040 membranes, the plant hit a steady recovery rate of 75%. Permeate TDS stayed below 20 ppm. The modular design cut four weeks off the installation period. The automated CIP system extended membrane life by 25%.
Advanced thin-film composite technology supports high-flux permeate production. It also keeps a strong barrier against dissolved inorganic solutes.
FAQs
1. How can I determine the most suitable reverse osmosis membrane for high-capacity industrial water treatment?
Selecting the right reverse osmosis membrane requires balancing permeate flow, salt rejection, and energy consumption. For high-demand industrial applications, a model like the MR-BW-8040 is often preferred due to its large effective filtration area of 34.37m² and a high flow rate of 10,500 GPD. When evaluating options, you should prioritize a salt rejection rate of at least 99.5% to ensure the removal of dissolved solids and contaminants. We recommend verifying three key parameters: the specific feed water TDS (Total Dissolved Solids), the required operating pressure (typically around 1.55Mpa for brackish water), and the recovery rate targets of your system. As a professional manufacturer since 2005, Guangdong Morui Environmental Technology Co.,Ltd suggests providing your raw water analysis report so our engineers can simulate the optimal membrane configuration for your facility.2. What are the critical factors that influence the lifespan and performance of a reverse osmosis membrane?
The longevity of a reverse osmosis membrane depends heavily on chemical compatibility, operating temperature, and fouling prevention. High temperatures may increase permeate production but can accelerate membrane fouling, while chlorine or heavy metals can degrade the thin-film composite (TFC) layers. To maximize efficiency, you should: 1) Implement robust pretreatment using sediment and activated carbon filters; 2) Maintain consistent operating pressure within the manufacturer’s specifications, such as 1.55Mpa; and 3) Conduct regular chemical cleanings (CIP) to remove biofilm or scale buildup. At Guangdong Morui, our membranes are engineered to withstand diverse industrial conditions, but maintaining stable flux and rejection rates requires adherence to these operational protocols. If you notice a significant drop in permeate quality, contact our technical team to discuss specialized antiscalant dosing or system adjustments.3. For water treatment projects in Southeast Asia and the Middle East, how do your membranes handle high salinity and high temperature conditions?
Water treatment in regions like the Middle East and Southeast Asia often faces challenges such as high source water salinity and elevated ambient temperatures, which can increase the risk of scaling and organic fouling. Our reverse osmosis membrane series, specifically the MR-BW-8040, is designed to maintain a high salt rejection rate of 99.5% even under these demanding conditions. To ensure stable performance, we recommend: 1) Utilizing high-rejection TFC membranes that offer better thermal stability; 2) Adjusting the feed pressure to compensate for osmotic pressure changes caused by high TDS; and 3) Using specialized spacers to reduce pressure drops across the pressure vessel. Guangdong Morui has extensive experience supplying projects in these regions, ensuring our products meet the durability standards required for tropical and arid climates.4. What international certifications should I look for when sourcing a reverse osmosis membrane for the European or South American markets?
When exporting to markets like Europe or South America, quality assurance and regulatory compliance are paramount for verifying a supplier's credibility. A reliable reverse osmosis membrane should carry recognized certifications such as ISO 9001 for quality management, alongside CE and ROHS for safety and environmental standards. These certifications demonstrate that the manufacturer adheres to strict production protocols and material safety requirements. Generally, compliance involves meeting specific directives for pressurized equipment and hazardous substance restriction, though you should always confirm specific local import regulations with your regional authorities. Guangdong Morui Environmental Technology Co.,Ltd maintains ISO, CE, and ROHS certifications, ensuring our MR-BW-8040 and other models meet the rigorous safety and performance benchmarks required for international distribution and large-scale government tenders.5. How can I verify the authenticity and production capacity of a reverse osmosis membrane supplier like Guangdong Morui?
To verify the strength of a supplier, you should look for established industry experience, physical manufacturing capabilities, and transparent technical specifications. Guangdong Morui Environmental Technology Co.,Ltd was established in 2005, providing nearly two decades of expertise in the water treatment sector. When vetting a partner, request detailed product data sheets—such as our MR-BW-8040 specs featuring 10,500 GPD flow and 99.5% salt rejection—and ask for evidence of international project references in regions like Africa or Southeast Asia. We encourage potential clients to review our ISO-certified production processes and schedule a virtual factory tour to inspect our quality control labs. For large-scale procurement, our team can provide localized technical support and customized membrane solutions tailored to your specific project parameters.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.