



Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
edi purified water system supplier
Advanced EDI Purified Water Systems for High-Resistivity Industrial Applications
For procurement managers in South America, Southeast Asia, Europe, the Middle East, and Africa, buying a dependable EDI purified water system is a key step - and picking the right edi purified water system supplier can make that process much smoother. It helps keep high-precision manufacturing processes stable. An EDI purified water system relies on electrodeionization. That technology combines ion-exchange membranes with an electrical current. It deionizes water continuously, and it doesn't need hazardous chemicals for regeneration. Today, this is the main way to make ultrapure water (UPW). It has replaced traditional ion exchange beds, which need frequent downtime and chemical handling.
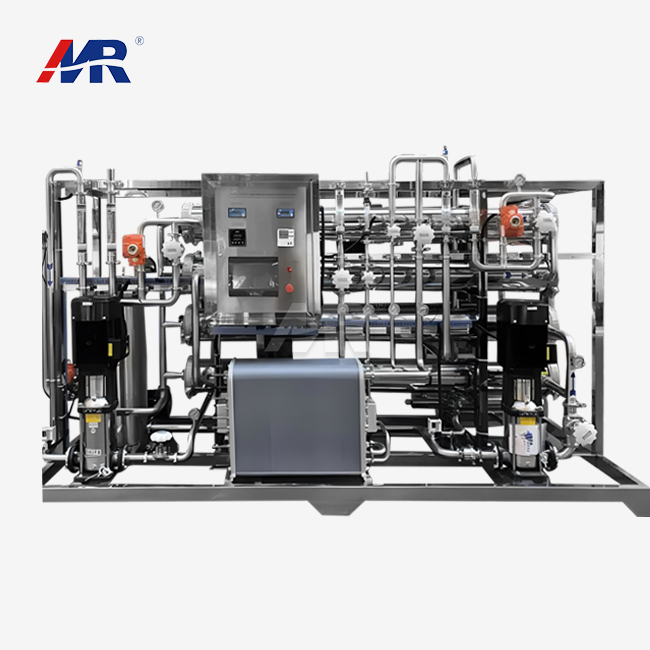
Industrial plants across different regions often hit major operational snags when managing ultrapure water production. In South America and Southeast Asia, shifting raw water quality and high humidity can throw off the stability of deionization modules. That, in turn, leads to inconsistent water resistivity. In Europe and the Middle East, operations have to comply with strict environmental rules on chemical waste discharge, while energy costs keep climbing, which drives up the total cost of ownership. Procurement teams often find it hard to verify the technical authenticity of edi purified water system supplier offerings. They also deal with long lead times, missing ISO/CE certification, and weak technical documentation for complex water treatment projects.
Guangdong Morui Environmental Technology Co.,Ltd was founded in 2005. The company provides specialized EDI purified water system solutions built to handle these global challenges. Our know-how shows in the MR-EDI-2TH model. It is designed for ultrapure water production in electronics, pharmaceuticals, and power generation. As an experienced EDI purified water system manufacturer, we focus on modular designs that make installation and maintenance easier in remote regions. With high-rejection membranes and optimized electrical stacks, our solutions deliver a continuous supply of high-resistivity water and meet international safety and environmental standards.
- Exceptional Deionization Performance: The MR-EDI-2TH model delivers a salt rejection rate of 99.99%, ensuring the high-purity output required for the most sensitive industrial water treatment applications.
- Energy-Efficient Operation: Designed with a power consumption of 8.5kw/hour, this edi purified water system reduces operational expenses for facilities in energy-sensitive markets like Europe and Africa.
- International Compliance Standards: Our manufacturing processes are ISO-certified, and all edi purified water system solutions carry CE and ROHS marks to ensure regulatory alignment across Southeast Asia and the Middle East.
- Sustainable Resource Management: With a recovery rate of 55%, the system maximizes water yield while eliminating the need for acid and caustic regeneration chemicals.
- Proven Industrial Reliability: Drawing on nearly two decades of engineering experience, our systems are built to withstand diverse environmental conditions while maintaining stable resistivity levels.
Detailed technical specifications and site-specific configuration guides are available to assist engineering teams in evaluating the compatibility of the MR-EDI-2TH with existing pre-treatment infrastructures. A thorough review of system flow diagrams and membrane performance data can facilitate the selection of the most efficient deionization setup for specific regional water chemistries.
The MR-EDI-2TH model provides a stable and chemical-free ultrapure water supply through a high-precision electrodeionization process that minimizes environmental impact and maintenance requirements.
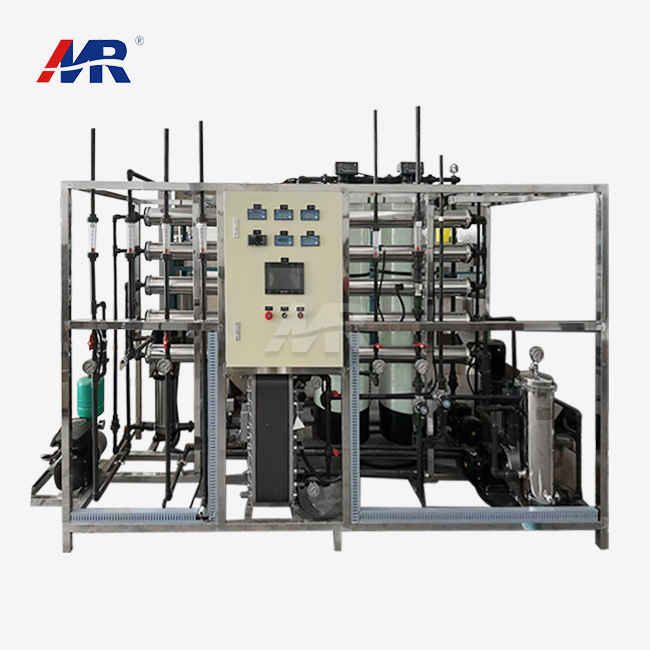




Trusted Manufacturer of EDI Purified Water Systems
Guangdong Morui Environmental Technology Co.,Ltd got its start back in 2005. We build high-performance EDI purified water systems. For nearly two decades, we've been a edi purified water system supplier in water treatment. Our advanced filtration technology now serves customers in South America, Southeast Asia, Europe, the Middle East, and Africa.
We're focused on making ultrapure water in a sustainable way, with no chemicals. The MR-EDI-2TH is a great example of what an edi purified water system supplier can deliver. It's built for precision. Salt rejection sits at 99.99%, and recovery is 55%. Plus, it runs on just 8.5kw/hour. That low power draw helps industrial plants bring down their total cost of ownership. And they still meet the strict resistivity standards that electronics and pharma work demands.
ISO, CE, and ROHS certifications back our quality claims. Every EDI purified water system goes through tough testing at our factory, so it meets international performance benchmarks. We also offer full technical support, from remote debugging to on-site training. That way, our partners can run the equipment smoothly, no matter where they are.
Work with Morui and you get a dependable, long-term supply of ultrapure water. We stay focused on moving water treatment technology forward to meet the changing needs of industrial infrastructure around the world.

Integrated EDI Ultrapure Water Solutions for High-Performance Industrial Manufacturing
Application Scenarios in Modern Industry
EDI purified water systems are essential in high-precision manufacturing because they deliver ultra-low conductivity water with outstanding stability. In pharmaceutical production, EDI has become the go-to method for generating Water for Injection (WFI) and for cleaning sterile equipment. Microelectronics and semiconductor plants across Europe and Southeast Asia depend on a reliable edi purified water system supplier for the high-resistivity water used in wafer rinsing, where even trace ionic contamination can significantly cut yields. In the Middle East and Africa, power plants use EDI as the final polishing step for high-pressure boiler feed water, which prevents turbine scaling and corrosion.
Regional Challenges and Operational Pain Points
Source water in South America and Southeast Asia changes frequently, and industrial operators constantly deal with the fallout. Traditional deionization systems are battered by that variability, which is why many turn to an edi purified water system supplier for a more resilient setup.
- Europe and South America enforce strict environmental rules, including ROHS and local wastewater discharge limits. Conventional ion exchange (IX) needs hazardous acids and caustics for regeneration. That creates a toxic effluent stream that's expensive to treat and neutralize.
- Operational costs and downtime are high. Where labor is expensive or technical skills are scarce, manual chemical handling and batch processing in IX resin beds cause frequent downtime. Poor regeneration control triggers water quality swings that can put entire production batches at risk.
- Energy and resource scarcity is a major concern. In the Middle East and Africa, water recovery and energy efficiency are top priorities. High reject rates or excessive power use directly affect total cost of ownership and sustainability goals.
The Morui EDI Solution Strategy
Guangdong Morui Environmental Technology Co.,Ltd, established in 2005, provides a modular and automated approach to ultrapure water production. Our solution replaces the chemical-intensive regeneration process with a continuous, electrically driven separation technique. By integrating the MR-EDI-2TH model into a comprehensive treatment train, we offer a "plug-and-play" turnkey solution that ensures a footprint-optimized system capable of meeting ISO and CE standards. Our approach focuses on stabilizing output quality regardless of feed fluctuations, ensuring a constant supply of ultrapure water with zero chemical handling.
System Architecture and Key Components
The Morui solution is organized into high-efficiency functional blocks designed to withstand harsh environments.
- An advanced pre-treatment unit uses multi-stage filtration and high-rejection reverse osmosis (RO) to remove most dissolved solids. This keeps the feed water entering the EDI module within optimal parameters.
- The MR-EDI-2TH Core Module is a high-performance stack. It uses a continuous electrodeionization process to hit a 99.99% salt rejection rate. It produces ultrapure water at a 55% recovery rate, balancing product water against waste.
- Intelligent power management: the system runs at a precise 8.5 kW/hour. An automated PLC interface monitors resistivity and flow in real time to keep it at peak efficiency.
- Automated maintenance suite: integrated Cleaning-In-Place (CIP) systems let you perform periodic maintenance without taking the membrane stacks apart. That substantially reduces labor intensity.
Strategic Advantages and Quantifiable Benefits
- Since it runs chemical-free, you don't need bulk chemical storage or neutralization systems. This lowers environmental risk and compliance costs.
- Water quality stays above 15-18 MΩ·cm with 99.99% salt rejection, so critical processes get the reliability they need.
- The optimized electrochemical design keeps power draw at 8.5kw/hour, a significant drop in utility costs compared to older thermal or chemical systems.
- Unlike batch resin systems, EDI runs 24/7 with no regeneration downtime. That boosts total plant uptime by 15–20%.
- Compact Footprint: The modular design uses up to 60% less space than traditional ion exchange towers, which lets it fit easily into existing facilities.
Global Implementation and Service Capability
Guangdong Morui Environmental Technology Co.,Ltd has nearly 20 years of experience serving clients in the Middle East, Africa, and Southeast Asia. Before we design a system, we carry out site surveys and water quality analysis. We then run factory acceptance tests (FAT) to confirm CE and ROHS compliance. Our global logistics network gets spare parts to you quickly. Our technical team provides remote diagnostics and on-site training, helping local operators maintain long-term system performance and reliability.
Typical Application Case
A large-scale chemical processing plant in Southeast Asia transitioned from traditional IX beds to the Morui MR-EDI-2TH system to meet rising environmental standards. Prior to the upgrade, the client faced high costs for acid/alkali procurement and frequent production halts. After implementing our modular EDI solution, the facility achieved a continuous flow of ultrapure water with a stable 99.99% rejection rate. This transition resulted in a 30% reduction in annual maintenance costs and completely eliminated the need for hazardous chemical handling on-site.
The MR-EDI-2TH system delivers a reliable and sustainable path to ultrapure water through high salt rejection and optimized energy consumption for modern industrial applications.
FAQs
1. What is an edi purified water system and how does it compare to traditional ion exchange methods?
An EDI (Electrodeionization) purified water system is an advanced water treatment technology that combines ion-exchange membranes and resin with an electrical current to remove impurities. Unlike traditional ion exchange (IX) systems that require periodic downtime and hazardous chemicals like acid and caustic for resin regeneration, an EDI system operates continuously and chemical-free. This makes it an environmentally friendly and cost-effective solution for industries requiring ultrapure water. At Guangdong Morui Environmental Technology Co.,Ltd, we have refined this technology since 2005 to solve common industry pain points such as high operational costs and wastewater disposal issues. By integrating an EDI module after a Reverse Osmosis (RO) system, you can achieve consistent water quality with a significantly smaller physical footprint. For facilities prioritizing sustainability and safety, transitioning to EDI technology is the recommended standard for modern high-purity water production.2. How do I select the right edi purified water system model for my facility's specific requirements?
Choosing the correct system involves evaluating several technical parameters to ensure the output meets your ultrapure water standards. You should primarily focus on the salt rejection rate, recovery rate, and power efficiency. For instance, our Model MR-EDI-2TH is engineered for high-performance ultrapure water production, featuring a remarkable salt rejection rate of 99.99% and a recovery rate of 55%. These specifications ensure that mineral content is virtually eliminated while maintaining a balanced water yield. Additionally, consider the energy footprint; our systems are designed to be efficient, with the MR-EDI-2TH consuming approximately 8.5kw/hour. We suggest assessing your daily volume needs and feed water quality before selection. If you are unsure which configuration fits your workflow, the experts at Guangdong Morui can provide a customized technical proposal based on your specific project parameters and local water conditions.3. For projects in Southeast Asia or the Middle East, what are the critical pre-treatment requirements for an edi purified water system?
In regions like Southeast Asia or the Middle East, source water often contains high levels of hardness, silica, or total dissolved solids (TDS), which can lead to scaling and fouling within the EDI module. To protect your edi purified water system, a robust Reverse Osmosis (RO) pre-treatment stage is mandatory. The RO system acts as a barrier, removing the bulk of the ionic load so the EDI unit can focus on "polishing" the water to ultrapure levels. We recommend monitoring the Feed Water Conductivity (typically preferred below 40 µS/cm) and ensuring the removal of free chlorine and CO2, which can impact the efficiency of the ion-exchange resin. Since environmental conditions vary, Guangdong Morui suggests a comprehensive water analysis report before installation. Our systems are designed to withstand diverse climates, but local pre-filtration adjustments are essential to maximize the 99.99% salt rejection capability of our modules.4. What international certifications should I verify when sourcing an edi purified water system for the European or South American markets?
When importing high-tech water treatment equipment to Europe or South America, verifying international certifications is crucial for ensuring both safety and legal compliance. You should look for CE marking, which indicates conformity with health, safety, and environmental protection standards for products sold within the European Economic Area. ROHS compliance is also vital, as it restricts the use of specific hazardous materials in electrical and electronic equipment. Furthermore, ISO 9001 certification demonstrates that the manufacturer, such as Guangdong Morui Environmental Technology Co.,Ltd, adheres to rigorous quality management systems. These certifications serve as a benchmark for reliability and manufacturing excellence. While these standards are globally recognized, we advise clients to check if there are additional local municipal regulations or industry-specific standards (such as pharmacopeia standards for medical use) required for your specific project site in South America or Europe.5. Does Guangdong Morui provide technical support and installation guidance for EDI projects located in Africa or Southeast Asia?
Yes, supporting international clients across Africa, Southeast Asia, and beyond is a core part of our service. Since our establishment in 2005, we have developed a streamlined support system to assist with the deployment of our edi purified water system technology. While we provide comprehensive technical manuals and remote video commissioning support, we can also coordinate onsite technical guidance for large-scale industrial projects depending on the region. Our engineers focus on training your local team on essential operational tasks, such as monitoring the 8.5kw/hour power consumption and maintaining the 55% recovery rate to ensure long-term system health. We recommend establishing a preventative maintenance schedule early in the project. If you are planning a project in these regions, please contact our technical department with your raw water specifications so we can ensure the system design is optimized for your local infrastructure and environmental conditions.
Best Selling Products






Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.