

Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
100m3/hour reverse osmosis equipment supplier
100m3/hour Reverse Osmosis Equipment, Verified for Industrial Desalination
Buyers in South America, Southeast Asia, Europe, the Middle East, and Africa often need a water treatment system that can hold steady at high capacity. A 100m3/hour reverse osmosis system is a big purchase for them, so choosing a dependable 100m3/hour reverse osmosis equipment supplier can make the decision a lot easier. This is industrial-scale technology, and in large water treatment plants it handles the main filtration stage. Semi-permeable membranes do the work, pulling dissolved solids and contaminants out of brackish or underground sources.
Operators in places like Southeast Asia and Africa deal with some really tough problems on the job. Raw water quality keeps changing. Energy costs stay high. And finding a 100m3/hour reverse osmosis equipment supplier with technical credentials you can actually verify isn't easy. They also need to meet international safety standards, keep power use under control on high-flux systems, and get long-term technical support for complex desalination work. Get the system design wrong, and a facility can end up with relentless membrane scaling, unexpected downtime, and hefty maintenance bills. Any one of those can put an entire production line at risk.
Guangdong Morui Environmental Technology Co., Ltd has been operating since 2005. We meet these challenges with engineered 100m3/hour reverse osmosis equipment made for harsh underground water conditions. Our Model: MR-BWRO-100TH is built for underground water desalination. It combines industrial-grade durability with precise control systems. Nearly two decades of expertise sit behind it. Our ISO, CE, and ROHS certifications show how we handle quality. We also give procurement teams the transparency and technical depth to check what a supplier can do. These systems handle the varied climates of South America and the Middle East. High-grade materials and automated monitoring keep performance steady.
Several technical strengths set the MR-BWRO-100TH system apart:
- Strong desalination performance. Made specifically for underground water applications. Salt rejection holds at a steady 98%, and the output is high purity.
- Energy efficiency you can verify. The system runs at 105kw/hour. For large-scale 100m3/hour reverse osmosis equipment, it balances energy input against permeate volume.
- Compliance for global markets. Every unit is made under ISO quality management and meets CE and ROHS requirements. That helps them fit into European and South American industrial frameworks.
- Recovery tuned for output: run the system at 55-60% recovery and it makes as much water as possible. Pressure holds steady across the membrane modules.
- Reliability for industrial use: Our engineers have improved how we apply corrosion-resistant parts since 2005. That work helps the system stay stable long term in high-TDS conditions.
When a project has special technical requirements, your engineering department can review detailed performance data and system configuration charts. Technical consultations center on matching the influent water analysis to the right membrane setup. The aim is an installation that lasts.
For industrial desalination, the MR-BWRO-100TH reaches 98% salt rejection and 55-60% recovery. It runs on an energy-efficient 105kw/hour power configuration.
Related Products
About Guangdong Morui Environmental Technology Co., Ltd.
Founded in 2005, Guangdong Morui Environmental Technology Co., Ltd. is a leading global manufacturer focused on advanced industrial water treatment solutions. We bring nearly two decades of engineering expertise and, as a 100m3/hour reverse osmosis equipment supplier, a strong presence across South America, Southeast Asia, Europe, the Middle East, and Africa. That makes us a trusted partner for high-capacity 100m3/hour reverse osmosis equipment.
Our technical strength is clear in the MR-BWRO-100TH model, which is built for large-scale underground water desalination. It is designed to run 24/7 in industrial operation and delivers a stable 98% salt rejection rate and a 55-60% recovery rate. We use automated PLC controls and corrosion-resistant materials such as SS316L and FRP, and as a 100m3/hour reverse osmosis equipment supplier, we make sure our systems meet the strict demands of international infrastructure and industrial projects.
Quality and compliance are at the center of how we work. Our manufacturing processes are certified under ISO, CE, and ROHS standards. To support customers around the world, Morui offers complete technical services, including remote commissioning, on-site training, and specialized maintenance support tailored to the environmental conditions of our target markets. Investing in Morui's 100m3/hour reverse osmosis equipment gives you long-term operational stability and high-performance water purification for your most critical assets.
Industrial Desalination and Water Treatment You Can Rely On at 100m3/hour
How Industries Around the World Use These Systems
Large water treatment plants help keep industry stable and meet municipal demand. A 100m3/hour reverse osmosis system from a trusted 100m3/hour reverse osmosis equipment supplier is built for high-volume work in sectors such as:
- Large-Scale Manufacturing: Delivers high-purity process water to electronics and textile plants. That's where a 100m3/hour reverse osmosis equipment supplier comes in, helping stop equipment scaling and keep products free from contamination.
- Municipal Water Supply: Removes salt from underground water for homes in remote parts of Southeast Asia and Africa.
- Power Generation: Supplies high-quality boiler feed water. This helps plants reach peak thermal efficiency and reduce maintenance intervals.
Major Challenges and Regional Pain Points
High-capacity water systems face unique challenges in regions as different as South America, the Middle East, and Europe:
- High Energy Costs: Where power is expensive, a system that runs inefficiently pushes operating costs to levels that just don't hold up. That 105kw/hour draw has to be reined in, and better hydraulics are how you do it.
- Strict Regulatory Compliance: Buyers in Europe and South America expect you to meet ISO, CE, and ROHS standards in full. Those rules speak to two things: environmental safety and equipment quality.
- Harsh Feedwater Conditions: Groundwater in much of the Middle East carries high TDS. Membranes foul fast under those conditions, and the downtime that follows is never on anyone's schedule.
- Maintenance Logistics: Sites far from anywhere mean costly labor and long waits for spare parts. Reliability settles the question.
Guangdong Morui's Plan for 100m3/hour
Guangdong Morui Environmental Technology Co.,Ltd has been in business since 2005, and its answer to these problems is the MR-BWRO-100TH model. The company supplies more than hardware. It delivers a turnkey modular system built to go in fast and run steadily over the long haul. That setup takes raw underground water and brings it up to high-purity industrial standards, holding performance steady even where salinity runs high.
System Layout and Technical Setup
The system splits into separate functional modules, all laid out to keep uptime as high as it can go:
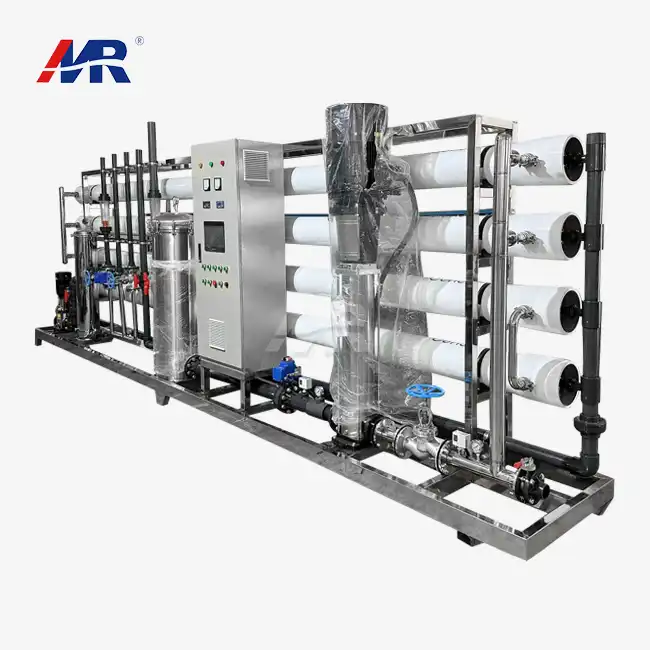
- Advanced Pre-treatment Unit: Multi-media and activated carbon filters remove suspended solids and chlorine. That keeps the RO membranes from degrading too soon.
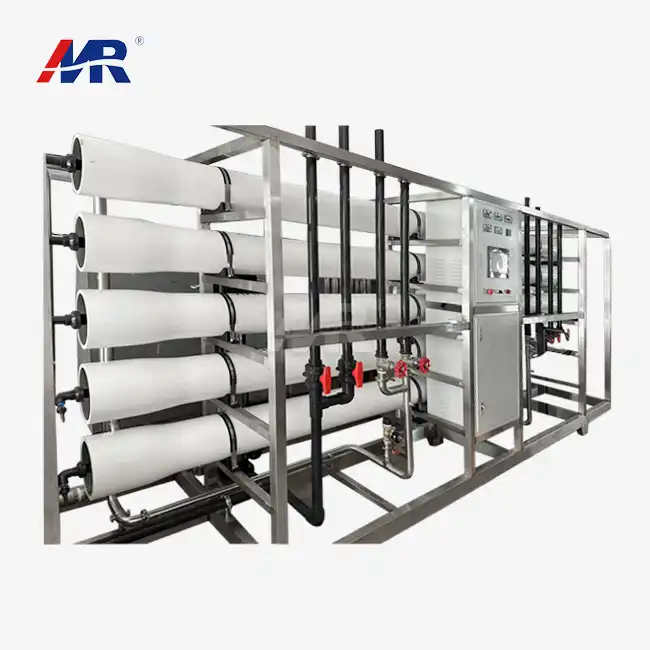
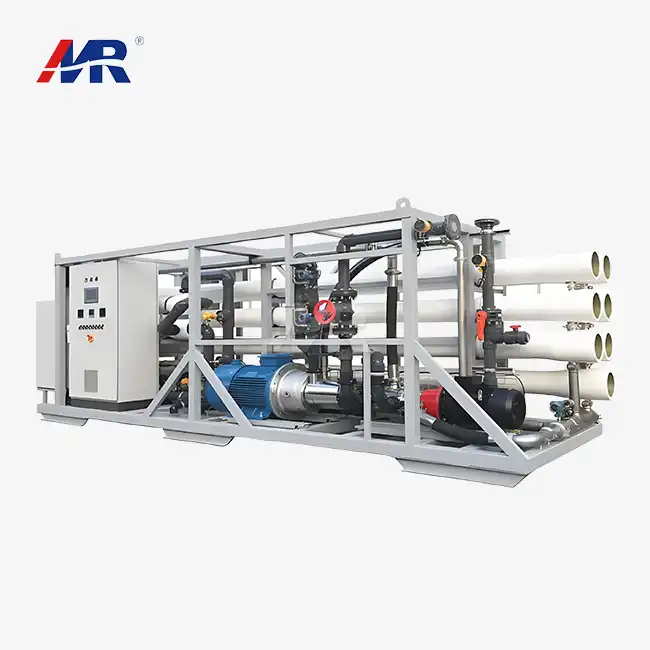
- MR-BWRO-100TH Mainframe: The high-efficiency membrane arrays deliver a 98% salt rejection rate and maintain a steady 55-60% recovery rate. The system is tuned for desalinating underground water.
- Automated Control Center: Integrated PLC and HMI systems track flux and conductivity in real time. That keeps power consumption at 105kw/hour within the design limits.
- Integrated CIP (Clean-In-Place) Module: This dedicated chemical cleaning system cuts down on manual work and helps pressure vessels last longer.
Benefits You Can Measure and Strategic Advantages
- High Salt Rejection: Dissolved solids drop by 98%, so the water meets strict industrial and potable water standards.
- Certified Quality: It fully meets ISO, CE, and ROHS requirements. That makes it legally and technically fit for markets in Europe and the Middle East.
- Optimized Energy Efficiency: The 105kw/hour power profile balances high-pressure needs against operating costs, so they stay sustainable.
- Stable High Output: Designed for 24/7 operation. Permeate flow stays steady at 100m3/hour.
- Scalable Modular Design: Cuts installation time by up to 30% compared with traditional on-site construction.
Worldwide Deployment and Service Support
Each project includes site analysis, custom hydraulic design, and factory FAT (Factory Acceptance Testing). For clients in South America, Southeast Asia, and Africa, the service framework also adds remote diagnostic support and a standard spare parts kit. That helps lower the risk of supply chain delays.
Example of an Industrial Project
In the Middle East, a large agricultural project needed 100m3/hour of irrigation water from high-salinity boreholes. The site installed the MR-BWRO-100TH system. Groundwater TDS fell to levels safe for crops, and the system kept a steady 58% recovery rate. That cut raw water waste by a significant margin.
Assessment and Engineering Consultation
Technical specs and a site-specific configuration report are available once you provide a raw water analysis and target purity requirements. Case studies from similar 100m3/hour installations give you a clear view of long-term performance and lifecycle costs.
Industrial reverse osmosis systems are designed to take salt out of water, and they do it reliably. They work well for large-scale purification in tough conditions.
FAQs
1. What are the primary technical considerations when selecting a 100m3/hour reverse osmosis equipment for industrial desalination?
When scaling up to a capacity of 100m3/hour, the balance between energy efficiency and water recovery is critical. For a system like the Guangdong Morui MR-BWRO-100TH, designed specifically for underground water desalination, you should focus on the recovery rate—typically 55-60%—and the salt rejection rate, which should be at least 98% to ensure high-purity output. Additionally, assess the power consumption; our 100m3/hour reverse osmosis equipment operates at approximately 105kw/hour. It is also vital to verify the supplier’s manufacturing history; Guangdong Morui has been specializing in water treatment since 2005, ensuring that the modular design and PLC automation are refined for 24/7 industrial loads. We recommend providing your raw water TDS (Total Dissolved Solids) report to our engineers to optimize these parameters for your specific site.2. How can I verify the reliability and certification of a 100m3/hour reverse osmosis equipment supplier for international projects?
For large-scale investments in regions like Europe, South America, or the Middle East, supplier credibility is paramount. A reliable manufacturer must hold international certifications such as ISO 9001 for quality management, alongside CE and ROHS for electrical and environmental safety. Guangdong Morui Environmental Technology Co., Ltd. maintains all three certifications, reflecting nearly two decades of industry expertise since our establishment in 2005. When evaluating equipment, look for high-grade materials like SS316L or FRP (Fiber Reinforced Plastic) and industrial-grade components that can withstand high operating pressures. We invite potential clients to request our factory audit reports and performance case studies from Southeast Asia and Africa to validate the long-term stability and salt rejection efficiency of our 100m3/hour reverse osmosis equipment.3. For water treatment projects in Southeast Asia and Africa, how does the 100m3/hour reverse osmosis equipment handle high-salinity underground water?
In regions like Southeast Asia and Africa, underground water often contains high levels of dissolved salts and minerals that can cause membrane scaling. The MR-BWRO-100TH model is engineered with a robust 98% salt rejection rate to effectively transform brackish underground water into high-quality process water. To maintain a recovery rate of 55-60% in these environments, we incorporate advanced pre-treatment stages and automated flushing cycles. The 105kw/hour power consumption is optimized for large-scale output, ensuring that the cost-per-cubic-meter remains competitive. If your project site experiences fluctuating water quality, Guangdong Morui suggests installing real-time conductivity monitoring. We provide customized technical configurations to ensure the 100m3/hour reverse osmosis equipment meets local industrial standards while protecting downstream assets from mineral buildup.4. What international standards and regulations apply to 100m3/hour reverse osmosis equipment in European and Middle Eastern markets?
Exporting large-scale 100m3/hour reverse osmosis equipment to Europe or the Middle East requires strict adherence to safety and environmental regulations. Typically, this involves CE marking for electrical components and compliance with ROHS directives to ensure no hazardous substances are used in manufacturing. While ISO standards cover general production quality, specific regions may have unique water discharge or pressure vessel regulations (such as ASME or PED). At Guangdong Morui, our equipment is built to these global benchmarks to facilitate smoother customs clearance and local installation. However, since regulations can vary by country, we recommend consulting with our technical team to confirm that the equipment configuration aligns with your local environmental and safety codes before shipping.5. Does Guangdong Morui provide on-site installation and technical support for 100m3/hour reverse osmosis equipment in remote regions?
Yes, Guangdong Morui Environmental Technology Co., Ltd. provides comprehensive global support for our 100m3/hour reverse osmosis equipment. Recognizing that projects in South America, Africa, and the Middle East may be in remote locations, we design our systems with a modular approach to simplify shipping and assembly. Our equipment features an integrated PLC (Programmable Logic Controller) with a user-friendly HMI, allowing for remote monitoring and troubleshooting. For complex installations, we offer field service options where our engineers provide on-site commissioning and staff training. We also maintain a rapid-response spare parts supply chain to ensure your desalination process remains operational. For a detailed installation roadmap tailored to your region’s logistics, please contact our support desk with your project coordinates.
Best Selling Products
Related Blogs
Related Search
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.