
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
2000m3/day ultrafiltration equipment supplier
Industrial Wastewater Management: Reliable Ultrafiltration Equipment at 2000m3/day
If procurement is part of your job and you need reliable ultrafiltration equipment in South America, Southeast Asia, Europe, the Middle East, and Africa, start with two checks: the technical skill and manufacturing scale that a 2000m3/day ultrafiltration equipment supplier brings to the table. That is step one for a successful project. The system is a high-capacity water treatment unit. It acts as a specialized physical barrier. Semi-permeable membranes remove suspended solids, bacteria, and macromolecules from complex industrial streams. In wastewater recycling today, this equipment does critical work. It shields downstream processes from fouling and helps plants meet strict environmental discharge limits.

In Southeast Asia and the Middle East, industrial plants often have to deal with feed water that's variable in quality and high in turbidity. That can lead to early membrane failure. Europe and South America have strict regulations too. Facilities there have to meet ISO and CE standards all the time, which puts a lot of pressure on system reliability. On top of that, many operators struggle with high energy consumption and low recovery rates. Both of these drive up the total cost of ownership. Finding a 2000m3/day ultrafiltration equipment supplier who knows the regional compliance landscape and offers solid after-sales support is often the biggest bottleneck in the procurement process.
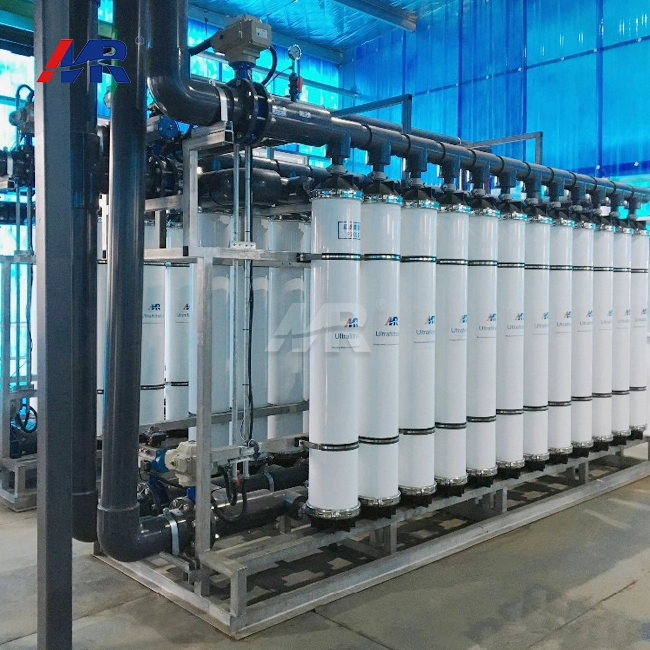
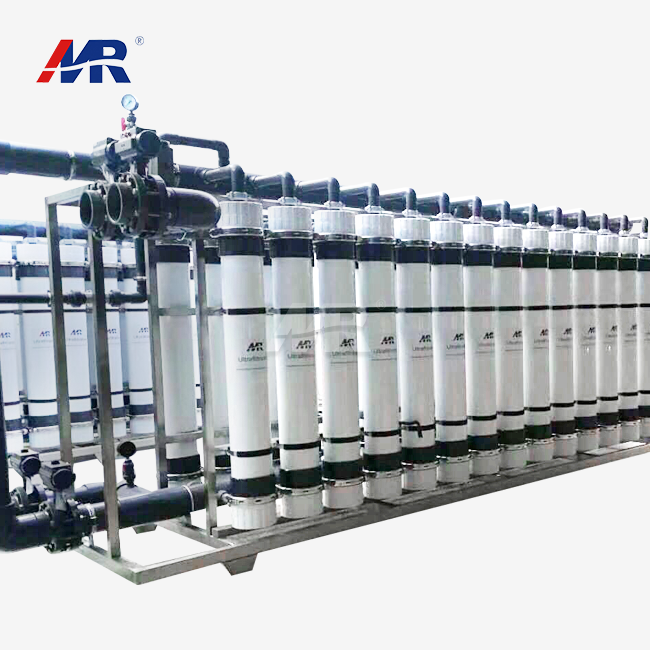
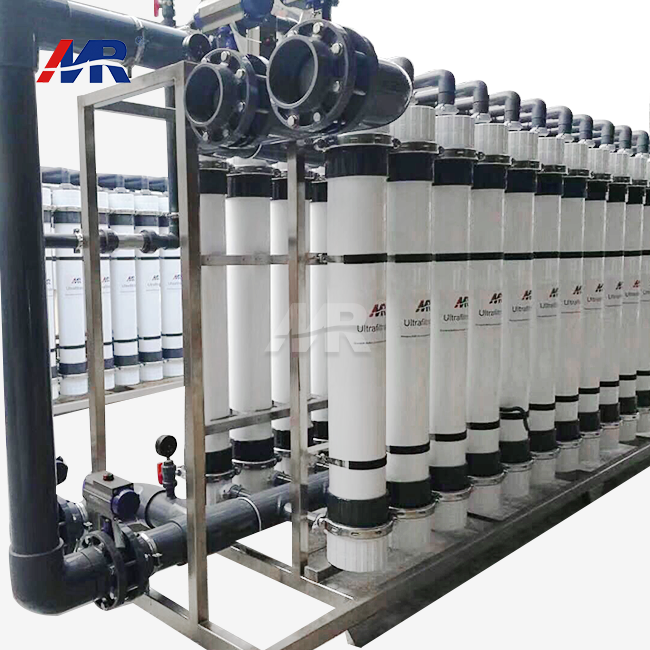
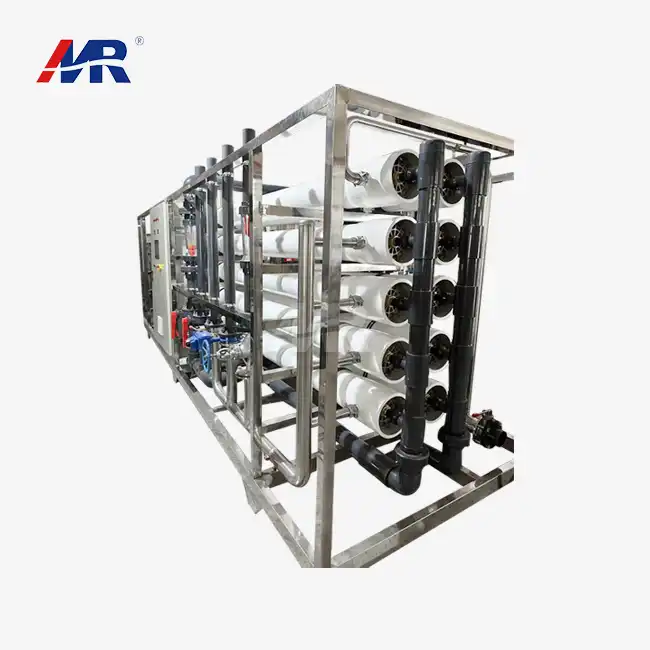
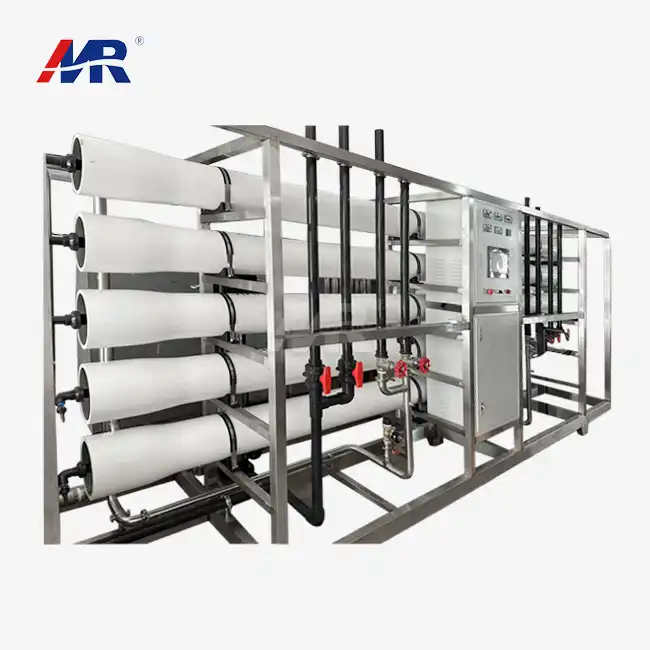
Guangdong Morui Environmental Technology Co.,Ltd has been operating since 2005. The company takes on these industrial challenges with the Model MR-UF-100TH, a high-performance 2000m3/day ultrafiltration system. It is built for industrial wastewater treatment. The design balances high throughput with low operating costs. For markets in Africa and South America, it uses durable materials that hold up in different climates. This 2000m3/day ultrafiltration equipment uses advanced membrane chemistry. That brings long-term stability and high rejection rates for organic pollutants and colloidal matter.
- Optimized Energy Profile: The MR-UF-100TH is built for high-efficiency water treatment and draws only 15kw/hour. Even with that low draw, it still delivers a 2000m3 daily output.
- International Quality Certification: Every unit is built to ISO9001 standards. It also holds CE and ROHS certification. For projects in Europe and beyond, that gives you full compliance.
- High Resource Recovery: This ultrafiltration equipment handles 2000m3/day. It recovers 70-90% of the water. In dry regions like the Middle East, that cuts water waste by a wide margin.
- Low-Pressure Operation: The system runs at an operating pressure of just 0.1-0.3Mpa. Low pressure means less mechanical wear on the membrane modules, so maintenance happens less often.
- Industrial-grade filtration. Size-exclusion technology does the work here, and the result is a filtrate quality that stays consistent. That makes it suitable for RO pretreatment or for direct reuse in industrial operations.
Want to check these technical benchmarks for yourself? Procurement teams can look through our project portfolio across Southeast Asia and Africa. We also provide detailed technical datasheets and P&ID drawings to help you integrate the 2000m3/day ultrafiltration equipment into your existing plant infrastructure. Our engineering consultations give you the data you need to confirm energy savings and flux stability before you commit any capital. The PVDF membrane modules are built for high performance. They act as a physical barrier against contaminants, and they keep energy consumption low in high-volume industrial applications.
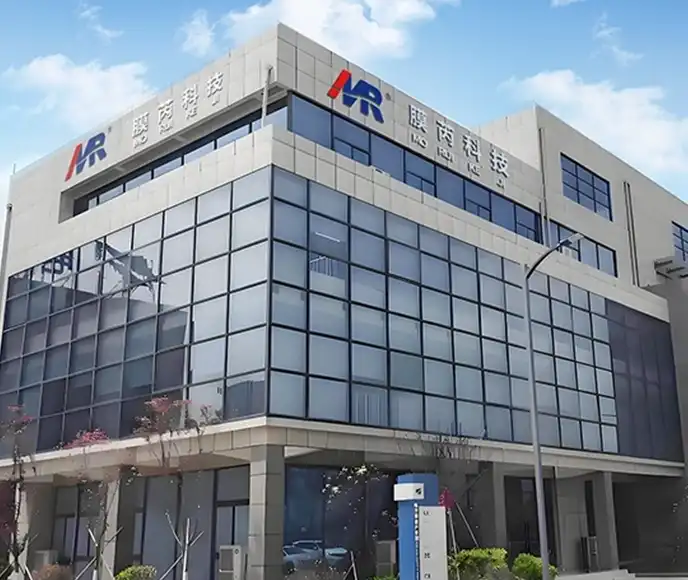
Company overview: Guangdong Morui Environmental Technology Co., Ltd.
Guangdong Morui Environmental Technology Co., Ltd. has been operating since 2005. We're a leading specialist in the global water treatment industry. We provide high-performance membrane separation solutions, and as a 2000m3/day ultrafiltration equipment supplier, we serve large-scale industrial systems. Those systems are our core focus. That includes our 2000m3/day ultrafiltration equipment.
We've worked with complex industrial wastewater sectors in South America, Southeast Asia, Europe, the Middle East, and Africa. Our MR-UF-100TH model, which we offer as a 2000m3/day ultrafiltration equipment supplier, really shows our technical strength. Its advanced PVDF membranes hit a 70-90% recovery rate. These systems are built to last, handle high capacity, and use little energy (15kw/hour). They also serve as a critical physical barrier against suspended solids and bacteria. This keeps RO pretreatment stable and process water safe for international industrial facilities.
Morui follows strict ISO, CE, and ROHS quality management standards. We have a steady track record for reliable delivery and superior rejection performance. Customers worldwide get a full range of technical services. These include remote commissioning, on-site training, and specialized maintenance guidance tailored to diverse regional environmental conditions.
Morui is a trusted partner for large-scale 2000m3/day ultrafiltration equipment projects. We combine two decades of engineering heritage with localized support. That gives you long-term operational success and water security.
Industrial Wastewater Recovery: High-Efficiency Ultrafiltration Systems at 2000 m3/day
Typical Applications
A 2000 m3/day ultrafiltration system, often sourced from a 2000m3/day ultrafiltration equipment supplier, does two things in industrial water treatment. It keeps a plant running without unexpected stops, and it keeps that plant within environmental rules. Most of the time, you'll find one doing a job like this:
- Pre-treatment ahead of RO systems: if you're running a large desalination plant or a boiler feed water plant, picking a dependable 2000m3/day ultrafiltration equipment supplier makes a real difference, since this stage shields the reverse osmosis membranes downstream from colloidal fouling and organic scaling.
- Industrial wastewater recycling: Effluent from textile, electronics, or chemical production is treated until it meets strict reuse standards. That closes the water loop.
- Cooling tower blowdown recovery: Capture the blowdown water, purify it, and you cut costs on both raw water intake and discharge.
Customer Pain Points and Common Hurdles
Large filtration systems run into their own mix of environmental and regulatory obstacles in regions such as Southeast Asia, the Middle East, and South America:
- Strict discharge rules. Europe, South America, and other regions have set tighter limits on suspended solids and bacteria. Break those rules and you could be looking at heavy fines, or a shutdown.
- High energy costs. In many developing markets, water treatment eats up a lot of power. That cuts straight into manufacturing margins.
- Maintenance and downtime risks. When turbidity runs high, or feed water changes often, membranes foul fast. You end up cleaning them with chemicals over and over. Every production stop costs you money.
- Reliability concerns. Buy equipment with no ISO or CE certification, and you put the safety and stability of your long-term infrastructure at real risk.
Guangdong Morui Environmental Technology Co.,Ltd: The Solution
Guangdong Morui Environmental Technology Co.,Ltd has been building its expertise since 2005. The company's modular, high-capacity solution is built around the Model MR-UF-100TH. This ultrafiltration system handles 2000m3/day and comes as a turnkey unit for high-load industrial wastewater. Its footprint is compact, too. The process works by physical separation, using advanced hollow fiber membranes. Those membranes form a physical barrier against contaminants and need very little chemical help.
System Construction and Main Components
- Automated pre-filtration. This stage strips out large particles and debris. That helps the main UF modules last far longer.
- Ultrafiltration host (Model MR-UF-100TH). The membranes run at low transmembrane pressure, between 0.1 and 0.3 MPa. Flux stays high, and performance holds steady over the long run.
- Smart control system (PLC/SCADA). It watches flow rates and pressure differentials in real time. That is what makes unmanned operation possible. And when feed water conditions shift, the system reacts fast.
- Integrated CIP (clean-in-place) module. It handles system maintenance on its own. Chemicals are dosed at set levels to bring membrane permeability back. Nothing has to be taken apart.
Solution advantages, with the numbers to back them up
- Optimized energy efficiency. The system draws only 15 kW/hour. Conventional thermal or high-pressure separation methods use far more.
- High recovery rates. Water recovery lands between 70% and 90%. So operators get more usable water out of every cubic meter of feed.
- Certified quality. Meets ISO, CE, and ROHS standards. The system runs safely and is accepted in markets worldwide.
- Reduced footprint. The modular design processes 2000m3/day in very little space. That makes it a strong fit for retrofitting existing plants.
- Membranes keep working longer. A better backwash routine means less fouling, and that can stretch the replacement cycle by as much as 20%.
How We Run Projects and What Services We Provide
Every project starts with a full water quality analysis. From there, we design a system that fits the site and build it to exact standards. If you're in Africa, the Middle East, or other regions, we back you up with remote diagnostics and a spare parts supply chain you can count on. Our technical teams also handle on-site commissioning and train your staff. That way local operators can run the system with confidence and need very little supervision.
A Real-World Example
A large manufacturing plant in Southeast Asia needed a 2000m3/day system to treat process water with high turbidity. Before the project, the plant was replacing RO membranes often, and water costs ran high. Then they installed the MR-UF-100TH system. Recovery held at 85%, and RO membrane cleaning frequency dropped by 60%. In the first year, total operating costs went down by 25%.
Technical Support and Assistance
Do you want technical specifications, configuration options for your site, or full case reports for the 2000m3/day ultrafiltration equipment? Just ask, and we'll send them. They can help you plan and evaluate the project. A professional engineering assessment also helps pin down the best membrane selection and pre-treatment requirements for specific industrial water chemistries.
Hollow fiber membranes are made to perform. They remove suspended solids and pathogens at a steady rate, and they suit a wide range of industrial wastewater applications.
FAQs
1. How should I select the right 2000m3/day ultrafiltration equipment for my industrial facility?
Selecting a system with a 2000m3/day capacity requires a deep analysis of your feed water quality and specific industrial application. At Guangdong Morui Environmental Technology Co., Ltd., we recommend evaluating the Total Suspended Solids (TSS) and organic load of your influent. For high-volume industrial wastewater treatment, our MR-UF-100TH model is designed to handle these demands efficiently. You should focus on the membrane's Molecular Weight Cut-Off (MWCO) and material compatibility—such as PVDF for better chemical resistance—to ensure the equipment can withstand rigorous cleaning cycles. Since 2005, we have helped clients across Southeast Asia and the Middle East match their flux requirements with the right membrane packing density. We suggest sharing your water analysis report with our technical team to receive a customized configuration.2. What are the primary operational benefits of the MR-UF-100TH 2000m3/day ultrafiltration equipment?
The MR-UF-100TH is engineered for high-efficiency industrial wastewater treatment with a focus on resource recovery and energy savings. This 2000m3/day ultrafiltration equipment achieves a recovery rate of 70-90%, significantly reducing water waste in water-scarce regions like Africa and the Middle East. Operationally, it is highly cost-effective, consuming only 15kw/hour while maintaining a low operating pressure of 0.1-0.3Mpa. This low transmembrane pressure (TMP) not only reduces electricity costs but also minimizes mechanical stress on the hollow fiber membranes, extending their service life. By providing a consistent physical barrier against bacteria and suspended solids, the system ensures stable effluent quality, which is critical for protecting downstream Reverse Osmosis (RO) units from premature fouling.3. Does your 2000m3/day ultrafiltration equipment comply with international standards for South American and European markets?
Yes, Guangdong Morui ensures that our water treatment solutions meet rigorous international quality and safety benchmarks. Our 2000m3/day ultrafiltration equipment is manufactured under ISO-certified processes and carries CE and ROHS certifications, which are essential for entry into European and South American markets. These certifications verify that our electrical components and pressure vessels meet high safety and environmental standards. While our equipment complies with these global frameworks, specific projects may be subject to local environmental regulations regarding discharge quality or structural engineering codes. We recommend consulting with local authorities to confirm site-specific requirements. Our team can provide all necessary technical documentation and certification proof to streamline your local permitting and compliance process.4. How does this ultrafiltration system manage membrane fouling in harsh industrial wastewater environments?
Fouling is the most significant challenge in industrial wastewater treatment, but our 2000m3/day ultrafiltration equipment is designed with multiple mitigation strategies. The system utilizes semi-permeable membranes with pore sizes between 0.001 and 0.1 μm to physically block contaminants. To maintain performance, the MR-UF-100TH incorporates automated backwashing and Chemical Enhanced Backwash (CEB) protocols. By operating at a stable pressure of 0.1-0.3Mpa, the system prevents the deep compaction of solids into the membrane pores. In regions with high ambient temperatures or specific mineral content, such as Southeast Asia or the Middle East, we may recommend specific chemical cleaning agents. Regular monitoring of the transmembrane pressure is vital; we suggest a professional maintenance schedule to ensure the system operates at peak efficiency for many years.5. What technical support and installation services are available for projects in Southeast Asia, Africa, and the Middle East?
Guangdong Morui Environmental Technology Co., Ltd. provides comprehensive technical support for all international installations of our 2000m3/day ultrafiltration equipment. For large-scale projects in Southeast Asia, Africa, and the Middle East, we offer detailed installation manuals, P&ID drawings, and remote commissioning support via video conferencing. Depending on the project scale and local requirements, we can also coordinate onsite technical supervision to ensure the MR-UF-100TH is integrated correctly into your existing infrastructure. Our goal is to ensure your local operators are fully trained in daily maintenance and emergency troubleshooting. Because long-distance logistics can be complex, we maintain a robust supply chain for replacement membranes and spare parts to minimize potential downtime. Contact our export department to discuss the specific logistics and service requirements for your region.
Best Selling Products
Related Blogs
Related Search
Tel: +86-1353-0341575
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.