

Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.
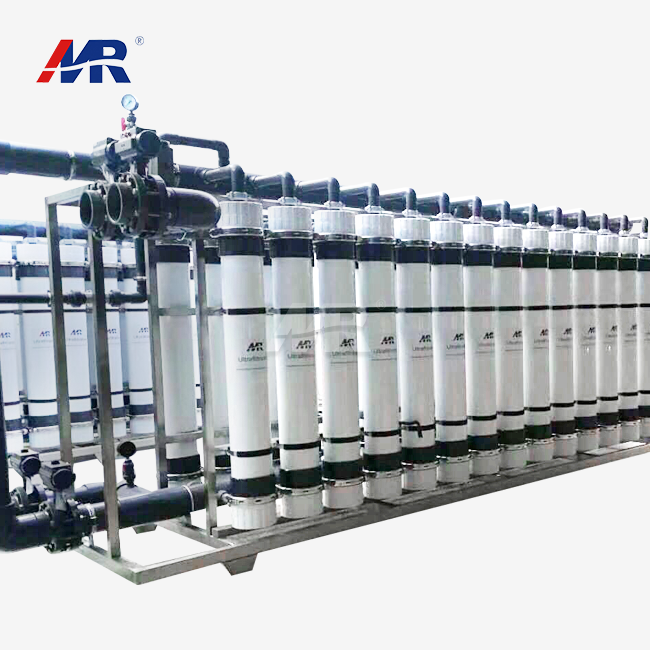
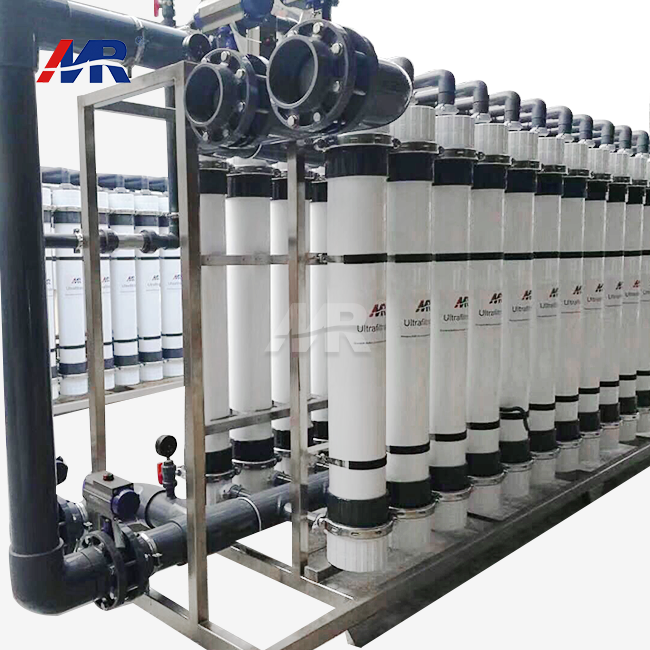
15T/H ultrafiltration system supplier
High-Capacity 15T/H Ultrafiltration System for Industrial Water Treatment
For procurement managers overseeing water treatment projects in South America, Southeast Asia, Europe, the Middle East, and Africa, identifying a reliable 15T/H ultrafiltration system is a critical step in ensuring long-term operational stability. This technology serves as a high-efficiency pressure-driven process, utilizing semi-permeable membranes with pore sizes between 0.001 and 0.1 micrometers to physically remove suspended solids, bacteria, and high-molecular-weight organic compounds. In industrial environments, the 15T/H ultrafiltration system acts as a sophisticated barrier, bridging the gap between conventional sand filtration and advanced nanofiltration to protect downstream equipment.
In many regions, particularly when dealing with borehole water treatment, operators face significant technical hurdles. Fluctuating turbidity levels and high microbial loads can lead to rapid membrane fouling, resulting in frequent downtime and high replacement costs. Furthermore, high energy prices in parts of Africa and Southeast Asia make power-intensive systems financially unsustainable. Many facilities also struggle with meeting international regulatory standards, such as CE and ROHS, which are mandatory for legal compliance in European and South American markets. Finding a 15T/H ultrafiltration system manufacturer that balances these regulatory requirements with low operational energy consumption is a primary concern for decision-makers.
Guangdong Morui Environmental Technology Co.,Ltd, established in 2005, addresses these specific pain points through the MR-UF-15TH model. This 15T/H ultrafiltration system is specifically engineered for borehole water treatment, providing a stable supply of purified water while maintaining strict adherence to ISO, CE, and ROHS certifications. As a veteran provider of 15T/H ultrafiltration system solutions, the company utilizes the MR-UF-0860 membrane configuration to ensure high flux rates even under variable feed water conditions. These systems are designed to operate at a low transmembrane pressure of 0.1-0.3Mpa, which minimizes mechanical stress on the fibers and extends the overall lifecycle of the equipment.
Key technical and operational advantages of this system include:
- Low Energy Footprint: The MR-UF-15TH is optimized for efficiency, with a power consumption of only 4kw/hour, significantly lowering the total cost of ownership for large-scale water treatment facilities.
- Advanced Membrane Performance: Utilizing the MR-UF-0860 hollow fiber membrane, the system provides high packing density and superior resistance to oxidative cleaning agents, ensuring consistent particle rejection.
- Borehole-Specific Engineering: The 15T/H ultrafiltration system is tailored to handle the unique silt and organic profiles found in deep-well water sources common in the Middle East and Africa.
- Global Compliance Standards: Full adherence to CE and ROHS documentation requirements simplifies the procurement and installation process for international infrastructure projects.
Verifying the technical specifications and energy metrics of a 15T/H ultrafiltration system is essential for aligning the technology with specific site requirements. Detailed performance logs and selection tables allow engineers to calculate the precise molecular weight cut-off needed for their local water chemistry. Technical consultations provide the data necessary to integrate these units into existing multi-stage filtration trains without compromising system pressure.
The integrated modular design ensures consistent permeate quality across diverse industrial environments.
Related Products
Guangdong Morui: Industrial Ultrafiltration Solutions You Can Rely On
Guangdong Morui Environmental Technology Co., Ltd. got its start in 2005. We build advanced water treatment equipment. Nearly 20 years in the business have taken us across South America, Southeast Asia, Europe, the Middle East, and Africa. That global reach is why, as a 15T/H ultrafiltration system supplier, we can be a steady partner on high-capacity 15T/H ultrafiltration projects.
Take the MR-UF-15TH. It's designed for borehole water treatment. The system runs at 15T/H and uses our own MR-UF-0860 hollow fiber membranes, a combination we've refined as a 15T/H ultrafiltration system supplier for years. It pulls out pathogens and suspended solids at low pressure, just 0.1-0.3Mpa. Power use holds at 4kw/hour. That kind of control suits local brand factories and tough industrial RO pretreatment jobs.
Quality comes first for us. Our factory follows ISO, CE, and ROHS standards to the letter. We run hard tests on membrane flux and chemical resistance. That gives us superior separation efficiency and long system life. For overseas clients, Morui offers full technical support, from remote commissioning to local maintenance guidance. So your operations run smoothly, no matter where you are.
Guangdong Morui is committed to running water treatment operations to a high standard. Work with us, and you get a high-performance filtration solution that brings lasting value and reliability.
Advanced 15T/H Ultrafiltration Solutions for Global Borehole Water
Application Scenarios and Industrial Context
In the global water treatment sector, the 15T/H ultrafiltration system serves as a critical bridge between raw water sourcing and high-purity output. This specific capacity is ideal for medium-scale industrial and municipal projects where groundwater consistency is paramount. Typical applications include providing high-quality process water for food and beverage production, serving as a robust pre-treatment stage for desalination plants to protect sensitive Reverse Osmosis (RO) membranes, and supplying potable water for remote communities or industrial parks relying on borehole sources. These scenarios require a system capable of handling fluctuating turbidity and microbial loads common in subsurface water.
Regional Challenges and Operational Pain Points
Operators in South America, Southeast Asia, and Africa frequently encounter borehole water contaminated with suspended solids, bacteria, and seasonal silt. In regions like the Middle East, the high mineral content often complicates filtration efficiency. Key challenges include:
- Regulatory Compliance: Meeting stringent ISO and CE standards is non-negotiable for projects in Europe and international industrial zones; failure to comply leads to legal risks and operational shutdowns.
- Energy Efficiency: With rising electricity costs in developing markets, high power consumption significantly impacts the total cost of ownership.
- Maintenance Hurdles: In remote locations, frequent downtime due to membrane fouling or complex manual cleaning routines can paralyze local production lines.
Integrated Solutions by Guangdong Morui
Guangdong Morui Environmental Technology Co.,Ltd, established in 2005, leverages nearly two decades of expertise to provide a "plug-and-play" modular solution centered on the MR-UF-15TH model. Our approach focuses on stabilizing output quality while minimizing the technical burden on local staff. By integrating advanced membrane technology with automated safeguards, the system effectively addresses the volatility of borehole water, ensuring a physical barrier against pathogens and colloids regardless of the feed water's initial state.
System Architecture and Technical Integration
The 15T/H ultrafiltration system is structured into four primary modules designed for maximum resilience:
- Automated Pre-filtration Unit: Utilizes multi-media filters to remove larger particulates, significantly reducing the solids loading on the primary ultrafiltration membranes.
- High-Performance UF Core: Featuring the MR-UF-0860 hollow fiber membrane, the system operates at a stable pressure of 0.1-0.3Mpa, utilizing size exclusion to filter out particles down to 0.01 microns.
- Energy-Optimized Power Hub: The system is engineered to consume only 4kw/hour, making it one of the most energy-efficient solutions in its class for borehole treatment.
- Smart Control & CIP Module: An integrated PLC manages the backwash cycles and Chemically Enhanced Backwash (CEB) processes, maintaining membrane flux without intensive manual intervention.
Quantifiable Benefits and Value
- Enhanced Microbiological Safety: Provides a validated physical barrier, achieving up to 4-log reduction in viruses and bacteria.
- Reduced Operational Cost: The 4kw/hour power profile lowers monthly energy expenditures by approximately 15-20% compared to traditional pressurized systems.
- Extended Equipment Life: Consistent 0.1-0.3Mpa operating pressure reduces mechanical stress on pipes and fittings, extending the system's lifespan to over 10 years.
- Certified Reliability: Fully compliant with CE and ROHS directives, ensuring smooth customs clearance and environmental auditing in any target market.
Technical Implementation and Global Support
The implementation process begins with a comprehensive water chemistry analysis to calibrate the MR-UF-0860 membranes to specific borehole conditions. From the 2005-established manufacturing base, systems are pre-commissioned and skid-mounted for rapid deployment. Support for markets in South America and Southeast Asia includes remote diagnostic capabilities and a standardized spare parts kit, ensuring that critical components like replacement membranes or sensors are available within minimal lead times to prevent unplanned downtime.
Typical Implementation Case
In a recent borehole water project in Southeast Asia, a manufacturing facility faced high turbidity and bacterial counts that compromised their cooling towers. By implementing the MR-UF-15TH solution, the site achieved a constant 15T/H flow with turbidity levels consistently below 0.1 NTU. The automated backwash system reduced manual cleaning frequency from daily to once every two weeks, while the 4kw/h energy consumption aligned with the facility's sustainability goals.
The MR-UF-15TH ultrafiltration system ensures high-efficiency removal of suspended solids and pathogens from borehole water sources through precision-engineered hollow fiber membrane technology.
FAQs
1. What is a 15T/H ultrafiltration system and why is it preferred for borehole water treatment?
A 15T/H ultrafiltration system is a high-efficiency water purification unit capable of processing 15,000 liters of water per hour. Unlike traditional sand filtration, this system utilizes semi-permeable membranes with a pore size range of 0.001 to 0.1 micrometers to physically block bacteria, viruses, and suspended solids while retaining essential minerals. For borehole water treatment, the system acts as a reliable barrier against microorganisms and colloidal particles. The Guangdong Morui MR-UF-15TH model is specifically designed for these industrial applications, utilizing a low-energy 4kw/hour power consumption and operating at a stable pressure of 0.1-0.3Mpa. By choosing this technology, industrial users can achieve a consistent water flux that meets high-quality standards, making it an ideal pretreatment step for reverse osmosis systems to prevent downstream membrane fouling.2. How do I select the right membrane and configuration for an industrial 15T/H ultrafiltration system?
Selecting the right configuration depends largely on your raw water quality and the required Molecular Weight Cut-Off (MWCO). For a 15T/H ultrafiltration system, we typically recommend high-performance polymers like PVDF or PES, such as our MR-UF-0860 membrane, which offers superior chemical resistance and mechanical strength. When evaluating a system, you should focus on the packing density of the hollow fibers and the ability of the system to operate under low transmembrane pressure (0.1-0.3Mpa) to save energy. It is also vital to consider the flux rate, measured in LMH (liters per square meter per hour), to ensure the system handles your specific capacity requirements without over-stressing the fibers. Guangdong Morui Environmental Technology Co.,Ltd, established in 2005, provides expert consultations to help you match these technical parameters to your project’s specific borehole water analysis.3. What international certifications are required for exporting a 15T/H ultrafiltration system to Europe or South America?
When importing water treatment equipment into markets like Europe or South America, compliance with international safety and quality standards is essential. A 15T/H ultrafiltration system should generally meet ISO 9001 quality management standards and carry the CE mark for European safety compliance. Additionally, ROHS certification ensures that the components are free from hazardous substances. Our MR-UF-15TH system is manufactured under these rigorous protocols to facilitate smooth customs clearance and ensure operational safety. While these certifications cover global requirements, specific countries may have additional local regulations regarding pressurized vessels or drinking water contact materials. We recommend consulting with Guangdong Morui to ensure all necessary technical documentation and certificates are prepared for your project's location to avoid regulatory delays during the import process.4. How does the MR-UF-15TH system manage membrane fouling and maintenance in Southeast Asia or Middle East climates?
In tropical regions like Southeast Asia or arid climates in the Middle East, high temperatures and mineral-rich borehole water can accelerate membrane fouling. Our 15T/H ultrafiltration system addresses this through an optimized hollow fiber design that facilitates efficient backwashing and chemical cleaning. By maintaining an operating pressure of 0.1-0.3Mpa, the system minimizes the compaction of contaminants on the membrane surface. Regular maintenance involves periodic flushing and occasional chemical cleaning with agents like sodium hypochlorite to remove organic buildup. We suggest replacing the MR-UF-0860 filters every 6 to 12 months, depending on the turbidity of the source water. Guangdong Morui provides specific maintenance protocols tailored to high-temperature environments to ensure your system continues to operate at its peak 15T/H capacity while maintaining a low power draw of 4kw/hour.5. What technical support and lead times can I expect from Guangdong Morui for projects in Africa or Southeast Asia?
Guangdong Morui Environmental Technology Co.,Ltd has been a professional manufacturer since 2005, developing a robust logistics and support network for Southeast Asia and Africa. For a standard 15T/H ultrafiltration system, the typical production lead time is approximately 4 to 6 weeks, ensuring that every unit undergoes strict quality testing before dispatch. We provide comprehensive technical support for international clients, including detailed installation manuals, video tutorials, and remote commissioning assistance to ensure the MR-UF-15TH model is integrated correctly into your borehole water treatment plant. For large-scale industrial projects, we can also discuss tailored technical solutions based on your specific feed water parameters. If you are located in these regions, please contact our engineering team to receive a precise shipping schedule and a customized technical proposal for your water treatment needs.
Best Selling Products
Related Blogs
Related Search
Email:benson@guangdongmorui.com
Whatapp:8613530341575
Add: No.3 Xuwu Road, Baoan District, Shenzhen, China.